


Choosing the right Die Spotting Machine in 2026 requires more than comparing purchase prices. A reliable machine must match your mold dimensions, maintenance skills, production rhythm, and workshop space. This guide explains the practical details buyers often miss, including clamping force, platen size, daylight opening, mold height, tilting range, and spotting accuracy. A few millimeters can affect mold fitting, especially when large automotive tools need careful adjustment.
Look closely at the machine’s hydraulic or servo system, control interface, safety guarding, and access around the mold. Ask for measurable repeatability data, not only attractive catalog language. Energy consumption also matters. A servo-driven model may reduce operating costs, but its higher initial price needs realistic production data. Request installation requirements, training support, spare-parts availability, and response times from the supplier. These details often decide whether the machine remains productive after several years.
This guide uses manufacturer specifications, operating considerations, and common mold-shop evaluation practices. Independent references and a factory demonstration can strengthen your decision. Watch a complete cycle, listen for unusual pump noise, and inspect movement during low-speed mold closing. No machine is perfect. A cheaper option may perform well in one workshop and struggle in another. I would still question any promise of “universal” compatibility. Mold weight, operator experience, maintenance quality, and local service can change the result. Use this guide as a careful starting point, then confirm every critical specification before signing an order.
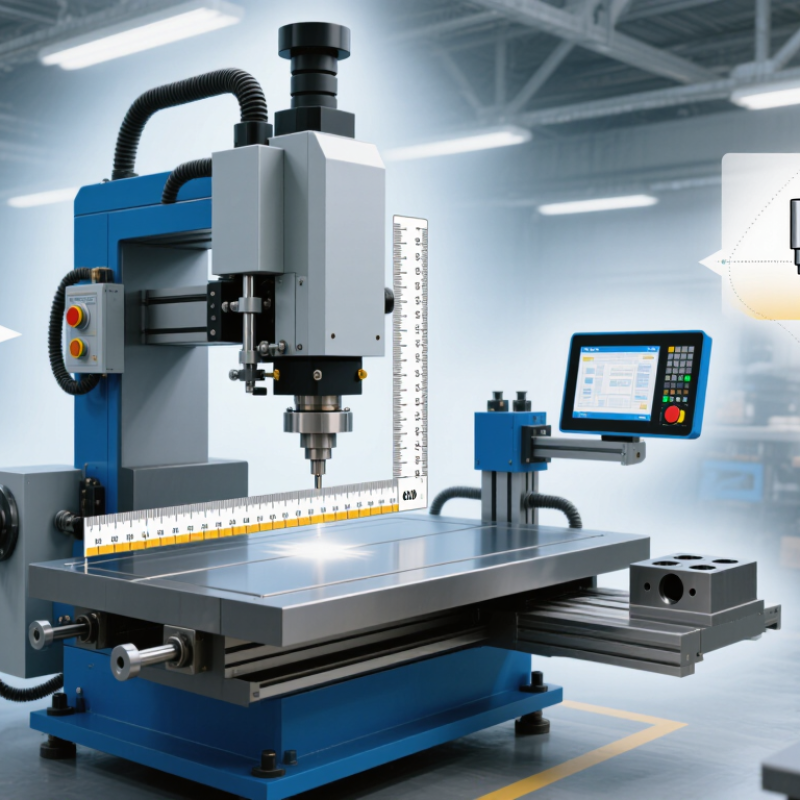
A die spotting machine is a specialized press for checking and correcting molds before production. It opens, closes, and lightly clamps the die at controlled speed and pressure. Technicians inspect parting lines, slides, inserts, and ejector movement on a clear working area. Unlike a production press, it focuses on fitting accuracy rather than injection speed. Hydraulic systems remain common, while servo-driven designs can offer finer movement control and lower idle energy use.
The need for reliable mold maintenance is significant. PlasticsEurope reported global plastics production of about 414 million tonnes in 2023. Every mold error can create scrap, delays, or repeated bench work. A spotting machine helps reveal uneven contact through low-pressure closing and marking compounds. It can also reduce manual lifting when the platen, safety system, and load capacity match the tool. Still, catalog specifications can mislead. Maximum clamping force does not prove better spotting accuracy. I would verify repeatability, platen parallelism, stroke control, and service support with actual test records.
Tips: Measure your largest die first. Check its weight, height, and center of gravity. Request a demonstration with a comparable mold. Watch the closing motion closely. Ask how accuracy is calibrated and documented. Leave room for future tooling changes; a machine that barely fits today may become restrictive tomorrow. Also, operator training matters more than many buyers expect. A perfect machine can still produce poor decisions.
In 2026, the most important die spotting machine specification is not maximum tonnage. It is controlled accuracy under real shop conditions. When checking a machine, measure platen parallelism, table flatness, spotting pressure, daylight, stroke, and die weight capacity. Ask for test records, not brochure claims. A useful target is repeatable, low-pressure contact without marking the parting line. Operators should verify T-slot layout, lifting access, guarding, and control response with an actual die. Small details matter.
The 2024 World Robotics report recorded 541,302 industrial robot installations in 2023, highlighting automation’s growing reach. This makes interface specifications practical, not decorative. Check I/O availability, recipe storage, remote diagnostics, and communication protocols before purchase. Repeatability matters more than headline speed. Published cycle time can hide manual loading, setup, and inspection. Request a complete timed demonstration.
The U.S. Department of Energy’s compressed-air system guidance notes that air systems can consume 10–30% of industrial electricity. Ask for standby consumption, pump efficiency, and heat rejection requirements.
Safety is a specification. ISO 12100 risk-assessment principles should shape guarding, access doors, emergency stops, and control layouts. I would not buy from accuracy alone. Service access, calibration intervals, spare-part availability, and operator training often decide whether precision survives after installation. A modest machine with transparent test data may outperform a larger machine with vague tolerances. That is the uncomfortable part.
Buying a die spotting machine in 2026 requires more than comparing tonnage. The machine type should match mold work, maintenance habits, and available floor space.
Hydraulic models provide strong, controlled clamping for complex molds. Servo-electric versions can offer cleaner operation, precise positioning, and lower idle energy use. Hybrid designs may balance force and responsiveness, but their controls can require better operator training.
Keep it practical. Size must be measured from the mold, not guessed from product descriptions. Check bolster length, width, T-slots, daylight, stroke, and maximum mold weight. A mold may fit the table yet fail when the upper half needs extra opening clearance.
Confirm tilting angle, ejector access, and crane loading space before ordering. Allow room for guards and maintenance doors.
A larger frame is not automatically better. It can increase installation, energy, and maintenance costs.
During demonstrations, test slow jog movement, pressure holding, speed adjustment, and position repeatability. Inspect the HMI for clear alarms, stored recipes, and permission levels.
Safety interlocks, two-hand controls, light curtains, and emergency stops deserve hands-on verification. Ask for measured cycle data, not optimistic estimates.
Review leakage control, lubrication points, noise, and service access. I would request references from plants using similar mold weights.
One overlooked detail matters: operator visibility. If the platen hides the cavity, setup errors become expensive.
My comparison sheets often miss ergonomics at first. That mistake is worth correcting before approval.
Safety should be checked on the shop floor, not only in a brochure. The U.S. Bureau of Labor Statistics recorded 2.6 million nonfatal workplace injuries and illnesses in private industry during 2023. That figure makes guarding, visibility, and emergency access practical buying concerns. Confirm interlocked doors, two-hand controls, safe hydraulic pressure release, and clearly reachable emergency stops. The design should also align with OSHA 29 CFR 1910.212 and ISO 12100 risk-assessment principles. Ask for safety-circuit documentation, not promises.
Maintenance details often decide the machine’s real cost. Request a service schedule covering lubrication, hydraulic filters, sensors, guide surfaces, and electrical inspections. A clean access panel matters when technicians work beside a large mold. Check whether diagnostic codes identify the failed component. Replacement parts should have stated lead times and technical specifications. The U.S. Department of Energy’s Operations and Maintenance Best Practices Guide links planned maintenance with improved equipment reliability, although shop conditions can change the result. Maintenance claims need evidence.
Support is more than a telephone number. Ask about operator training, remote troubleshooting, installation supervision, and response times. Confirm whether software updates preserve safety functions and production records. The NIST Cybersecurity Framework is useful when machines connect to factory networks. A low purchase price can look clever. It may not. One uncomfortable question remains: can your team maintain the machine without depending on one specialist? If the answer is no, the buying decision is not finished.
How to Choose the Best Die Spotting Machine for Your Application?
Choosing a die spotting machine starts with the tool, not the machine’s advertised tonnage. Measure die weight, shut height, opening stroke, platen dimensions, and required spotting pressure. A machine may fit the mould but still lack useful access for inserts or cooling lines. The 2024 World Machine Tool Survey reported global machine-tool consumption above US$80 billion in 2023. This reflects strong investment, but it does not guarantee suitability for every die shop. Application details still decide performance.
Check repeatability under real loading conditions. Ask for positioning accuracy, pressure stability, cycle data, and maintenance records. ISO 230-1 provides a recognized framework for evaluating machine-tool accuracy and testing conditions. Use it when comparing supplier claims. For casting applications, NADCA’s Product Specification Standards also highlight the importance of dimensional control and process consistency. A practical trial is valuable. Test your heaviest die, not an easy sample. I have seen specifications look excellent on paper, yet access became awkward during manual adjustment.
Tips: Select the smallest machine that safely handles your largest die. Confirm platen rigidity and operator visibility. Request energy data from actual cycles, not idle operation. Review local service response times and spare-part availability. Leave room for future tooling changes. That choice is often underestimated. MarketsandMarkets’ 2024 die-casting industry analysis identified continued automation and efficiency improvements as major market drivers. Still, automation can add complexity. If technicians cannot adjust the system confidently, the “best” machine may become an expensive compromise.
Use the following engineering-based comparison table to match machine capability with die size, tooling weight, adjustment needs, production environment, and operator-safety requirements.
| Selection Dimension | Typical Reference Range or Option | Best Fit / Application | Why It Matters | What to Verify Before Purchase |
|---|---|---|---|---|
| Machine Type | Hydraulic die spotting machine; servo-hydraulic machine; mechanical or toggle-assisted design | Hydraulic or servo-hydraulic systems are generally suitable for mold assembly, trial fitting, repair, and low-speed die validation. | Different drive systems affect control, positioning, energy use, maintenance, and the ability to handle variable loads. | Confirm whether the machine supports controlled opening, closing, tilting, low-speed movement, pressure holding, and safe mold access. |
| Required Clamping Force | Common machine classes range from approximately 500 kN to more than 10,000 kN; select according to die mass, projected load, and safety margin. | Smaller machines for precision molds and compact dies; higher-force machines for large automotive, casting, or multi-cavity tooling. | Insufficient force can cause unstable mold handling, while excessive capacity can increase purchase price, floor loading, and energy consumption. | Calculate the maximum mold weight and required closing force from actual tooling data. Do not select only by nominal force. |
| Maximum Mold Dimensions | Typical working areas may range from about 400 × 400 mm to over 2,000 × 1,500 mm, depending on machine class. | Choose a working area larger than the maximum die footprint while preserving access for clamps, ejectors, sensors, and maintenance. | The mold must sit fully on the spotting table without overhang that could affect stability or access. | Check maximum mold length, width, height, mounting pattern, T-slots, clamping points, and allowable overhang. |
| Maximum Mold Weight | Typical rated capacities range from approximately 1,000 kg to more than 20,000 kg. | Select a capacity comfortably above the heaviest complete die, including inserts, adapters, lifting fixtures, and temporary tooling. | Rated capacity is normally based on structural and hydraulic limits; uneven loading may reduce the practical safe capacity. | Ask for the permitted load distribution, center-of-gravity limits, table deflection data, and lifting or loading procedure. |
| Opening Stroke | Common opening strokes are approximately 500–1,500 mm; larger machines may provide more. | Use a longer stroke for deep molds, tall inserts, core-pull mechanisms, and applications requiring clear access to parting surfaces. | Insufficient stroke can prevent full inspection or make insert installation difficult. | Measure the required daylight between mold halves, including ejector travel, lifting tools, and operator access clearance. |
| Daylight Between Platens | Typical maximum daylight may range from approximately 800 mm to 2,500 mm, depending on machine design. | Important for tall dies, stacked components, large inserts, and manual or robotic mold servicing. | Daylight determines whether the assembled mold can be loaded, opened, inspected, and removed safely. | Verify minimum and maximum mold height, open-position clearance, and whether daylight changes when the table is tilted. |
| Table Tilting Capability | Common options include no tilt, one-axis tilt, or two-axis tilt; typical tilt angles are approximately 90° in one axis or up to 180° in rotating designs. | Tilting is valuable for die inspection, polishing, insert replacement, spotting blue checks, and maintenance access. | Tilting can reduce manual handling and improve visibility of parting lines and difficult-to-reach areas. | Check tilt angle, rotation speed, locking method, allowable tilted load, center-of-gravity limits, and pinch-point protection. |
| Positioning Accuracy | Typical controlled positioning accuracy may be specified from approximately ±0.05 mm to ±0.20 mm, depending on machine size and measurement method. | Use higher accuracy for precision injection molds, die-casting dies, progressive dies, and tooling with tight parting-line requirements. | Accurate positioning supports repeatable spotting and reduces rework during mold fitting. | Request measured repeatability, not only nominal resolution. Confirm test conditions, measurement points, and calibration method. |
| Operating Speed | Fast approach speeds may be several hundred millimeters per second, while spotting and final closing should use controlled low speed. | High approach speed improves productivity; precise low-speed movement is essential near parting surfaces and inserts. | A machine needs both productivity and fine control; maximum speed alone is not a useful quality indicator. | Compare approach speed, spotting speed, crawl speed, acceleration control, stopping distance, and speed under load. |
| Pressure and Force Control | Adjustable hydraulic pressure, proportional valves, force monitoring, and programmable pressure stages are common options. | Useful for controlled contact, protecting delicate inserts, checking flash areas, and repeatable die fitting. | Controlled force prevents unnecessary damage when the die halves or inserts are not fully aligned. | Verify force-control resolution, pressure stability, alarm limits, data logging, and automatic overload protection. |
| Control System | Basic manual controls; touchscreen PLC control; programmable recipes with position, speed, pressure, and sequence monitoring. | Manual control suits occasional repair work; programmable control is better for repeated tooling trials and standardized processes. | Recipe storage improves repeatability between operators and reduces setup errors. | Check user permissions, recipe backup, multilingual support, diagnostic functions, HMI visibility, and control-system service life. |
| Table and Platen Design | Hardened or machined steel surfaces; T-slots, threaded holes, clamping rails, replaceable wear plates, and optional adapter plates. | Choose the interface that matches existing mold bases, clamps, lifting devices, and workshop fixtures. | A suitable table interface reduces setup time and prevents unsafe improvised clamping. | Confirm table flatness, allowable surface pressure, slot dimensions, hole pattern, replaceability, and corrosion protection. |
| Loading and Handling | Overhead-crane loading; integrated loading table; powered roller or sliding system; robotic or semi-automatic handling. | Integrated handling is useful for heavy dies or frequent changeovers; crane loading may be sufficient for low utilization. | Handling arrangements affect installation time, labor requirements, and the risk of impact damage. | Confirm loading height, transfer path, crane capacity, floor clearance, lifting points, and compatibility with existing equipment. |
| Safety Features | Guarding, interlocked doors, emergency stops, two-hand controls, light curtains, anti-drop protection, overload monitoring, and safety-rated control circuits. | All applications require a documented risk assessment and safeguards appropriate to movement, crushing, tilting, and stored hydraulic energy. | Die spotting involves heavy moving components and pinch points; safety must not depend only on operator awareness. | Verify conformity with applicable local machinery-safety legislation, safety validation documents, lockout provisions, and operator training requirements. |
| Energy Consumption | Variable-displacement or servo-hydraulic pumps generally reduce idle energy compared with fixed-speed systems, but actual consumption depends on cycle and load. | Energy-efficient systems are beneficial for frequent operation, long idle periods, or facilities with energy-management targets. | Hydraulic power demand varies significantly between approach, spotting, holding, and tilting operations. | Request measured power data for a representative cycle rather than relying only on installed motor power. |
| Maintenance Requirements | Hydraulic oil and filter service; lubrication; seal and hose inspection; alignment checks; electrical and safety-system testing. | Choose accessible service points and commonly available components when uptime is critical. | Maintenance access and spare-parts availability directly affect total cost of ownership. | Review maintenance intervals, oil specifications, filtration grade, recommended spare parts, service response, and documentation. |
| Installation Conditions | Requirements may include reinforced foundations, level flooring, electrical supply, hydraulic-fluid handling, ventilation, and overhead clearance. | Large machines may require a foundation design and lifting plan before delivery. | Insufficient foundation strength or floor flatness can affect alignment, vibration, and long-term accuracy. | Obtain total machine weight, floor-loading data, anchor layout, power requirements, transport dimensions, and commissioning requirements. |
| Application Match | Injection molds; die-casting dies; stamping dies; progressive dies; compression molds; maintenance and repair tooling. | Select based on the dominant tooling type and the most demanding mold dimensions, weight, access, and accuracy requirements. | A machine optimized for small precision molds may not be suitable for large automotive dies or high-load casting tooling. | Run a sample-die trial using representative tooling and document loading, opening, tilting, spotting, and removal steps. |
| Total Cost of Ownership | Purchase price plus installation, foundation work, tooling adapters, energy, maintenance, calibration, training, and downtime. | Compare lifecycle cost over the expected service period rather than comparing the initial price alone. | The lowest initial price may result in higher operating cost, longer setup time, or limited future capacity. | Request a complete quotation including options, commissioning, warranty, training, spare parts, software, and service terms. |
Important: The ranges above are general engineering reference values, not a specification for one particular machine. Final selection should be confirmed with the actual die drawings, maximum die weight, center of gravity, required opening clearance, force profile, safety assessment, available floor space, and local electrical and machinery-safety requirements.



For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.