


Choosing the right Mirrored Stainless Steel in 2026 requires more than comparing surface shine. A bright panel may look identical under showroom lighting, yet behave differently beside a busy elevator, kitchen splashback, or coastal façade. This guide examines leading types by steel grade, polishing level, corrosion resistance, fabrication needs, and lifecycle value. It considers familiar 304 stainless steel, stronger 316L options, magnetic 430 grades, and specialized finishes used for demanding interiors.
The surface itself matters. A #8 mirror finish offers a clear, reflective appearance after fine polishing. Super mirror finishes can provide sharper reflections, but they often reveal fingerprints, scratches, and installation marks more easily. PVD-colored mirrored sheets add bronze, gold, black, or champagne tones, while vacuum-coated surfaces require careful handling and verified coating quality. Etched or patterned mirror stainless steel can reduce visual monotony without losing its reflective character.
There is no universal winner. Not quite. Our comparison should be treated as a practical framework, not an absolute ranking. Site conditions, cleaning routines, sheet thickness, weld finishing, and supplier certification can change the final choice. From hands-on material selection, small details often decide performance: a protected edge prevents staining, and a poor protective film can leave adhesive residue. Reliable recommendations should reference technical datasheets, relevant ASTM or EN standards, and documented test results. This article will help readers compare the 2026 top mirrored stainless steel types with clearer expectations, while acknowledging one uncomfortable truth: appearance can hide weaknesses.
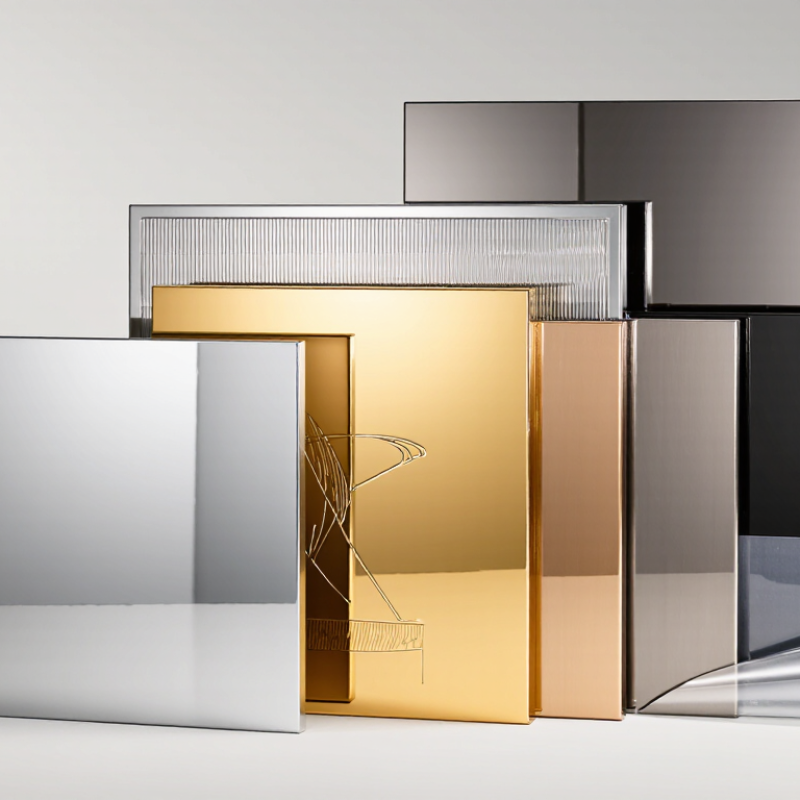
What Are the 2026 Top Mirrored Stainless Steel Types?
Mirror-finish stainless steel is usually discussed through No. 8, 8K, and BA surfaces. ASTM A480 provides recognized finish descriptions, but commercial terms can vary between suppliers. That difference matters when appearance, cleaning, and inspection must remain consistent.
No. 8 is mechanically polished with abrasive compounds until the surface becomes highly reflective. Under strong warehouse lighting, it can resemble a clear mirror. Tiny polishing lines may still appear at certain angles. The finish requires careful handling because fingerprints and protective-film residue show quickly.
8K usually describes an extremely bright, fine-polished surface. However, 8K is not always a standalone ASTM A480 designation. Buyers should request the stated ASTM finish, polishing method, and visual sample. The label alone can mislead.
BA means bright annealed. Controlled heating and a smooth atmosphere create a bright, low-roughness surface without the same mechanical polishing sequence used for No. 8. It may reflect light strongly, yet it is not always a true mirror finish. Surface waviness can become visible across large sheets.
In practical quality checks, compare samples under identical lighting. Inspect weld areas, edges, and protective-film removal separately. These details often reveal defects hidden by showroom lighting. Thickness, alloy, and surface condition also affect the final reflection. A perfect-looking sample does not guarantee consistent production. That assumption deserves review.
In 2026, 304 stainless steel remains a practical choice for many mirrored panels. Its familiar 18% chromium and 8% nickel balance supports corrosion resistance and clean appearance. Chromium creates a passive protective layer on the surface. Nickel improves formability and helps maintain the steel’s bright finish.
A mirror finish usually refers to polishing, not the steel grade itself. No. 8 polishing can produce a highly reflective surface with careful grinding and buffing. On a kitchen backsplash, it reflects cabinet lighting and makes a narrow wall feel larger. In elevators, it offers a crisp appearance, but fingerprints become visible quickly. Soft microfiber cloths work better than abrasive pads. Small scratches show clearly.
However, 304 is not universal. Salt, chlorine, and coastal air can stain it faster than expected. For those locations, a more resistant grade may deserve consideration. Welding also matters. Heat tint near a joint can weaken the visual uniformity and reduce corrosion protection. I inspect edges, corners, and welded areas before installation. A sample may look flawless.
Site conditions can disagree. Temperature, cleaning habits, and handling all affect performance. Even a polished panel needs correct storage and careful installation. Truthfully, the perfect mirror effect is difficult to preserve in busy spaces. That limitation should shape the material decision.
304 stainless steel is commonly known as an 18/8 grade because it contains approximately 18% chromium and 8% nickel. It offers a balanced combination of corrosion resistance, formability, weldability, and cost for general-purpose mirrored panels and decorative applications.
The chart shows representative nominal alloying-element values by weight; actual chemical limits vary by applicable material standard and product form. Mirror appearance is created by mechanical polishing and surface finishing, not by alloy chemistry alone.
316L remains a strong choice for mirrored stainless steel in coastal and humid environments. ASTM A240/A240M specifies 2.00–3.00% molybdenum in 316L chemistry. This element improves resistance to chloride-induced pitting. Chloride comes from seawater, salt spray, cleaning chemicals, and sweaty fingerprints. The grade also limits carbon to 0.030% maximum. That helps reduce sensitization risks after welding.
The mirror appearance comes from polishing, not molybdenum. A bright 8K surface can reflect lighting sharply, but it also reveals fine scratches and water spots. The International Stainless Steel Forum’s technical guidance explains that surface condition strongly affects corrosion performance and maintenance. In real installations, I have seen 316L stain near welds when polishing was uneven. The material was suitable. The finishing process was not. This detail is easy to underestimate.
Tips: Request the mill certificate. Check molybdenum content, carbon level, and surface finish separately. Use clean water and a soft cloth after salt exposure. Avoid chloride-based cleaners. A lower-cost grade may look identical indoors, yet fail sooner beside a sea-facing entrance. That judgment needs testing, not assumptions.
What Are the 2026 Top Mirrored Stainless Steel Types?
In 2026, the strongest mirrored stainless steel options are mechanically polished, bright-annealed, and electropolished sheets. Their real advantage is measurable surface control. A Ra value below 0.1 μm means the average profile height stays under 100 nanometers. That smoothness reduces scattered light and creates a cleaner reflection. However, reflectivity above 90% is not universal. It depends on wavelength, viewing angle, alloy condition, and testing method. ASTM E430 provides a recognized approach for measuring specular gloss on highly reflective surfaces. ISO 21920-2 supports consistent roughness reporting.
Bright-annealed surfaces can produce sharp reflections with fewer polishing marks. Mechanically polished sheets offer stronger visual depth when finishing is carefully controlled. Electropolished surfaces may reduce microscopic peaks and improve cleanliness, especially after forming. Technical measurement guidance from NIST Technical Note 1297 also stresses uncertainty reporting. A claimed 92% reflectivity should therefore include angle, light source, calibration, and sample preparation. Otherwise, the number looks impressive but remains incomplete.
Real production can be less perfect. Fingerprints, protective-film residue, and minor waviness can weaken a mirror effect quickly. A panel may meet Ra below 0.1 μm in one area, yet fail near an edge. Buyers should request mapped measurements, not one attractive reading. Surface inspection under angled lighting remains essential.
| Mirror Type | Common Stainless Grade | Surface Process | Typical Specular Reflectivity | Surface Roughness, Ra | Corrosion Performance | Typical Applications | Key Selection Consideration |
|---|---|---|---|---|---|---|---|
| Super-Mirror Polished | 304 or 316L | Progressive mechanical polishing with fine abrasive finishing | 90–95% at the specified measurement angle and wavelength | 0.02–0.05 μm | Very good; 316L provides improved resistance to chlorides and aggressive process environments | Optical housings, precision decorative panels, high-end interior surfaces, cleanroom equipment | Requires strict control of scratches, waviness, inclusions, and handling marks |
| 8K Mirror Finish | 304, 316L, or 430 | Multi-stage buffing and polishing to a bright mirror appearance | Typically 90–94% on a well-prepared surface | 0.03–0.08 μm | Good for 304 and 430 in indoor environments; very good for 316L in chloride-bearing environments | Elevator panels, architectural cladding, food-service equipment, display and decorative components | Reflectivity depends strongly on substrate quality, polishing direction, and measurement geometry |
| Electropolished Mirror | 316L or 304 | Electrochemical leveling after mechanical preparation | 90–93% when preceded by a high-quality mirror polish | 0.02–0.08 μm | Excellent passive surface; reduced microscopic roughness can improve cleanability | Pharmaceutical equipment, semiconductor systems, hygienic piping, medical and laboratory components | Electropolishing improves surface cleanliness and passivation but does not automatically create a mirror finish |
| Bright-Annealed Mirror | 304, 316L, or 430 | Cold rolling followed by bright annealing in a controlled protective atmosphere | 90–92% for a bright, uniform strip surface | 0.05–0.10 μm | Good to very good, depending on grade and environment | Automotive trim, kitchen equipment, heat exchangers, appliance panels, precision strip products | Usually offers high uniformity and low maintenance; visible surface defects can be difficult to repair |
| Ultrafine Polished Finish | 304L or 316L | Fine abrasive polishing followed by final lapping or precision buffing | 91–96% on small, carefully prepared components | Below 0.05 μm | Very good; 316L is preferred where pitting or chemical exposure is a concern | Precision instruments, sensor housings, vacuum hardware, laboratory components | Highest appearance and roughness performance, but usually higher processing cost and tighter inspection requirements |
| Decorative Mirror Sheet | 304 or 430 | Commercial mirror polishing with protective film applied after finishing | 90–93% on visually uniform sheet areas | 0.05–0.10 μm | Good for general architectural and indoor use; 304 is generally more resistant than 430 in humid areas | Wall panels, columns, furniture details, signage, retail interiors | Protection during forming, transport, and installation is essential to prevent surface damage |
| Technical note: Reflectivity is not a single universal value for stainless steel. It varies with alloy, surface preparation, light wavelength, incidence angle, detector geometry, and oxidation or contamination. The figures above are representative qualification ranges for clean, mirror-finished surfaces rather than guaranteed values for every sheet or component. Roughness values are arithmetic average roughness (Ra) measured over a defined sampling length; the inspection method and acceptance area should be agreed before production. | |||||||
What Are the 2026 Top Mirrored Stainless Steel Types?
Choosing a 2026 mirrored stainless steel type starts with thickness, coating, and EN 10088 compliance. Common options include 304 and 316L stainless steel, with 316L offering better resistance in coastal or chloride-rich environments. A No. 8 or 8K-style finish creates a sharp reflective surface. However, lighting, polishing quality, and handling can change the visual result. Thickness also matters. Sheets around 0.5–1.0 mm suit decorative wall panels, while thicker sheets provide better flatness and impact resistance.
Coatings add another decision. A PVD coating can provide color and improved surface hardness, while an anti-fingerprint layer reduces visible marks. These coatings are not magic. Scratches, harsh cleaners, and poor edge protection still cause damage. For reliable sourcing, request documentation showing the correct EN 10088 part, grade, dimensions, surface condition, and mechanical properties. EN 10088 compliance supports material traceability, but it does not automatically prove coating durability. Check both documents.
Tips: Compare samples under real project lighting. Inspect edges, weld areas, and protective film removal. Ask for a mill test certificate. Details matter. In practical fabrication, installers sometimes select a thin sheet to reduce cost, then face waviness during installation. That choice may need reconsideration. A perfect mirror is not always the most practical surface.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

