10 AGV AMR Buying Tips for Global Buyers?

Global buyers need more than a robot brochure. They need evidence that an Agv Amr system can perform reliably in their facility, workforce, and operating environment. A vehicle moving pallets smoothly during a demonstration may struggle with uneven floors, reflective packaging, narrow aisles, or unexpected pedestrian traffic. Real purchasing decisions begin with these details.

Melonee Wise, a respected robotics executive and industry expert, has often emphasized a practical principle: “Robots should solve a real problem, not create a new one.” That principle should guide every evaluation. Buyers must examine payload accuracy, navigation methods, safety functions, charging behavior, fleet software, integration options, service coverage, and total ownership cost. They should also ask who will support the system after installation. A low purchase price can become expensive when spare parts, training, or remote assistance are unavailable.

Start with the workflow.

This guide presents 10 AGV AMR buying tips for global buyers. It focuses on measurable performance, supplier credibility, deployment experience, and long-term adaptability. Site surveys, live route tests, and pilot programs often reveal more than polished presentations. Ask the supplier to demonstrate recovery from a blocked aisle, a low battery, and a changed delivery point. Small failures matter.

No checklist predicts every exception. Some recommendations may require revision after local testing, especially across different factories, climates, and labor practices. That is not a weakness. It is responsible planning. The strongest Agv Amr investment is not always the fastest machine or the cheapest quote. It is the system that keeps working when real operations become messy.
10 AGV AMR Buying Tips for Global Buyers?

Define AGV and AMR Needs for Your Facility

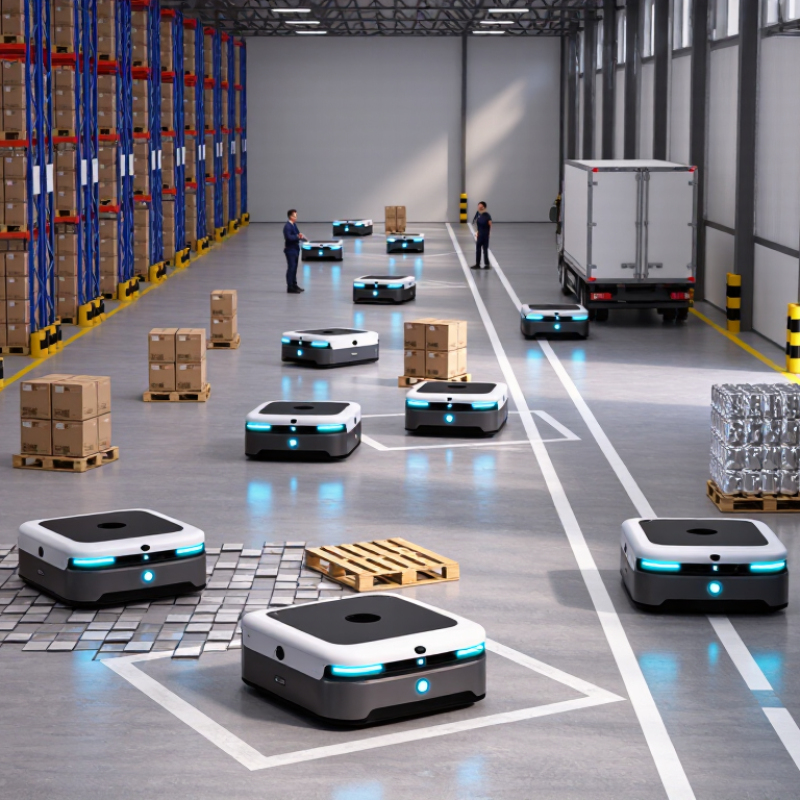
Before buying, define the work your facility truly needs. An AGV follows planned routes, markers, wires, or mapped paths. It suits repeatable transport between fixed stations. An AMR navigates changing spaces and avoids obstacles more independently. It fits facilities with variable routes, mixed traffic, or frequent layout changes. Walk the operation during a busy shift. Record load weights, pickup frequency, aisle width, floor conditions, and delivery distances. A clean spreadsheet can still miss blocked aisles and informal worker shortcuts.

Tip: Match the vehicle to the workflow, not the trend. If pallets move between two stable points, an AGV may offer simpler control. If routes change daily, an AMR may reduce manual reprogramming. Check turning space, lift height, battery cycles, charging locations, and handoff points. Safety performance also depends on pedestrian behavior, visibility, speed limits, and clearly defined zones. These details require practical observation, not only supplier specifications.

Tip: Build a small pilot around one measurable task. Track delivery time, waiting time, successful handoffs, and human interventions. Test the vehicle with real containers, uneven loads, and normal floor debris. Do not rely only on an ideal demonstration. Our facility assumptions are often incomplete, especially around peak-hour congestion. Review the results with operators, maintenance staff, and safety managers. Their experience may expose a problem that technical data does not show. A clear requirement document should state what must improve, what can change, and what still needs testing.

Compare Navigation Systems, Payloads, and Operating Environments

10 AGV AMR Buying Tips for Global Buyers
Compare Navigation Systems, Payloads, and Operating Environments

Navigation determines whether an AGV or AMR fits your facility. Laser-based systems can map changing layouts, but reflective surfaces and narrow aisles may reduce accuracy. Camera navigation needs suitable lighting and clear visual references. QR markers and magnetic guidance can offer predictable routes, although they may require more site preparation. Ask for documented accuracy, localization recovery time, and performance near people, racks, and moving equipment. Test the ugly route.

Payload figures need careful interpretation. Check both rated capacity and the load’s center of gravity. A vehicle carrying 1,000 kilograms may handle less on ramps, uneven floors, or sharp turns. Measure it empty. Then test the heaviest real load, including pallets, containers, and packaging. Review braking distance, turning clearance, lifting height, and charging frequency. A laboratory rating is not the same as reliable production performance.

Operating conditions often expose hidden weaknesses. Confirm floor flatness, aisle width, slope limits, dust protection, temperature range, humidity tolerance, and cleaning methods. Cold rooms, metal dust, sunlight, and frequent washdown can affect sensors and batteries. Evaluate pedestrian safety, emergency stops, obstacle detection, and network coverage across the entire route. Request a site trial using normal shifts and peak traffic. Leave room for failure; one missed pickup or blocked lane can reveal more than a polished demonstration. Also verify local service capability, spare-part lead times, software updates, and operator training before approving the purchase.

10 AGV and AMR Buying Tips for Global Buyers

Compare navigation systems, payload capacity, floor conditions, traffic complexity, safety requirements, charging methods, integration needs, localization support, maintenance access, and total operating cost before selecting an AGV or AMR.

Navigation system Typical operating environment Main buying consideration
Magnetic tape or wire Stable indoor routes with smooth floors Low navigation complexity, but route changes require physical modification
QR-code or landmark navigation Structured warehouses and production areas Reliable positioning when markers remain visible and undamaged
Laser reflector navigation Large facilities with defined travel lanes High repeatability, with additional reflector installation requirements
LiDAR or visual SLAM Dynamic indoor environments with changing layouts Flexible deployment, but lighting, dust, reflective surfaces, and mapping quality matter

The chart shows representative payload bands commonly found across industrial AGV and AMR product classes. Actual payload depends on vehicle design, lift height, battery configuration, floor quality, load center, safety speed, and local certification requirements.

Evaluate Safety Features, Software, and System Integration

Global buyers should treat safety, software, and integration as one purchasing decision. An impressive vehicle is not enough. Check obstacle detection, emergency stops, speed limits, warning lights, and safe recovery after a fault. Ask suppliers to demonstrate these functions with pallets, people, narrow aisles, and poor lighting. The ISO 3691-4 safety framework offers a useful reference for driverless industrial trucks, but local risk assessments still matter.

Software deserves equal scrutiny. The International Federation of Robotics reported 541,302 industrial robots were installed worldwide in 2023, showing how quickly automated equipment is entering shared workspaces. Your fleet software should support traffic control, task allocation, audit logs, cybersecurity updates, and clear operator permissions. Request live dashboards and failure histories. A polished interface can still hide weak diagnostics.

Integration is often the costly part. MHI’s 2024 Annual Industry Report found that 55% of respondents already used robotics and automation, while 76% planned to increase investment. Test connections with warehouse management, manufacturing, conveyor, elevator, and access-control systems before signing. Confirm API documentation, response times, data ownership, and support responsibilities. Run a site acceptance test during peak traffic. Do not trust a laboratory demonstration alone. It feels convincing, but it may not represent your floor. Allow time for mapping errors, changing routes, and operator hesitation. That is where many plans become less perfect.

Calculate Total Ownership Costs, Service Needs, and Scalability

A reliable AGV or AMR purchase starts with total ownership cost, not the quoted unit price. Include charging equipment, batteries, software subscriptions, integration, training, spare parts, and floor preparation. A robot may cost less initially but create higher expenses through frequent downtime. Map each cost across five to eight years. Then compare it with measurable gains, such as reduced travel time, fewer picking errors, and improved shift coverage.

Service capability matters when the warehouse is busy. Ask how quickly technicians respond, which parts are stocked locally, and whether remote diagnostics are available. Review maintenance records from similar sites, not just sales forecasts. Test navigation near loading docks, narrow aisles, changing light, and temporary obstacles. Small details matter. A weak wireless signal can delay an entire task queue.

Scalability should be proven during a controlled pilot. Begin with a limited route and measure completed missions, charging time, human interventions, and system recovery. Confirm whether new robots require major software changes or additional infrastructure. Also check data ownership and cybersecurity controls. I have seen purchase plans focus heavily on peak capacity while ignoring quiet-season utilization. That assumption needs challenging. Flexible fleets, modular charging, and open integration tools can reduce future risk, but only when operators receive practical training and clear procedures. A realistic business case includes failure scenarios, labor changes, and the cost of pausing operations during upgrades.

10 AGV AMR Buying Tips for Global Buyers? - Calculate Total Ownership Costs, Service Needs, and Scalability
No. Buying Dimension What to Calculate or Verify Indicative Planning Data TCO / Operational Impact Required Evidence
1 Define the Transport Requirement Document payload, load dimensions, pickup and drop-off points, travel distance, floor conditions, gradients, aisle width, and required moves per hour. Common industrial payload classes range from approximately 100 kg to more than 1,000 kg. Required capacity should normally include a 15%–25% operating margin. Underspecification can cause missed deliveries, safety risks, and premature replacement. Overspecification increases capital cost and reduces utilization. Process map, SKU/load list, route survey, floor inspection, and a measured baseline of current transport volume.
2 Compare Total Acquisition Cost Include the vehicle, navigation hardware, fleet software, chargers, safety equipment, installation, site preparation, integration, commissioning, training, taxes, and shipping. For industrial projects, integration and commissioning can add roughly 15%–40% to equipment purchase cost, depending on site complexity and interfaces. A low equipment quotation may become expensive after software licenses, network upgrades, engineering work, and acceptance testing are added. Itemized quotation, installation scope, software license terms, shipping responsibilities, and a written acceptance-test plan.
3 Calculate Five-Year TCO Use: TCO = purchase and integration cost + energy + labor + maintenance + spare parts + software + facility changes + downtime − residual value. A practical review period is 5 years. Annual maintenance and support are often budgeted at approximately 3%–8% of equipment capital cost, excluding major damage. TCO exposes recurring costs that are not visible in the initial purchase price and enables comparison with manual labor or conventional vehicles. Five-year cost model with sensitivity cases for labor rates, utilization, energy prices, battery replacement, and downtime.
4 Measure Throughput and Utilization Verify sustained moves per hour, average cycle time, empty travel, waiting time, loading time, traffic delays, and peak-hour demand. For a representative route, calculate throughput from actual cycle time rather than catalog speed. A utilization target of approximately 60%–80% leaves capacity for variability and growth. High theoretical speed does not guarantee high output if vehicles queue at stations, doors, elevators, or charging points. Site simulation, time-study data, peak-shift test, and documented performance under representative load conditions.
5 Evaluate Battery and Charging Strategy Compare opportunity charging, battery swapping, and scheduled charging. Check operating hours, charging time, usable battery capacity, ambient temperature, and charging-space requirements. Industrial battery service life commonly varies from approximately 2–5 years, depending on chemistry, depth of discharge, temperature, and charging practice. Charging downtime, spare batteries, chargers, ventilation, and battery disposal can materially affect labor savings and facility cost. Battery warranty, expected cycle life, charging profile, replacement price, charging-failure procedure, and end-of-life recycling plan.
6 Set Service and Uptime Requirements Define preventive-maintenance intervals, remote diagnostics, response time, repair time, spare-parts availability, local technicians, and escalation procedures. For material-handling automation, an availability objective of approximately 95%–99% may be appropriate, depending on process criticality and redundancy. One hour of downtime should be valued using lost production, delayed shipments, overtime, recovery labor, and customer-service effects. Service-level agreement, regional support coverage, parts lead times, maintenance checklist, uptime definition, and escalation contacts.
7 Check Safety and Compliance Assess speed limits, obstacle detection, emergency stops, warning signals, pedestrian interaction, rack and door interfaces, risk assessment, and local regulatory requirements. Safety performance should be validated in the actual operating environment; nominal sensor range or speed alone is not sufficient evidence. Insufficient safety design can increase injury risk, project delays, insurance exposure, and retrofit cost. Application-specific risk assessment, safety validation records, operating manuals, training plan, and conformity documentation applicable to the destination market.
8 Verify Software and Integration Review interfaces with warehouse, manufacturing, enterprise, conveyor, door, lift, barcode, and access-control systems. Confirm data ownership and cybersecurity responsibilities. Integration effort can range from several weeks for a standardized pilot to several months for multi-system, multi-site deployment. Closed interfaces may create recurring customization fees, slow future expansion, and increase dependency on a single solution provider. API documentation, integration architecture, cybersecurity controls, user permissions, data-export capability, license model, and change-management process.
9 Plan for Scalability and Flexibility Determine how additional vehicles, routes, sites, shifts, payload types, and workflows will be added without redesigning the entire system. A scalable deployment should support phased expansion, such as a pilot followed by additional vehicle groups, while maintaining centralized fleet visibility. Modular expansion reduces the risk of overbuying at launch and helps align capital expenditure with proven operational demand. Expansion pricing, fleet-size limits, site licensing, multi-site architecture, spare capacity, route-editing tools, and compatibility policy.
10 Validate ROI with a Pilot Compare current labor, transport time, errors, damage, safety incidents, and throughput with measured pilot results. Include training and change-management effort. Many automation business cases target a simple payback period of approximately 2–4 years, but the result depends heavily on utilization, labor cost, uptime, and integration expense. A pilot reduces technical and financial uncertainty before a full rollout and identifies process changes needed for sustainable benefits. Baseline-versus-pilot KPI report, agreed success criteria, acceptance test, operator feedback, total cost update, and implementation risk register.
Planning note: The ranges shown are indicative budgeting benchmarks for preliminary comparison, not supplier quotations or guaranteed performance. Final values should be confirmed through a site survey, technical validation, local compliance review, and a five-year sensitivity-based TCO model.

Verify Suppliers Through Testing, Compliance, and Support Standards

Global AGV and AMR procurement should begin with evidence, not attractive brochures. A supplier should provide test records for payload, stopping distance, localization, battery endurance, and recovery after obstruction. Request videos and raw data from controlled warehouse trials. Then repeat critical tests at your site. Floors, lighting, Wi-Fi traffic, and pallet quality can change results. A machine that performs well in a showroom may hesitate beside a dusty loading bay.

Compliance must be practical. Ask for risk assessments, safety-function records, electrical documentation, and region-specific declarations. Check whether manuals cover emergency stops, maintenance isolation, software updates, and operator training. Do not accept certificates with unclear scope or expired dates. Your legal and safety teams should map applicable requirements before purchase orders are released. This step feels slow. It prevents expensive surprises.

Support standards deserve equal scrutiny. Require response times, spare-parts availability, remote-diagnostic rules, cybersecurity controls, and escalation contacts in writing. Ask how faults are logged and how uptime is measured. A supplier may promise 24-hour help, but define whether that means acknowledgment or resolution. Request references from operations with similar shifts, floor layouts, and labor conditions. We have seen capable systems underperform when training was rushed. That weakness is easy to miss. No supplier is perfect, and neither is every test plan.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.