


Global projects rarely fail because a pipe looks unsuitable on paper. They fail when material certificates, welding procedures, pressure data, and site conditions do not align. This is where Astm A106 Pipe earns attention. It is a seamless carbon steel pipe designed for high-temperature service, making it a practical option for process lines, refineries, power plants, and industrial utilities.
Dr. James R. Davis, a senior materials engineer specializing in pressure piping, states, “Reliable pipe selection begins with understanding temperature, stress, chemistry, and installation conditions together.” That principle deserves careful consideration. ASTM A106 compliance alone does not guarantee project success. Engineers must verify the correct grade, wall thickness, heat treatment, dimensional tolerance, and hydrostatic testing records. Grade B is widely selected, yet Grade C may suit applications requiring greater tensile strength. The decision should follow calculations, not habit.
Field experience also exposes uncomfortable details. A pipe can meet the standard and still create delays when markings are unclear. Poor storage can invite surface damage. Inadequate welding control can weaken an otherwise sound system. Small oversights become expensive offshore or remote-site problems. Astm A106 Pipe offers recognized performance, but it is not a shortcut around engineering judgment. Buyers should compare mill documentation, inspection plans, coating needs, and regional delivery reliability before placing an order. The standard is strong. The project review must be stronger.
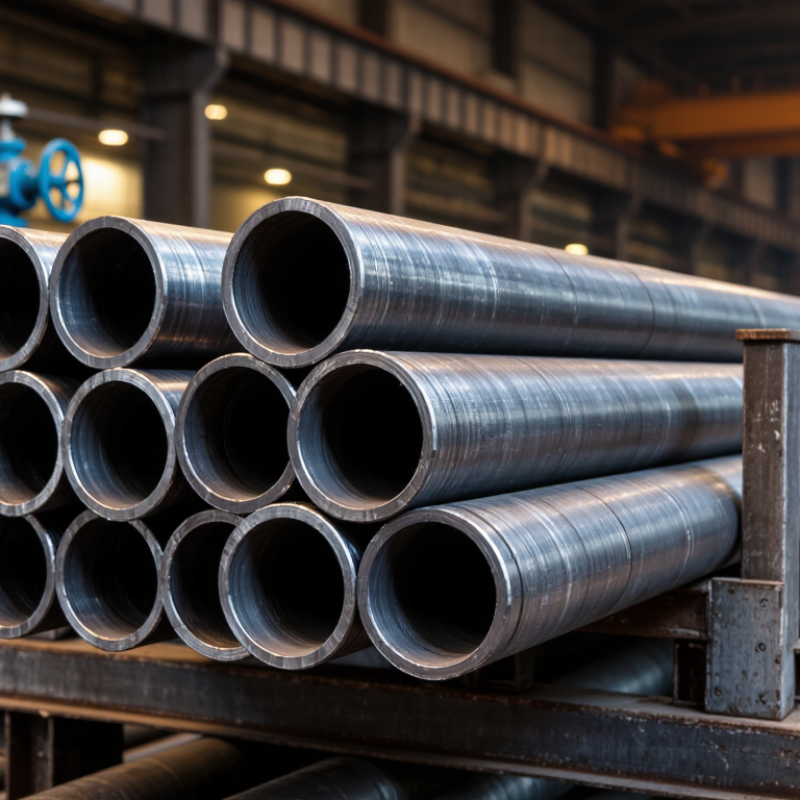
ASTM A106 Pipe: Definition, Scope, and Key Specifications
ASTM A106 pipe is a seamless carbon steel pipe designed for high-temperature service. It commonly carries steam, water, oil, and gas through process plants, refineries, and power facilities. Its scope covers Grades A, B, and C, with Grade B frequently selected for balanced strength and availability.
Grade B provides a minimum tensile strength of 60 ksi and a minimum yield strength of 35 ksi. Grade A is less strong, while Grade C offers higher strength. The specification also controls chemical composition, tensile properties, bending performance, hydrostatic testing, and dimensional tolerances. Project engineers should verify wall thickness against design pressure, temperature, corrosion allowance, and applicable piping codes. A pipe certificate alone cannot replace field inspection.
The specification fits demanding networks. The U.S. Energy Information Administration reported global natural gas consumption of about 4.1 trillion cubic meters in 2023, supporting continued investment in thermal and gas infrastructure. World Steel Association data recorded approximately 1.89 billion tonnes of crude steel production that year. These figures show the scale of industrial construction, but they do not guarantee suitable pipe quality. Each shipment still needs heat-number traceability, test records, and dimensional checks. Small errors matter. A practical review should also question whether seamless A106 is necessary, because design conditions and lifecycle costs may favor another compliant material.
ASTM A106 is a seamless carbon steel pipe specification for high-temperature service. Its three grades are A, B, and C. Grade A has a minimum tensile strength of 330 MPa and yield strength of 205 MPa. Grade B reaches 415 MPa tensile strength and 240 MPa yield strength. Grade C provides the highest values, at 485 MPa and 275 MPa.
These figures describe minimum performance, not guaranteed design pressure. Grade A usually suits less demanding service, while Grade B is widely selected for steam, process, and refinery piping. Grade C may support heavier mechanical demands, but its higher strength does not automatically make it the best choice. Temperature, wall thickness, welding procedure, corrosion allowance, and local code requirements still control the decision. They matter in practice.
During inspection, engineers should review mill test certificates, heat numbers, dimensions, and hydrostatic test records. A pipe may meet the grade requirements yet fail a project need because of incorrect wall thickness or poor installation control. I have seen specifications focus heavily on strength and overlook fabrication details. That approach deserves reconsideration. ASTM A106 also requires attention to tensile testing, yield testing, elongation, and acceptable manufacturing quality. Actual project conditions should be checked against the current ASTM edition and applicable design code.
ASTM A106 seamless carbon steel pipe is specified in Grades A, B, and C. The minimum tensile strength increases from 330 MPa for Grade A to 485 MPa for Grade C, while the minimum yield strength increases from 205 MPa to 275 MPa. These standardized mechanical properties support material selection for high-temperature and high-pressure service.
ASTM A106 pipe is commonly selected for high-temperature, pressure-related service. Its seamless construction reduces risks linked to welded seams. In practice, production begins with a solid steel billet. The billet is heated, pierced, and formed through controlled rolling. Some sizes may receive cold finishing for tighter dimensions. Heat treatment then helps balance strength, toughness, and uniformity.
Quality control must continue beyond the forming line. Manufacturers should verify chemical composition through controlled laboratory testing. Tensile strength, yield strength, and elongation require documented mechanical tests. Hydrostatic testing checks pressure resistance, while approved nondestructive testing can reveal internal flaws. Wall thickness, outside diameter, straightness, and end condition also need inspection. Each pipe should carry clear identification and traceable records.
A certificate alone is not enough. Experienced inspectors compare test results with the purchase specification and project conditions. They also review furnace practices, calibration records, and sampling methods. This step often exposes small inconsistencies before shipment. One detail is easy to miss. ASTM A106 compliance does not automatically satisfy every local code or engineering requirement. Project teams should confirm temperature limits, testing extensions, impact requirements, and documentation needs early. In my experience, rushed verification creates expensive questions later. Even a well-made pipe can become unsuitable when its dimensions, grade, or inspection records do not match the design.
ASTM A106 pipe is designed for seamless carbon steel service at elevated temperatures. It is commonly selected for steam, process fluids, and hot oil lines. Its strength remains dependable when systems face heat and internal pressure. However, temperature ratings are not universal. Grade, wall thickness, diameter, and design code all influence safe operation. A pipe that performs well at 200°C may require a different assessment at 450°C.
Pressure service depends on more than a stamped specification. Engineers should check allowable stress, corrosion allowance, joint design, and pressure cycling. ASTM A106 supports consistent material verification through heat numbers, chemical analysis, tensile testing, and dimensional inspection. These records improve traceability across international projects. In field experience, small documentation gaps can delay installation more than manufacturing defects. That is easy to underestimate.
Tips: Match the pipe grade to the actual medium and operating temperature. Confirm wall thickness after corrosion allowance. Review mill certificates before shipment. Inspect bevels and surfaces on arrival. Do not rely on nominal pressure tables alone. A qualified engineer should verify the complete piping design under the applicable project code. Also, ask whether insulation, thermal expansion, or frequent shutdowns could change service performance. The practical answer is not always the most obvious one.
ASTM A106/A106M is widely specified for seamless carbon steel pipe in high-temperature service. Its established chemistry, tensile requirements, and hydrostatic testing support predictable engineering decisions. However, “global standard” does not mean universal acceptance. Engineers must compare ASTM requirements with ASME B31.1, ASME B31.3, EN 10216-2, and local pressure-equipment rules. Documentation matters as much as the pipe wall.
The International Energy Agency’s Oil 2024 report projects global oil demand at 105.4 million barrels per day by 2030. That outlook supports continued investment in refineries, steam systems, and process facilities. A106 is suitable for many above-ground piping runs carrying hot water, steam, and hydrocarbons. Temperature, pressure, corrosion allowance, diameter, and welding procedures should guide selection. A cold coastal site may need stronger corrosion controls than a dry inland plant. Small details decide performance.
Procurement teams should verify heat numbers, mill test certificates, dimensional tolerances, and traceability records. Third-party inspection can reduce uncertainty before shipment. Field inspections often find mismatched schedules or incomplete certificates, not dramatic material failures. That is an uncomfortable lesson. A106 is not automatically the best choice for sour service, severe corrosion, or low-temperature impact conditions. A project may need alloy steel, stainless steel, or another qualified specification. The World Steel Association reported global crude steel production of about 1.89 billion tonnes in 2023, but abundant steel does not guarantee correct pipe selection. Availability can influence decisions, sometimes too strongly.
| Dimension | Selection Criterion | Verified Technical Data | Project Application and Practical Consideration |
|---|---|---|---|
| Global Standard | Primary material specification | ASTM A106/A106M covers seamless carbon steel pipe for high-temperature service. The specification includes Grades A, B, and C. | Suitable for engineered piping systems where seamless carbon steel pipe is required for elevated-temperature fluid transport. |
| International Compatibility | Comparable design and procurement references | ASTM A106 is commonly referenced alongside ASME B36.10M for dimensions and ASME B16.5 or ASME B16.47 for compatible flanges, where applicable. | Using a recognized specification and compatible dimensional standards can simplify documentation, supplier qualification, and cross-border procurement. |
| Manufacturing Method | Pipe construction | Seamless pipe is manufactured without a welded longitudinal seam. ASTM A106 pipe is generally supplied in seamless construction. | Useful for high-temperature and pressure service where the project specification favors seamless construction and consistent pressure-boundary integrity. |
| Material Grades | Strength and service selection | Grade B is widely used for general industrial piping. Grade A provides lower minimum strength, while Grade C provides higher minimum tensile and yield strength than Grades A and B. | Select the grade according to design pressure, temperature, code calculations, weldability requirements, and procurement availability—not by grade name alone. |
| Mechanical Performance | Minimum specified properties | Typical ASTM A106 minimum values include: Grade A tensile strength 330 MPa and yield strength 205 MPa; Grade B tensile strength 415 MPa and yield strength 240 MPa; Grade C tensile strength 485 MPa and yield strength 275 MPa. | Design engineers should verify the exact edition of the specification, grade, wall thickness, design code, and allowable stresses before final material approval. |
| Temperature Capability | High-temperature suitability | The specification is intended for high-temperature service, but allowable pressure and temperature are governed by the applicable design code and material allowable stresses. | Commonly considered for steam, hot oil, boiler-related piping, refinery process lines, and high-temperature utility systems. |
| Chemical Control | Composition and weldability | ASTM A106 places limits on elements such as carbon, manganese, phosphorus, sulfur, and silicon. Carbon-equivalent and welding procedure requirements should be checked separately. | Review mill test certificates and welding qualifications when the project includes field welding, preheating, post-weld heat treatment, or sour-service restrictions. |
| Dimensional Selection | Outside diameter and wall thickness | Nominal pipe size and schedule are commonly selected using ASME B36.10M dimensions. Actual outside diameter and wall thickness must match the approved piping class. | Confirm design pressure, corrosion allowance, mechanical loads, allowable stress, internal diameter, and connection requirements before choosing the schedule. |
| Pressure Design | Wall-thickness verification | Pipe suitability cannot be determined from nominal size alone. Required wall thickness depends on design pressure, design temperature, material stress, weld factors where applicable, and corrosion allowance. | Use the governing piping or pressure-vessel code for calculations. Do not substitute nominal schedule selection for a complete engineering review. |
| Common Applications | Industrial fluid transport | Typical applications include steam lines, process piping, boiler systems, heat-exchanger connections, petroleum refining, power generation, and high-temperature water service. | Confirm whether the service contains chlorides, hydrogen sulfide, oxygen, acids, or other aggressive media that may require a different alloy or additional controls. |
| Corrosion Consideration | Environmental resistance | ASTM A106 is carbon steel and does not provide stainless-steel-level resistance to general corrosion, pitting, or specialized chemical environments. | Consider corrosion allowance, internal lining, external coating, cathodic protection, insulation design, chemical control, or an alternative alloy when required by the service environment. |
| Inspection and Testing | Quality verification | Typical requirements include chemical analysis, tensile testing, hydrostatic testing, dimensional inspection, and visual examination. Additional nondestructive examination may be specified by the purchase order or project code. | Define inspection scope, test pressure, acceptance criteria, traceability, and documentation requirements before placing the order. |
| Traceability | Documentation package | Project records commonly include material test certificates, heat or batch identification, dimensional reports, hydrostatic test results, inspection records, and compliance statements. | Strong traceability supports customs clearance, third-party inspection, construction turnover, maintenance records, and future replacement planning. |
| Welding and Fabrication | Installation requirements | Carbon steel pipe can generally be welded using qualified procedures, but preheat, interpass temperature, consumable control, and post-weld heat treatment depend on thickness, grade, service, and governing code. | Coordinate pipe material, fittings, flanges, welding procedures, welder qualifications, and heat-treatment requirements before fabrication begins. |
| Project Economics | Lifecycle value | Carbon steel is often selected for its broad availability, established fabrication practices, and compatibility with common industrial piping systems. | Compare purchase price with coating, insulation, corrosion management, inspection, maintenance, replacement, and downtime costs over the project lifecycle. |
| Procurement Risk | Supplier and delivery qualification | International projects should verify specification edition, grade, size range, schedule, end preparation, quantity, testing requirements, and delivery condition before award. | Use approved technical submittals, inspection hold points, packaging requirements, and clear Incoterms to reduce cross-border delivery and conformity risks. |
| Final Selection Rule | Engineering approval | ASTM A106 is appropriate when the service, design code, temperature, pressure, corrosion environment, dimensions, fabrication method, and documentation requirements are compatible. | Make the final selection through the project piping class and engineering review rather than relying solely on the ASTM designation. |


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

