10 Best Hydraulic Fittings for Global Buyers?

Choosing the right Hydraulic Fittings is more than comparing prices or browsing polished product images. A fitting may look identical to another, yet differ in pressure rating, steel grade, sealing design, or thread accuracy. For global buyers, these small differences can affect leakage, downtime, maintenance costs, and operator safety.

This guide examines ten widely used hydraulic fitting options for international purchasing decisions. It considers practical factors such as working pressure, temperature range, connection type, corrosion resistance, installation space, and replacement availability. It also reviews common standards, including SAE, DIN, BSP, and metric specifications, while recognizing that local requirements may vary. Always confirm technical documents with a qualified engineer before final approval.

Real purchasing experience shows that the cheapest fitting is rarely the lowest-cost choice. A damaged O-ring, mismatched thread, or poorly protected shipment can create expensive problems at the installation site. Ask suppliers for material certificates, pressure-test records, dimensional drawings, and batch traceability. Check whether packaging can withstand long ocean transport, humidity, and repeated handling.

Details matter most.

The ranking is not absolute. A compact stainless-steel fitting may suit a coastal machine, while a plated carbon-steel model may serve a protected factory system better. Some suppliers provide excellent samples but inconsistent production batches. That risk deserves attention. This overview offers a practical starting point, not a substitute for application testing, supplier audits, or professional engineering judgment. By comparing performance, documentation, service support, and total ownership cost, buyers can make more reliable decisions across different markets.
10 Best Hydraulic Fittings for Global Buyers?

Define Global Buyer Criteria Using ISO 8434, SAE J514, and DIN 2353

10 Best Hydraulic Fittings for Global Buyers?

Global buyers should define fitting criteria before comparing price or delivery. ISO 8434, SAE J514, and DIN 2353 provide different design languages. They are not automatically interchangeable. ISO 8434 covers several metric and inch connection types. SAE J514 focuses on hydraulic tube fittings, including 37-degree flared connections. DIN 2353 uses metric tube sizes and controlled cutting-ring geometry. Check thread form, sealing method, tube diameter, pressure rating, and material together.

Market data supports careful selection. The Business Research Company’s 2024 Hydraulic Fittings Global Market Report forecasts continued market growth through 2028, driven by construction, industrial machinery, and mobile equipment. Growth does not reduce technical risk. A mismatched thread can leak before the machine reaches full load. Field audits often find incorrect tube-wall assumptions and unverified torque values. Small errors become expensive downtime.

Use the standard printed on the drawing, not only the fitting’s appearance. Confirm dimensions with calibrated gauges and request test evidence for pressure, vibration, and corrosion resistance. ISO 8434 may suit international procurement, while SAE J514 remains practical for many North American systems. DIN 2353 is often efficient for metric machinery. Yet regional practice can mislead. Supplier certificates deserve review, but they are not a substitute for incoming inspection. That extra step feels slow, and sometimes it is. It can still prevent a failure hidden inside a crowded hydraulic cabinet.

Compare 10 Hydraulic Fitting Types Across 3,000–10,000 psi Ratings

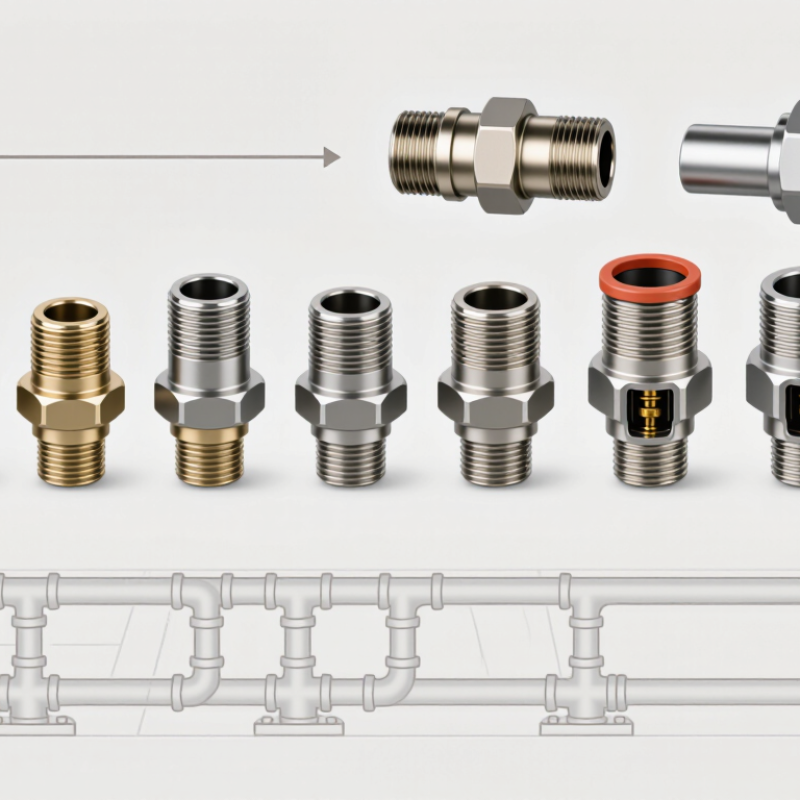
Hydraulic fittings must be compared by working pressure, not appearance. Across 3,000–10,000 psi systems, ten common types deserve careful review: JIC flare, ORFS, SAE O-ring straight thread, NPT, BSPP, BSPT, metric 24-degree cone, bite-type tube, SAE split-flange, and high-pressure quick-disconnect fittings. Their ratings change with size, material, temperature, and assembly quality.

JIC flare fittings suit many mobile systems near 3,000–6,000 psi and tolerate repeated assembly. ORFS fittings control leakage better, especially with vibration. SAE O-ring ports seal reliably, but damaged grooves can cause slow leaks. NPT and BSPT threads are practical, yet thread sealant and over-tightening create risks at higher pressure. BSPP fittings need a sealing washer or bonded seal. They should not be treated like tapered threads.

Metric cone and bite-type fittings often perform well around 4,000–6,000 psi when tubes are prepared correctly. SAE split-flange fittings handle large flow paths and can reach approximately 6,000–10,000 psi in suitable configurations. High-pressure quick disconnects may support 10,000 psi, but only dedicated models qualify. Standard couplers usually do not. Ratings are not universal. I have seen clean-looking assemblies fail because a tube was slightly oval or a seal was reused. Small errors matter. Check the manufacturer’s pressure table, impulse rating, temperature range, and compatible fluid before installation. A perfect fitting cannot rescue poor alignment.

Match NPT, BSPP, BSPT, and Metric Threads for Global Compatibility

10 Best Hydraulic Fittings for Global Buyers

Choosing hydraulic fittings for global projects requires more than matching outside diameter. Thread standards can look similar but seal differently. NPT uses a tapered thread and usually seals through thread interference or approved sealant. BSPT is also tapered, yet its 55-degree thread angle differs from NPT’s 60 degrees. They should not be forced together. BSPP is parallel and commonly needs a bonded washer, O-ring, or sealing seat. Metric threads are usually parallel, with pitch measured in millimeters. A correct match protects pressure performance and reduces leakage risk.

Tips: Check the thread with a gauge, not eyesight. Measure diameter, pitch, and thread form. Confirm whether the port is NPT, BSPP, BSPT, or metric before ordering. I have seen projects fail because “one-quarter inch” was treated as a complete specification. It is not. A one-quarter NPT fitting may not connect safely to a similarly sized BSPT port. Always verify pressure ratings, fluid compatibility, temperature range, and fitting material. Keep a thread identification chart near the assembly bench.

For international sourcing, request clear technical drawings and sample measurements. Confirm the sealing method, wrench dimensions, and required adapter type. A conversion fitting can solve compatibility problems, but it also adds length and possible leak points. This detail is sometimes missed. My own review process would be stricter now: identify every port first, then select fittings by standard, pressure, and service conditions. Small thread differences can create expensive downtime.

10 Best Hydraulic Fittings for Global Buyers? - Match NPT, BSPP, BSPT, and Metric Threads for Global Compatibility

No. Fitting Type Typical Thread Configuration Thread Standard Typical Size Examples Sealing Method Best Application Global Compatibility Guidance
1 Straight Male Adapter Tube connection to male pipe thread NPT, BSPT, BSPP, or metric 1/4, 3/8, 1/2, 3/4 in; M12, M14, M16, M18 Thread sealant for NPT/BSPT; O-ring or bonded seal for parallel and metric ports Connecting hydraulic tubing to pumps, valves, manifolds, and cylinders Select the adapter by matching both the thread form and the sealing face; do not mate NPT directly with BSP threads.
2 Female-to-Female Union Female pipe thread on both ends NPT-to-NPT, BSPP-to-BSPP, or BSPT-to-BSPT 1/8 to 1 in nominal pipe sizes Thread sealing; BSPP requires a suitable face seal or sealing washer Joining two male-threaded components in a compact installation Use the same thread standard on both ends unless the union is specifically manufactured as a conversion adapter.
3 45-Degree Elbow Tube or hose connection with a 45-degree change of direction NPT, BSPP, BSPT, or metric port versions 6 to 25 mm tube; 1/4 to 1 in pipe thread O-ring face seal, bonded seal, or thread sealant depending on port design Reducing hose stress while maintaining smoother flow than a sharp bend Confirm orientation, tube outside diameter, and thread type before ordering.
4 90-Degree Elbow Perpendicular tube, hose, or pipe connection NPT, BSPP, BSPT, metric, or ISO 6149 port connection 6, 8, 10, 12, 16 mm tube; 1/4 to 1 in thread O-ring, bonded washer, or tapered-thread sealant Compact routing around cylinders, control valves, and machine frames Choose an adjustable or fixed orientation according to assembly space and hose alignment.
5 Tee Fitting Three-way connection with equal or reduced outlets NPT, BSPP, BSPT, or metric tube-and-port versions 6 to 25 mm tube; 1/4 to 1 in ports O-ring or compression seal for tube ends; thread sealant or washer at ports Splitting a hydraulic line or connecting a pressure gauge branch Use a reducing tee when branch flow demand differs from the main circuit.
6 Bulkhead Fitting Pass-through connection for panels, tanks, or guards NPT, BSPP, BSPT, and metric threaded designs M14 to M30; 1/4 to 1 in pipe thread Locknut with O-ring, bonded seal, or sealing washer Routing lines through hydraulic reservoirs, mounting plates, and enclosures Check panel thickness, hole diameter, locknut clearance, and seal location.
7 Banjo Fitting Hollow bolt and eye connection for low-profile routing Metric or unified bolt threads; port options may include BSPP or NPT M10, M12, M14, M16; commonly used with small and medium hose sizes Copper, aluminum, or bonded sealing washers Tight spaces near pumps, motors, brake systems, and mobile equipment Verify bolt length, eye thickness, washer material, and flow-hole diameter.
8 Test Point Adapter Pressure-measurement port with a mini test connection Metric, BSPP, or NPT mounting thread; test interface varies M10, M12, M14; 1/4 or 1/8 in ports O-ring, bonded seal, or tapered thread sealant Fast pressure checks, commissioning, diagnostics, and preventive maintenance Match the adapter to the test hose or gauge coupling and confirm the pressure range.
9 Tube Union Straight connection between two equal tube outside diameters Metric tube, inch tube, or dual-standard conversion design 6, 8, 10, 12, 15, 16, 18, 22 mm; 1/4, 3/8, 1/2 in Compression ferrule, bite-type sleeve, or O-ring tube seal Repairing or extending rigid hydraulic tubing without changing direction Tube outside diameter is critical; nominal pipe size is not interchangeable with tube size.
10 Flange-to-Thread Adapter SAE-style or split-flange port to threaded outlet ISO 6162 flange interface with NPT, BSPP, or metric thread 1/2 to 2 in flange sizes; M16 to M48 thread ranges O-ring flange seal plus O-ring, bonded seal, or thread seal at the outlet High-flow lines, pumps, motors, manifolds, and vibration-prone systems Confirm flange code, pressure class, port orientation, O-ring groove, and bolt pattern.
Selection note: NPT and BSPT are tapered pipe threads that normally seal on the threads. BSPP is a parallel thread and generally requires an O-ring, bonded seal, or sealing washer. Metric hydraulic ports commonly use O-ring or bonded-seal designs. Actual working pressure depends on material, size, temperature, fluid, tube or hose connection, and the applicable fitting standard; always verify the supplier's pressure rating before installation.

Assess Steel, Stainless Steel, and Brass Against 316L Corrosion Data

10 Best Hydraulic Fittings for Global Buyers?

Hydraulic fittings must survive pressure, vibration, temperature changes, and corrosion. Carbon steel offers high strength and low cost, but exposed moisture can produce red rust quickly. Paint or plating helps, yet scratches often become early failure points. I have seen fittings look sound outside while threads weakened internally.

Stainless steel performs better in humid and chemical environments. 316L is a useful corrosion benchmark because its molybdenum content improves resistance to chloride pitting. Its PREN is commonly around 24–26, although laboratory values cannot predict every field condition. Salt concentration, stagnant fluid, temperature, and crevices can change results sharply. Brass resists ordinary water well and machines easily, but aggressive water may cause dezincification. The surface can remain bright while losing structural strength. That detail is easy to miss.

Tips: Match the fitting to the actual fluid, not just the pressure rating. Check chloride levels, operating temperature, and cleaning chemicals. Avoid mixing dissimilar metals without reviewing galvanic risk. Inspect threads and sealing faces after installation. A 316L fitting is not automatically the safest choice; poor design, contamination from steel tools, or trapped water can still create corrosion. I would also request test data from the supplier, while remembering that test conditions may not match your pipeline.

Verify Leakage, Assembly, and Durability Under ISO 19879 Test Methods

Choosing among the ten best hydraulic fittings requires more than comparing pressure ratings. ISO 19879 test methods provide a practical basis for checking leakage, assembly performance, and durability. Buyers should request test reports covering proof pressure, burst pressure, impulse testing, and leakage inspection. The connection must remain dry.

In real workshops, assembly quality often changes the result. I have seen correctly specified fittings leak because tubes were cut unevenly or installed with side loading. Inspect tube ends, remove burrs, and follow the documented tightening procedure. Record torque, test pressure, fluid temperature, and holding time. Small details matter. A clean fitting can still fail after careless installation.

Durability testing should reflect field conditions, not only a short bench test. Repeated pressure cycles, vibration, temperature changes, and fluid compatibility can expose weaknesses. ISO 19879 results improve confidence, but they do not replace application-specific validation. Ask whether the tested configuration matches your tube material, size, seal design, and working pressure. A report with missing setup details deserves questions. This may feel inconvenient, yet incomplete evidence can create expensive downtime later. Also inspect fittings after testing, because hidden deformation may not cause immediate leakage.

This buyer comparison covers ten common hydraulic fitting configurations without using company or brand data. The values show ISO 19879 verification reference levels as multiples of the fitting's maximum allowable working pressure (MAWP): leakage testing at 1.0× MAWP, proof testing at 1.5× MAWP, and burst testing at 4.0× MAWP. These are test-method reference points, not product performance claims. Buyers should also confirm assembly instructions, material compatibility, tube size, temperature range, and documented test results.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.