


Choosing the right Hb88509 Center Bearing is not a simple matter of matching a part number. It requires careful attention to vehicle application, shaft design, bearing dimensions, and operating conditions. A bearing may look correct on a workbench yet fail after several weeks on the road. That risk deserves respect.
Driveline engineer Elena Marquez explains, “A center bearing should be selected by fit, load capacity, alignment, and service environment—not by appearance alone.” Her advice reflects practical workshop experience. Measure the inner diameter, outer diameter, and mounting width before ordering. Check the rubber support for stiffness, cracks, and correct bonding. Confirm the bearing’s internal clearance and seal design. A dusty construction vehicle may need stronger protection than a lightly used passenger vehicle.
Start with the manufacturer’s catalog and verify every cross-reference. Compare the original bearing with the proposed Hb88509 Center Bearing. Look for differences in flange shape, grease specification, and shaft support position. Small errors can create vibration, humming, or uneven universal-joint angles. These symptoms often appear during acceleration. Sometimes, the real problem is not the bearing.
Installation also matters. Press only against the correct bearing race. Do not hammer the inner ring directly. Keep the driveshaft aligned with its original marks. Incorrect preload can shorten service life dramatically. Still, no selection method is perfect. Catalog information may contain gaps, and vehicle modifications can confuse the process. When measurements disagree, pause and recheck them. A trusted supplier, verified technical data, and experienced inspection provide the safest path toward choosing the right Hb88509 Center Bearing.
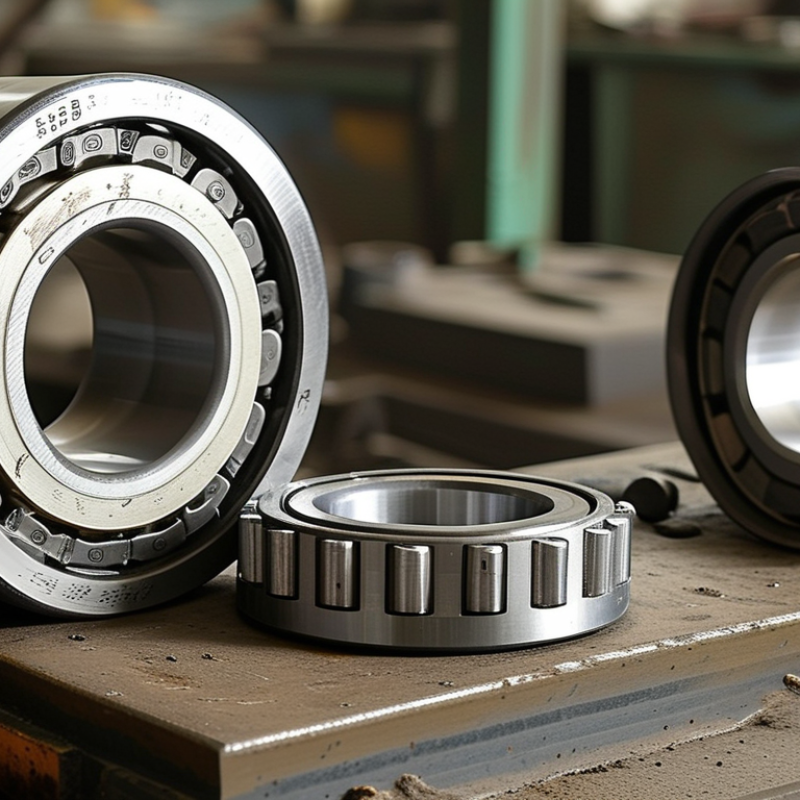
An Hb88509 center bearing is a support assembly for a vehicle’s propeller shaft. It holds the rotating shaft near its midpoint and reduces vibration as torque travels toward the differential. The assembly normally includes a bearing, rubber isolator, inner sleeve, and mounting bracket. It is not simply a universal bearing. Small differences matter. Shaft diameter, bolt spacing, bearing width, and rubber stiffness must match the vehicle’s original design.
Identification should begin with measurements, not appearance. Check the shaft diameter with a caliper, then measure the bracket holes and bearing offset. Compare these details with the vehicle’s service manual and the part’s engineering drawing. ISO 281 defines L10 bearing life as the operating life reached by 90% of identical bearings under stated conditions. That figure is useful, but it does not predict rubber fatigue, water exposure, poor alignment, or harsh road impacts.
A suitable Hb88509 bearing should also match load direction, rotational speed, temperature range, and sealing requirements. A 2023 report from the International Organization for Standardization on rolling-bearing reliability supports using calculated load ratings rather than visual similarity alone. In practical inspections, a torn rubber support, humming noise, or vibration under acceleration can indicate failure. Still, these symptoms may come from universal joints or shaft imbalance.
I once trusted noise alone; that was a mistake. Verify every dimension before choosing the replacement.
Confirming Hb88509 compatibility starts with your vehicle’s exact configuration. Record the make, model, production year, engine, drivetrain, and wheelbase. Small differences can change the driveshaft length and bearing position. Check the service manual or a trusted parts catalog for the correct reference number. Do not depend on appearance alone.
Measure carefully. Compare the bearing’s inner diameter, outer housing, mounting-hole spacing, and rubber support shape. Also inspect the driveshaft tube and flange area for wear. A matching bearing should sit firmly without forcing the shaft into alignment. It should also match the vehicle’s original mounting position. That detail matters.
Online listings can contain errors. Recheck the number from two reliable sources. A qualified technician can confirm the result using the vehicle identification number and old-part measurements. During installation, mark the shaft orientation before removal. This helps preserve balance. Tighten fasteners evenly, then check for free movement. A short road test should reveal unusual vibration, humming, or clunking.
Do not ignore minor noise. I have seen apparently suitable parts fail because the bracket spacing was overlooked. The lesson is simple: fitment requires measurements, records, and a careful inspection.
How to Choose the Right Hb88509 Center Bearing?
Material and specification choices determine whether an Hb88509 center bearing survives real drivetrain conditions. A high-carbon bearing steel raceway handles repeated radial loads well. However, steel grade alone does not guarantee durability. Check hardness, heat treatment, surface finish, and corrosion protection. The rubber support should remain flexible near the vehicle’s operating temperature. A hardened inner ring is useful, but poor rubber bonding can still cause vibration.
Match the bearing’s bore, outer diameter, width, and mounting position precisely. Confirm the dynamic load rating, static load rating, rotational speed, and allowable misalignment. ISO 281 calculates basic rating life at one million revolutions under the rated dynamic load. That figure is a reference, not a promise. Field contamination, shaft imbalance, and incorrect preload can reduce life sharply. The U.S. Department of Energy’s tribology assessments associate drivetrain friction with approximately 20% of vehicle fuel-energy losses. Smooth rotation matters.
Tips: Measure the shaft before ordering. Do not trust appearance alone. Compare the load rating with the original specification. Inspect seal contact and rubber cracks. A 2023 technical review from the Society of Automotive Engineers also emphasizes temperature, lubrication, and alignment as major bearing-life variables. I would verify those conditions during installation. That step is often skipped. It should not be.
| Selection Dimension | Recommended Specification or Range | Why It Matters | Verification Method |
|---|---|---|---|
| Bearing designation | HB88509 or the exact application-specific equivalent | A similar-looking part number may have different dimensions, seals, or mounting geometry. | Match the complete part number with the vehicle or equipment service manual. |
| Inner bore diameter | Must match the propeller-shaft journal or mounting shaft diameter exactly; do not select by nominal bearing name alone. | An incorrect bore can cause looseness, shaft damage, or installation failure. | Measure the shaft with a calibrated vernier caliper or micrometer at several points. |
| Outer diameter and housing fit | Use the exact housing outside diameter and mounting profile specified for the application. | The housing controls alignment and transfers vibration loads to the vehicle frame or support bracket. | Compare the replacement part with the removed assembly and check mounting-hole position. |
| Bearing steel | Through-hardened high-carbon chromium bearing steel, commonly equivalent to AISI 52100 / 100Cr6. | This steel provides high rolling-contact fatigue resistance, hardness, and wear resistance when correctly heat-treated. | Request the material and heat-treatment specification or supplier certificate. |
| Seal material | Nitrile rubber (NBR) for ordinary automotive temperatures; fluoroelastomer (FKM) for higher heat or chemical exposure. | The seal protects grease from water and dirt while retaining lubricant inside the bearing. | Confirm the seal code, operating-temperature range, and compatibility with the required grease. |
| Seal arrangement | Prefer a double-sealed configuration for exposed propeller-shaft applications, unless the service design specifies otherwise. | Two seals improve resistance to road splash, dust, and lubricant loss. | Inspect the bearing for sealed sides, seal seating, and damage before installation. |
| Cage material | Pressed steel for general automotive use; machined or reinforced polymer designs may be used when specified by the application. | The cage maintains rolling-element spacing and must tolerate the expected speed, heat, and vibration. | Check the technical drawing and ensure the cage type matches the original design. |
| Rubber support compound | Oil-resistant elastomer with a hardness and deflection rate suitable for the original support system. | The rubber support absorbs vibration while keeping the propeller shaft correctly aligned. | Look for cracks, hardening, swelling, or excessive softness and compare the support geometry with the original. |
| Housing material | Stamped or formed steel for high structural strength; aluminum may be used where lower mass and corrosion resistance are specified. | The housing must resist distortion under shaft load, vibration, and vehicle movement. | Check for correct thickness, flat mounting surfaces, corrosion protection, and dimensional stability. |
| Dynamic load capacity | Select a bearing with a basic dynamic load rating equal to or greater than the original application requirement. | Dynamic load rating is used to assess rolling-fatigue life under rotating loads. | Compare the manufacturer’s published C rating with the service calculation or original specification. |
| Static load capacity | The basic static load rating should safely cover shock loads, stationary loads, and installation-related forces. | Insufficient static capacity can produce permanent dents in the raceways or rolling elements. | Review the published C0 rating, especially for heavy-duty or high-shock applications. |
| Internal clearance | Use the clearance class specified for the original assembly; standard clearance is common, while C3 is used only when operating conditions require it. | Clearance affects heat generation, noise, shaft fit, and operating life. | Confirm the clearance code on the bearing or packaging and follow the service specification. |
| Lubricant | Factory-filled, sealed-for-life grease compatible with the seal material and expected temperature range. | Correct grease reduces friction, wear, corrosion, and heat generation. | Do not mix greases unless compatibility is confirmed; replace contaminated or damaged sealed bearings. |
| Operating temperature | Choose seals and grease rated for the measured service temperature, including heat transferred from the exhaust and drivetrain. | Excessive heat can harden seals, degrade grease, and reduce bearing fatigue life. | Use temperature data from the application and compare it with the published operating range. |
| Rotational speed | The permissible speed must exceed the maximum propeller-shaft speed with an appropriate safety margin. | Overspeed can increase vibration, heat, seal wear, and the risk of premature failure. | Compare the bearing’s reference or limiting speed with the vehicle’s maximum shaft speed. |
| Alignment and mounting | The bearing must be centered on the shaft and installed with the support bracket in its original position. | Misalignment causes uneven loading, vibration, seal damage, and accelerated wear. | Inspect the shaft, bracket, fasteners, and mounting surfaces; follow the specified tightening procedure. |
| Environmental resistance | Use corrosion-protected metal surfaces and sealed construction for water, salt, dust, and road-debris exposure. | Road contamination can damage seals, corrode raceways, and contaminate the lubricant. | Check coating quality, seal condition, drainage exposure, and evidence of corrosion after installation. |
Note: The HB88509 designation can vary by application. Always confirm the complete dimensions, load ratings, clearance, seal type, and mounting configuration against the applicable service documentation before purchase or installation.
Choosing an Hb88509 center bearing requires more than checking a low price. Start with the vehicle application, shaft diameter, mounting pattern, and expected load. I once compared two bearings with identical catalog dimensions. One developed vibration within weeks because its rubber support was too soft. That mistake changed my inspection routine.
Quality should be judged through measurable details. Check bearing clearance, seal design, rubber hardness, grease type, and material certificates. Ask whether the unit passed rotation, noise, and load testing. A clean casting and even bolt holes also reveal manufacturing discipline. Request batch numbers and inspection records. Small details matter.
Price comparison should include service life, delivery risk, and installation labor. A cheaper bearing may require earlier replacement, creating extra downtime. Manufacturer support is equally important. Reliable suppliers provide drawings, fitting guidance, warranty terms, and technical replies from trained staff. Ask how they handle vibration complaints and defective samples. Their response before purchase often predicts support afterward. Do not accept vague promises. Compare written specifications, realistic lead times, and replacement procedures. My comparisons are not always perfect, especially when test data is incomplete, so I record assumptions before choosing.
Choosing the right Hb88509 center bearing starts with fit, not appearance. Confirm the bearing number, shaft diameter, bracket shape, and mounting-hole spacing against the vehicle service data. A similar housing can still create harmful misalignment. Check the rubber support for cracks before installation. It should feel firm, not brittle or excessively soft. Measure the old part if the vehicle has been modified.
Work safely. Support the vehicle securely, then mark the driveshaft orientation before removal. This helps preserve correct balance and phasing. Remove dirt from the shaft and mounting area. Slide the new bearing into position without forcing the inner race. Follow the service manual for torque values and bearing pre-load. Do not guess the support position. Rotate the shaft by hand and check for binding, looseness, or contact with nearby components. A rushed installation may feel acceptable but still produce vibration at road speed.
Inspect the center bearing during routine servicing. Look for torn rubber, rust marks, grease leakage, and polished contact areas. A sealed bearing normally needs no added grease. If lubrication is specified, use only the recommended type and amount. Listen for humming or clunking during acceleration and deceleration. Recheck mounting hardware after the initial road test, following the vehicle’s service procedure. I have seen small alignment errors become expensive drivetrain problems. The mistake is easy to miss.
This chart organizes the key inspection points for selecting and servicing a center bearing. Confirm dimensions, compatibility, shaft alignment, fastener security, and rubber-support condition before returning the vehicle to service.
The checklist emphasizes fitment and condition checks rather than brand-specific information. Always compare the replacement bearing with the vehicle service specifications and use the specified tightening procedure for the mounting hardware.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

