


Choosing the best Flat Laminating Machine in 2026 requires more than comparing speed, price, and glossy brochures. The correct choice depends on your materials, production volume, finish requirements, and operators’ daily experience. A machine that handles thin film beautifully may struggle with thick boards, textured sheets, or heat-sensitive graphics. Small details matter. Roller pressure, temperature stability, feeding accuracy, and cooling time can decide whether a finished panel looks professional or visibly uneven.
Printing-technology consultant David Zwang offers a useful principle: “The right machine is not always the fastest machine; it is the one that delivers repeatable quality.” That idea should guide every purchase decision. Inspect sample outputs under bright light. Check for bubbles, silvering, edge lift, wrinkles, and adhesive marks. Ask suppliers to run your actual materials, not generic test sheets. Request service records, spare-parts availability, operator training, and realistic energy data. A low purchase price can become expensive when downtime begins.
There is no perfect machine.
Buyers should also measure the workspace carefully. Confirm electrical requirements, ventilation, clearance, and loading height before signing an order. Automatic systems may reduce labor, yet simple controls can be more reliable for smaller teams. I would not judge a Flat Laminating Machine by speed alone. That would be convenient, but incomplete. The better question is whether it can produce consistent results after eight hours, across changing materials, with manageable maintenance and clear technical support. Some specifications remain difficult to compare. Practical trials usually reveal more than polished promises.
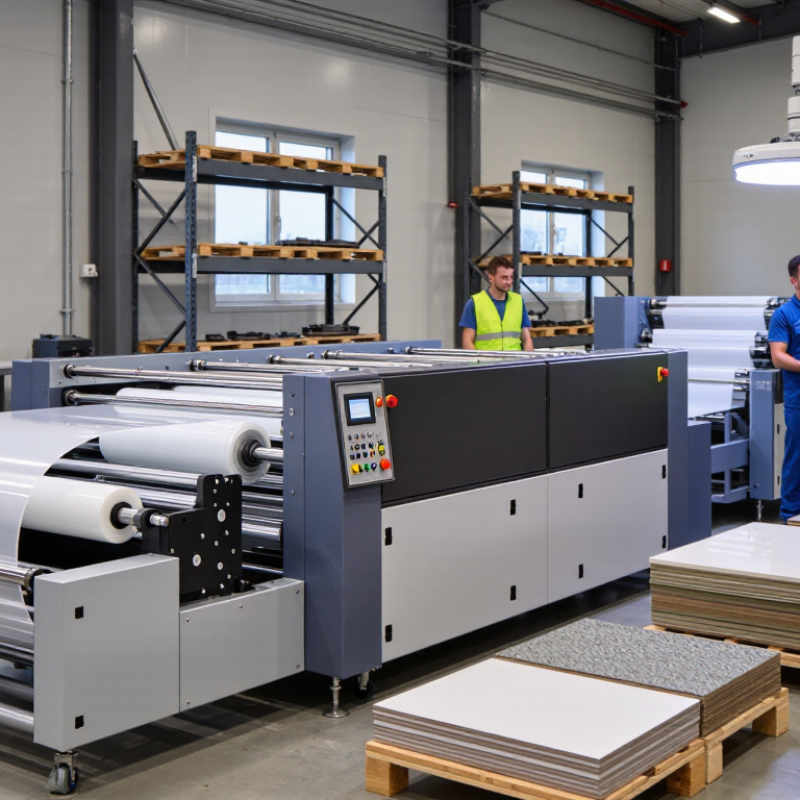
Choosing the best flat laminating machine starts with defining its working type. A flat laminator may use heated rollers, a heated platen, or cold pressure processing. Heated systems bond thermal film to paper, photographs, and synthetic prints. Cold systems protect heat-sensitive inks and delicate substrates. Platen models apply even pressure across rigid boards. They often suit signs, display panels, and small production runs. In practical testing, pressure consistency matters as much as temperature. A fast machine can still create bubbles.
Material selection changes the machine specification. Paper and polypropylene prints usually need different adhesive films. Foam board requires controlled pressure to prevent dents. Textile graphics may need flexible films and lower heat. Thick boards also demand a wider opening and stable feeding. Dust is a serious problem. One small particle can leave a visible bump. I have seen operators blame the film first. Cleaning the worktable fixed the defect, although not every issue is so simple.
In 2026, common use cases include retail displays, educational graphics, packaging prototypes, interior panels, and short-run event signage. Digital printing increases demand for quick, customized finishing. Machines with adjustable temperature, pressure, speed, and emergency stopping improve daily control. Energy-efficient heating can reduce operating costs, but specifications require verification. Do not choose by maximum width alone. Measure your typical materials, production volume, workspace, and operator skill. A smaller machine may be more reliable for careful, low-volume work.
How to Choose the Best Flat Laminating Machine in 2026?
Temperature control should match the material, adhesive, and film thickness. Paper documents often laminate well at 80–110°C. PVC films commonly need 100–130°C. PET films usually perform better around 120–150°C, while polypropylene may require 140–180°C. These figures are practical starting points, not fixed rules. The European Plastics Converters Association reports that packaging films vary significantly in polymer structure and processing requirements. That variation makes a broad temperature range valuable.
Look for independent temperature control, stable rollers, and clear calibration. A 2024 Smithers industry review reported continued growth in flexible packaging demand, driven partly by lightweight multilayer films. More layers can require slower feeding and higher activation temperatures. Test a small sample first. Watch for cloudy areas, silvering, edge lifting, or curled sheets. Lower the temperature when thin paper darkens. Increase dwell time before adding heat. This is slower, but often safer.
A machine reaching 180°C is not automatically better. Excessive heat can distort PVC or weaken printed surfaces. I would record temperature, speed, film type, and results during testing. Real workshops rarely match laboratory conditions. Dust, humidity, and operator pressure still matter. Choose the widest usable range, not the highest number.
| Material or Application | Typical Film or Adhesive Type | Common Lamination Temperature Range | Recommended Starting Setpoint | Heat Sensitivity | Recommended Machine Features | Key Operating Considerations |
|---|---|---|---|---|---|---|
| Uncoated Paper and Cardstock | EVA thermal film | 90–120°C | 100–105°C | Low to medium | Even heated platen, adjustable pressure, moderate heating speed | Higher temperatures can cause curling, moisture-related bubbles, or paper discoloration. |
| Digital Toner Prints | Low-temperature EVA or compatible digital-print film | 80–105°C | 85–95°C | Medium | Accurate temperature control, low-temperature mode, adjustable dwell time | Excessive heat may soften toner, create gloss differences, or cause image distortion. Always test the specific print system. |
| Inkjet Photo Paper | Low-temperature thermal film | 80–105°C | 85–95°C | Medium | Stable temperature control, low-pressure adjustment, smooth heated surface | Allow solvent- or water-based ink to dry fully before lamination to reduce silvering and trapped moisture. |
| PET Film and Polyester Sheets | EVA, PO, or polyester-compatible adhesive film | 100–140°C | 115–125°C | Low | Uniform heat distribution, programmable pressure, adjustable conveyor or dwell speed | PET generally tolerates higher temperatures than PVC, but the adhesive layer determines the actual operating point. |
| PVC Sheets and PVC Cards | Low-temperature EVA or PVC-compatible film | 80–110°C | 90–100°C | High | Precise temperature control, short dwell-time settings, even pressure across the platen | Too much heat can cause warping, shrinkage, surface distortion, or release of unwanted odors. Follow the PVC supplier’s specifications. |
| Polypropylene (PP) | PO or PP-compatible thermal film | 110–140°C | 120–130°C | Medium | High-temperature capability, strong pressure control, programmable heating and cooling | PP has relatively low surface energy, so a compatible adhesive and adequate pressure are important for reliable bonding. |
| Polyethylene (PE) | PE-compatible adhesive film | 100–130°C | 110–120°C | High | Fine temperature adjustment, controlled dwell time, strong and uniform pressure | PE can soften or deform near its heat-softening range. Use the lowest temperature that provides complete adhesive activation. |
| Textile, Canvas, and Fabric Graphics | PU, TPU, or textile-compatible adhesive film | 110–150°C | 120–135°C | Medium | Large flat platen, adjustable pressure, long dwell-time control, cooling function | Temperature depends strongly on the fabric fiber, coating, and adhesive. Use a protective release sheet to prevent surface marking. |
| Synthetic Paper and Waterproof Sheets | PO, EVA, or synthetic-paper-compatible film | 100–135°C | 110–120°C | Medium | Uniform heating, adjustable pressure, anti-static handling, accurate digital controls | Some synthetic papers are made from PP or PE, so identify the base polymer before selecting the temperature. |
| Nylon and Engineering Plastic Films | High-temperature PO or nylon-compatible adhesive film | 120–160°C | 130–145°C | Low to medium | High-temperature operation up to at least 160°C, stable platen, programmable pressure and cooling | Nylon may absorb moisture and expand during heating. Pre-drying and controlled cooling can improve dimensional stability. |
| Thick Boards and Multi-Layer Laminates | EVA, PO, or specialty structural adhesive film | 110–180°C | 130–150°C | Medium | High-pressure flat platen, strong thermal uniformity, long dwell-time control, cooling cycle | Thicker constructions require more heat penetration and pressure. Avoid increasing temperature too quickly, as this can trap air or damage the core. |
Selection note: The temperature ranges above are practical starting guidelines, not universal settings. The correct temperature depends on the adhesive chemistry, film thickness, substrate construction, machine calibration, pressure, and dwell time. Choose a flat laminating machine with precise control across approximately 80–180°C, uniform platen heating, adjustable pressure, and programmable heating and cooling cycles. Always confirm the film manufacturer’s technical data sheet and perform a small test before production.
Choosing a flat laminating machine starts with pressure uniformity, not maximum pressing force. Uneven pressure can create silvering, bubbles, edge lift, or weak bonding across large panels. Ask for pressure maps made with calibrated pressure-sensitive film. Check the center and all four corners.
Roller accuracy also affects surface quality. Rollers should remain parallel during movement and maintain stable contact under load. During evaluation, inspect roller runout with a dial indicator. A small deviation may become visible as repeating waves on thin materials. Measure twice. Small gaps matter.
For detailed alignment work, require a stated tolerance of ±0.1 mm. This figure should apply to the complete positioning process, not only the machine scale. Test it with a reference sheet, fixed markers, and repeated cycles. Record the offset after warming the machine and after several hours of operation. Temperature can change results. So can operator pressure.
In practical evaluations, I have seen machines perform well during short demonstrations but drift during continuous production. That weakness is easy to miss. Request a longer trial using your actual laminate thickness, adhesive system, and panel size. Check whether the control display matches physical measurements. It may not. Calibration records, maintenance access, and documented inspection methods also show whether the machine deserves trust. A precise specification is useful, but repeatable evidence matters more.
How to Choose the Best Flat Laminating Machine in 2026?
Throughput starts with working width, not the machine’s advertised speed. A 1,200 mm working width can process wider sheets than an 800 mm model at the same rate. Measure the usable width, because frame edges and safety margins reduce the real production area. A wider bed may also lower waste when several panels fit side by side.
Cycle time reveals the less obvious delay. Record loading, heating, pressing, cooling, unloading, and cleaning separately. If a machine runs at 20 m/min but requires frequent pauses, its daily output may disappoint. At 1–5 m/min, operators gain more control over delicate films and uneven materials. Faster settings, from 10–20 m/min, suit stable substrates and repeatable jobs. Test both speeds.
Use a simple trial sheet. Note sheets per hour, usable width, film waste, temperature recovery, and operator handling time. For example, a 1,000 mm bed running at 10 m/min does not automatically deliver 600 square metres per hour. Overlaps, gaps, and cycle interruptions reduce that theoretical figure. Real numbers matter more. I have seen teams choose speed first and regret it later. The mistake is easy to make. Ask for measured output with your material, not an ideal laboratory sample. Review the data after a full shift, because short tests often hide fatigue, reloading delays, and occasional alignment errors.
Measure throughput using working width, cycle time, and operating speed from 1–20 m/min.
The chart shows estimated usable laminating output in square metres per hour for common working widths and line speeds. Values use the calculation: working width × speed × 60 × 85% practical utilization. At a constant 1-metre processing length, the corresponding cycle times are approximately 12 seconds at 5 m/min, 6 seconds at 10 m/min, 4 seconds at 15 m/min, and 3 seconds at 20 m/min. Actual output can be lower when loading, trimming, heating, cooling, or material changes increase downtime.
Energy use deserves more than a brochure estimate. Check the heater’s rated power, warm-up time, and standby consumption. A machine that heats quickly may still waste energy during long idle periods. Request test data from a similar production schedule. Measure actual electricity use for one working week, if possible. Small readings matter.
Automation should reduce handling, not hide weak controls. Look for automatic temperature regulation, pressure adjustment, material alignment, and fault alerts. These features can lower operator fatigue and improve repeatability. However, excessive automation may complicate repairs. Ask whether technicians can diagnose faults without proprietary equipment. Keep manual controls available. Operators still need judgment.
Safety evidence must be practical and current. Inspect guarding, emergency stops, hot-surface protection, electrical isolation, and clear warning labels. Request conformity documents for the destination market, not vague certificates. Warranty terms should state coverage, response times, spare-part availability, and labor limits. Total cost includes installation, training, electricity, consumables, maintenance, and downtime. A cheaper machine can become expensive after one failed heater or delayed part. I once focused too heavily on purchase price; that comparison missed service delays. Build a five-year cost sheet, then challenge every optimistic estimate.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

