How to Choose the Best Tray Baking Equipment in 2026?
Choosing the best Tray Baking equipment in 2026 requires more than comparing prices, tray capacity, or glossy automation features. Bakery operators must examine thermal consistency, labor needs, cleaning access, energy consumption, and after-sales support. A crisp crust can hide an uneven oven. One cold corner may damage an entire production batch.
Industry data shows why this decision matters. Mordor Intelligence’s bakery equipment market research identifies automation, energy efficiency, and flexible production as major investment drivers. Grand View Research also reports continued growth in the global bakery products market, supported by changing consumer preferences and expanding industrial production. However, market forecasts differ between research firms. Treat them as planning references, not guaranteed outcomes.
Energy deserves close attention. The U.S. Department of Energy identifies process heating as a major share of industrial energy use, making oven efficiency a practical cost concern. When reviewing equipment, request measured energy data under real production conditions. Ask how many kilowatt-hours are used per tray, not only the rated power. Check heat recovery, insulation thickness, temperature recovery time, and standby consumption.
Experience often reveals what brochures omit. Operators notice difficult-to-reach corners, sticky residue around conveyors, and controls that slow changeovers. Equipment should match your actual products, tray dimensions, batch sizes, and staffing levels. A highly automated line may reduce labor, but it can also increase maintenance complexity.
The perfect machine does not exist. A careful decision combines supplier evidence, factory trials, operator feedback, and a realistic five-year cost calculation. That approach creates a more reliable Tray Baking investment for 2026.
Set Production Targets: 600×400 mm Trays, Batches per Hour, and Peak Load
How to Choose the Best Tray Baking Equipment in 2026?
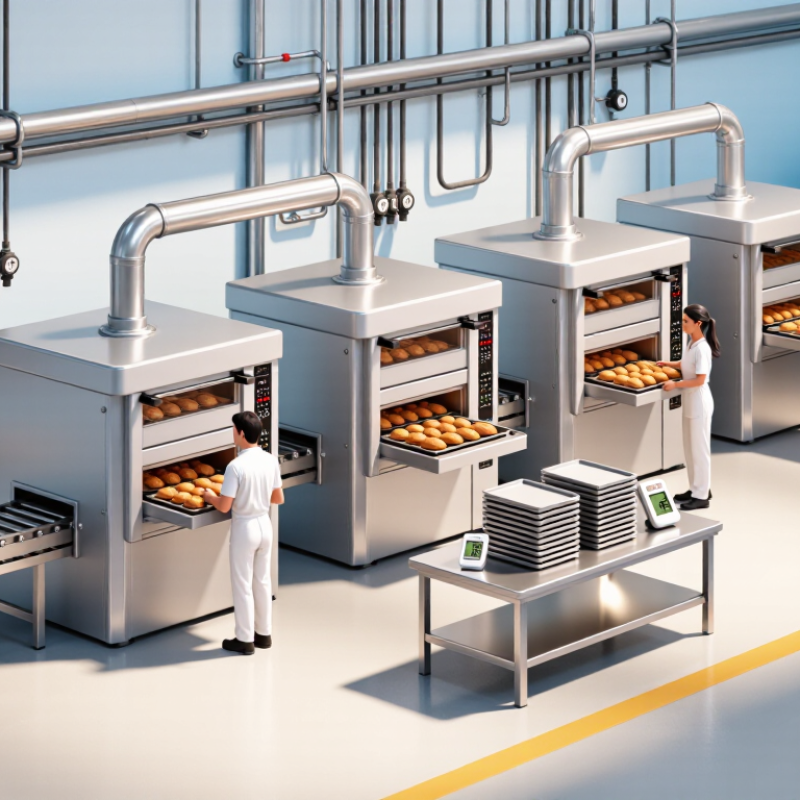
Start with a measurable production target, not a machine catalogue. For 600×400 mm trays, record the required trays per hour, product weight, and baking temperature. A small bakery may need 30 trays hourly, while a central kitchen may require 180. Calculate capacity using actual cycle time, including loading, baking, unloading, and cooling. My first production estimate was too optimistic because I ignored cleaning pauses.
Peak load matters more than average output. If orders rise by 25% on weekends, your equipment should handle that pressure without uneven browning or unsafe heat recovery. Check chamber spacing, trolley movement, electrical demand, and ventilation capacity. A suitable oven should maintain stable temperatures when several trays enter together. Test it with your heaviest product, not an easy sample.
Tips:
Run a timed trial with real 600×400 mm trays. Measure trays per hour, temperature recovery, and staff handling time. Leave practical space around the equipment for cleaning and repairs. Do not rely only on the stated maximum capacity. It may look impressive, but your real output can be lower. Review the figures after one busy week, then adjust the equipment plan.
Match Oven Type to Output: Convection, Rack, or Tunnel at 160–250°C
Choosing tray baking equipment starts with output, not catalog claims. At 160–200°C, convection ovens suit small batches, cafés, and products needing even airflow. They heat quickly, but fan speed can dry thin pastries. I have seen operators solve this with lower airflow and one extra minute of baking. It is not always elegant.
Rack ovens fit changing tray loads and medium production. Their steam control helps bread, laminated dough, and products with sensitive crusts. At 180–220°C, a rack system also reduces handling between batches. However, uneven loading can create pale corners and darker center trays. That mistake is easy to overlook.
Tunnel ovens make sense when one product runs continuously at stable volume. They can operate around 200–250°C, with separate heat zones for spring, drying, and browning. The European Commission’s 2019 Food, Drink and Milk BAT Reference Document highlights thermal processing as a major efficiency focus. The International Energy Agency’s Energy Efficiency 2023 report states that industry consumes about 37% of global final energy, so heat recovery and insulation deserve serious attention.
Match the oven to hourly trays, not peak-day ambition. The U.S. Department of Energy’s Industrial Decarbonization Roadmap identifies process heat as a key efficiency opportunity. Measure actual dwell time, temperature recovery, rejected trays, and energy per kilogram for at least two weeks. Data can be inconvenient. That is useful.
How to Choose the Best Tray Baking Equipment in 2026?
Match Oven Type to Output: Convection, Rack, or Tunnel at 160–250°C
Typical commercial planning ranges show how oven selection changes with production volume. Convection ovens suit flexible, low-to-mid output; rack ovens support larger batch production; tunnel ovens are generally preferred for continuous, high-volume baking.
Throughput is shown in trays per hour and represents typical planning ranges. Actual output depends on tray size, product weight, loading pattern, bake time, and oven configuration.
Compare Core Specs: ±2°C Uniformity, Airflow, Steam, and 3–30 Tray Capacity
Choosing tray baking equipment in 2026 starts with measurable control, not a polished brochure. A ±2°C uniformity claim sounds excellent, but ask how it was tested. Was the oven empty, fully loaded, or measured near the door? In real production, cold corners appear. I would test twelve points with calibrated probes, using the actual tray load. Repeat the test after door openings.
Airflow matters as much as heat. Weak circulation can leave pale centers and dark edges. Excessive airflow may dry crusts before the crumb sets. ASHRAE’s Handbook guidance emphasizes balanced air distribution for consistent temperature control. Steam also needs scrutiny. Check injection timing, recovery speed, drain design, and visible condensation around the door. The U.S. Department of Energy’s Better Buildings foodservice guidance identifies cooking and ventilation as major commercial-kitchen energy loads, often approaching one-third of total use. Efficient heat recovery and tight seals deserve attention.
Tips: Match capacity to your busiest hour, not your average shift. A 3-tray unit suits smaller batches and faster changeovers. A 30-tray system needs stronger electrical supply, ventilation, floor access, and cleaning routines. Review data from the ENERGY STAR Commercial Ovens program, especially cooking and idle-energy metrics. Ask for test conditions in writing. “Up to” is not enough. I still prefer a live trial with your pans, recipes, and loading pattern. Ten minutes saved per batch may be meaningless if quality varies.
How to Choose the Best Tray Baking Equipment in 2026? - Compare Core Specs: ±2°C Uniformity, Airflow, Steam, and 3–30 Tray Capacity
Reference comparison of common commercial tray-oven configurations. Actual performance depends on loading pattern, product temperature, test method, installation, and local electrical requirements.
| Equipment Configuration | Tray Capacity | Typical Tray Format | Temperature Range | Chamber Uniformity | Airflow System | Steam Capability | Typical Connected Load | Best-Fit Application |
| Compact Countertop Oven | 3 trays | 600 × 400 mm or smaller | 30–300°C | Typically ±3–5°C | Single rear or side fan; fixed airflow | Manual water injection or small-capacity steam system | 3–6 kW | Small bakeries, cafés, test kitchens |
| Small Floor-Standing Convection Oven | 5 trays | 600 × 400 mm | 30–300°C | Typically ±2–4°C | Reversible or multi-speed fan; improved circulation | Timed injection with drain or humidity release | 6–12 kW | Pastries, cookies, bread rolls, small production runs |
| Medium Rack Convection Oven | 10 trays | 600 × 400 mm or 600 × 800 mm | 30–300°C | Around ±2–3°C when properly loaded | High-volume fan with adjustable speed and airflow control | Automatic steam injection; programmable timing | 12–24 kW | Retail production, catering, central kitchens |
| Large Rack Oven | 15 trays | 600 × 400 mm or 600 × 800 mm | 30–300°C | Around ±2°C under validated conditions | High-capacity circulation fan with controlled exhaust | Integrated steam generator or high-output injection system | 18–30 kW | Continuous bakery production and institutional kitchens |
| Heavy-Duty Rack Oven | 20 trays | 600 × 400 mm or 600 × 800 mm | 30–300°C | Around ±2°C with calibrated sensors | Balanced airflow with programmable fan stages | Automatic steam, adjustable by recipe phase | 24–36 kW | High-throughput bakeries and foodservice facilities |
| Large Industrial Rack Oven | 30 trays | 600 × 400 mm or 600 × 800 mm | 30–300°C | Target ±2°C after heat-up and validation | Variable-speed, multi-zone airflow with exhaust control | High-capacity automatic steam with programmable release | 30–60 kW | Industrial bakery lines, commissaries, large-scale catering |