7 Tips for Choosing Stainless Threaded Rod?
Choosing the right Stainless Threaded Rod is a small engineering decision with serious consequences. A bent rod, mismatched nut, or unsuitable finish can cause loosened joints, staining, and premature replacement. The selection process should examine grade, diameter, thread form, strength, corrosion exposure, and installation conditions.
Global demand provides useful context. World Stainless reported approximately 62 million tonnes of stainless steel crude production in 2024, confirming the material’s continuing industrial importance. However, high production volume does not make every stainless alloy interchangeable. ASTM F593 covers stainless steel bolts, screws, studs, and similar fasteners, while ASTM F594 addresses compatible nuts. These standards help buyers compare mechanical and chemical requirements more reliably.
J.R. Davis, editor of the ASM Specialty Handbook: Stainless Steels, describes stainless steel as “iron-base alloys containing a minimum of about 11% chromium.” That chromium creates the passive film responsible for corrosion resistance, but the protection depends on alloy grade, surface condition, and environment. Salt spray is unforgiving. Chlorides can attack poorly selected or contaminated components.
The following seven tips connect specification details with real installation risks. They consider 304 and 316 grades, thread accuracy, tensile performance, corrosion exposure, certification, and supplier quality. The advice is practical, but not perfect. Site conditions vary, and a laboratory result cannot represent every coastal plant, food-processing line, or outdoor structure. Always verify the design load and applicable standard with a qualified engineer before purchasing.
Define the Purpose and Load Requirements for the Threaded Rod
Define the purpose before selecting a stainless threaded rod. Is it joining light brackets, supporting a pipe rack, or resisting vibration? Each application creates different tension, shear, bending, and fatigue demands. Record the design load, direction, service temperature, exposure, and required working life. “Stainless” is not a load rating.
Calculate the required tensile area from the threaded section, not the full rod diameter. Include the nut, washer, engagement length, edge distance, and load-sharing between rods. ASTM F593 provides mechanical requirements for stainless steel bolts, screws, studs, and threaded rod materials. Its requirements help verify material performance, but they do not replace an engineered connection design. A tidy calculation can still be wrong if installation torque or uneven loading is ignored. Measure twice.
Environmental purpose matters as much as structural purpose. The NACE IMPACT study estimated global corrosion costs at 2.5 trillion dollars annually, equal to about 3.4% of global GDP. That figure supports careful alloy selection in wet, coastal, chemical, or high-temperature locations. Check chloride exposure, crevice conditions, and galvanic contact with dissimilar metals. A higher-strength rod may appear efficient, yet corrosion can reduce its useful section over time. Specify inspection access and replacement expectations. Test a sample assembly when field conditions remain uncertain.
7 Tips for Choosing Stainless Threaded Rod: Define Purpose and Load Requirements
The chart compares the estimated tensile force of common UNC threaded sizes using their tensile stress areas at 125 ksi. This value represents the minimum tensile strength commonly specified for ASTM A193 Grade B7 rod, not a recommended working load. Select the rod diameter, material, thread type, and safety factor according to the actual application, loading direction, corrosion exposure, and applicable engineering standards.
Choose the Right Stainless Steel Grade for the Environment
Choosing the right stainless steel grade starts with the environment, not the thread size. A rod exposed to dry indoor air may perform well in 304 stainless steel. Coastal air, road salt, and cleaning chemicals demand more caution. Chloride is the troublemaker. It can trigger pitting in small, hidden areas.
Use seven checks: moisture, salt exposure, temperature, chemicals, crevices, load, and maintenance access. ISO 9223 classifies atmospheric corrosivity from C1 to CX, helping engineers compare service conditions. For marine or deicing-salt exposure, 316 stainless steel usually offers better resistance because molybdenum improves chloride protection. It is not immune. Poor drainage can still defeat a good grade.
3.4% NACE’s IMPACT study estimated that corrosion costs about 3.4% of global GDP. Grade selection therefore deserves more than a catalog shortcut. ASTM A193 and ASTM A276 provide useful requirements for stainless fasteners and bar products, but the exact specification must match the application. Check the rod’s chemistry, strength, thread quality, and certification. Ask for heat and material test records. Real projects often reveal an uncomfortable mistake: the surrounding nut or washer is weaker than the rod. Also inspect cut ends, damaged threads, and stagnant water during installation. Sometimes, 316 is selected too quickly. A qualified engineer should review chemical concentration, operating temperature, and expected service life before approval.
Match Rod Diameter, Thread Size, and Thread Length
Choosing a stainless threaded rod starts with matching the rod diameter to the real load. A larger diameter may improve strength, but it can also create fit problems. Measure the existing hole, nut, washer, and joining parts before ordering. Do not rely on appearance alone. A caliper gives better evidence.
Tip: Confirm the thread size and pitch together. A rod may look correct but still fail to fit its nut. Compare the thread pitch with a gauge or a known matching nut. Check whether the thread is coarse or fine. Mixing them can damage threads quickly. I have found that hand-tightening first reveals mistakes earlier than using a wrench.
Tip: Measure the required thread length, not just the total rod length. Allow space for washers, nuts, spacers, and full thread engagement. For a connection exposed to vibration, extra engagement is usually sensible. Yet excessive length can interfere with nearby parts. Leave a small clearance. It matters.
Stainless steel offers useful corrosion resistance, but it is not maintenance-free. Dirt, salt deposits, and contact with incompatible metals can still cause problems. Clean the threads before assembly and use suitable installation practices recommended for the application. If the rod will carry structural loads, verify the grade, diameter, and load calculation with a qualified engineer. A visual check is helpful, but it is not proof. Recheck your measurements before cutting, because a short rod cannot be repaired easily.
Check Thread Quality, Tolerance, and Surface Finish
7 Tips for Choosing Stainless Threaded Rod
Check Thread Quality, Tolerance, and Surface Finish
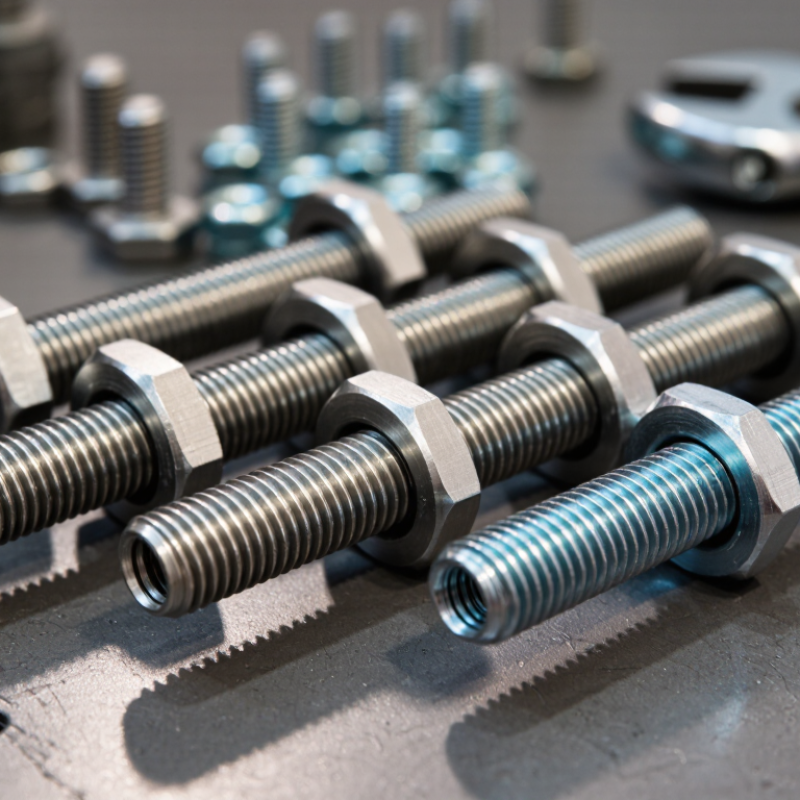
A stainless threaded rod should feel consistent from end to end. Examine the thread crest, root, and flank under bright light. Clean, sharp profiles usually indicate controlled forming or machining. Watch for torn metal, flattened peaks, dents, and cross-threaded areas. Even small defects can create difficult assembly and uneven clamping.
Use a matching nut or calibrated thread gauge during inspection. The nut should engage smoothly by hand, without binding or excessive looseness. Check the thread diameter, pitch, and length against the drawing or purchase specification. Tolerance matters because a rod can look correct yet fail during assembly. Request material certificates and inspection records when the application carries significant loads. A basic visual check is useful, but it is not enough.
Surface finish also affects installation and service life. Look for a clean, uniform surface without deep scratches, rust marks, oil residue, or embedded particles. Rough areas may damage nuts or collect contaminants. A polished finish is not always necessary; the required finish depends on the environment and assembly method. Be careful with assumptions. Shiny stainless steel is not automatically better stainless steel. Storage conditions matter too, because contact with carbon-steel dust can leave misleading stains. In practice, inspectors sometimes focus heavily on appearance and overlook thread fit. That is an easy mistake to repeat. Record sample measurements, gauge results, and visible defects before approving the rod.
Verify Standards, Certification, and Supplier Reliability
7 Tips for Choosing Stainless Threaded Rod
Verify the required standard before comparing prices. Stainless threaded rod may follow ASTM F593, ISO 3506-1, or a project-specific specification. These standards address different material grades, strength levels, and testing requirements. A polished surface proves little. Ask for the heat number, grade, diameter tolerance, thread specification, and mechanical test results.
Certification must be traceable. Request an EN 10204 3.1 material certificate, then match its heat number with the rod’s label and packing record. The ISO Survey 2023 reported more than one million ISO 9001 certificates worldwide. However, certification alone does not guarantee consistent production. Check the certificate scope, issuing body, audit date, and manufacturing location. A copied PDF is a warning sign.
Inspect supplier reliability through evidence, not confident promises. Ask for recent inspection reports, salt-spray results when relevant, and samples from the same production line. NIST guidance on supply-chain risk management stresses supplier evaluation, traceability, and documented controls. Those controls matter when rods support flanges, frames, or vibrating equipment. Confirm lead times in writing. Then test a sample for thread fit, straightness, and visible galling. I have seen “316” markings without complete records. It happens. Recheck critical orders, especially when the quotation looks unusually cheap.