Top 10 Types of High Carbon Steel Coil for Global Buyers?

Choosing the right High Carbon Steel Coil requires more than comparing carbon percentages or purchase prices. Global buyers must examine grade, thickness, width, surface condition, hardness, and intended processing. A coil for springs needs different performance from one used for saw blades, knives, wire products, or agricultural tools. Small specification gaps can create serious problems during stamping, slitting, heat treatment, or forming.

This guide introduces the top 10 types of High Carbon Steel Coil commonly considered by international buyers. It explains their typical carbon ranges, mechanical characteristics, applications, and purchasing considerations. Examples include spring steel coil, tool steel coil, bearing steel coil, and high-carbon strip steel. Each type responds differently to cutting, welding, bending, and thermal treatment. Buyers should also verify mill test certificates, chemical composition, dimensional tolerances, surface quality, and inspection methods before confirming an order.

Details matter.

Experienced sourcing teams often request samples and review actual production records, not only catalog descriptions. Relevant standards may include ASTM, EN, JIS, or customer-specific requirements, depending on the destination market. However, classifications are not perfectly consistent between suppliers. No list is perfect. Some grades overlap in application, while local naming practices may cause confusion. Therefore, this overview should support technical discussions rather than replace professional material verification. With careful comparison, buyers can reduce avoidable defects, improve processing stability, and select a coil that fits both production needs and reliable long-term supply.
Top 10 Types of High Carbon Steel Coil for Global Buyers?

High Carbon Steel Coil: Definition, Grades, and Key Properties

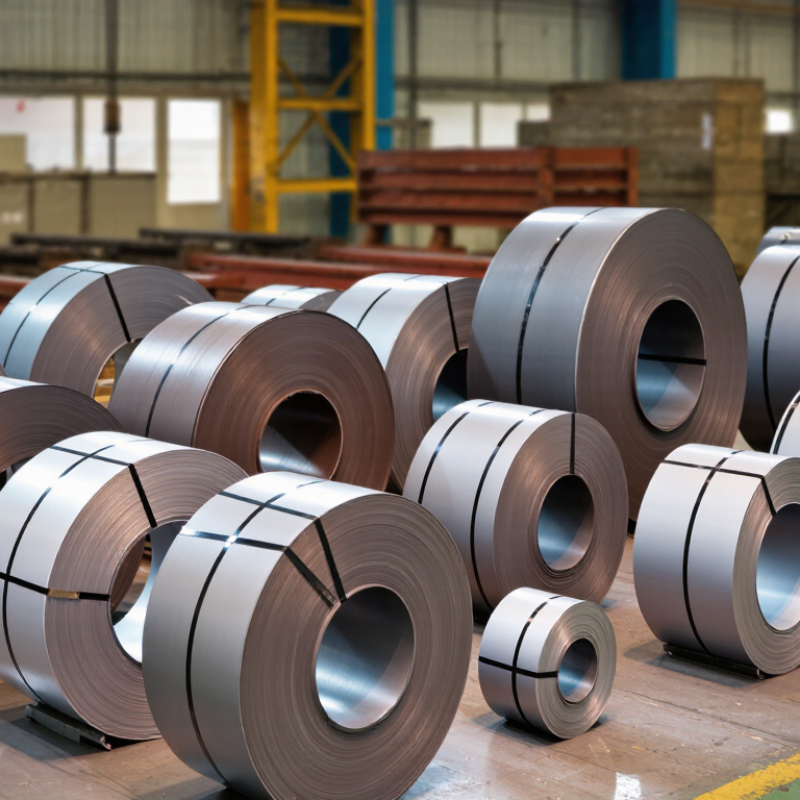
High carbon steel coil is flat-rolled steel containing roughly 0.60% to 1.00% carbon. Its carbon level creates high hardness, strength, and wear resistance after heat treatment. The coil arrives wound, like a heavy steel ribbon, and can be slit into narrower strips. Common grades include C55, C60, C65, C70, C75, C80, C85, C90, and C100. Exact grade names vary by international standard.

C55 and C60 often suit springs, blades, and forming parts requiring balanced strength. C65 to C75 provide greater elasticity and wear resistance for demanding spring applications.

C80, C85, C90, and C100 can reach higher hardness, but they usually offer less ductility. They are used for cutting tools, wear plates, and industrial components. Hardness depends on more than carbon content. Quenching, tempering, cooling speed, and strip thickness also change performance.

The coil surface should be checked for scale, rust marks, edge cracks, and uneven winding. A clean surface matters during stamping and heat treatment. Buyers should compare the mill certificate with chemical analysis, tensile results, hardness data, and dimensional tolerances. A simple grade label is never enough.

This is where buyers can misjudge. In practical sourcing, machinability and forming behavior may differ between coils with the same nominal grade. Testing a small batch before full production is sensible, although it can slow purchasing decisions. Supplier claims should remain secondary to traceable inspection records and agreed standards.

The Ten Main Types of High Carbon Steel Coil for Global Buyers

The ten main types of high carbon steel coil differ by carbon content, hardness, and end use. World Steel Association data reports 1,892 million tonnes of crude steel production in 2023. Yet, high carbon coil remains a specialized purchasing category. Carbon levels commonly range from about 0.60% to 1.00%, although specifications vary by standard and mill.

C60 coil suits stamped parts requiring moderate strength. C65 offers higher wear resistance for industrial components. C70 is common in blades and resilient strips. C75S supports spring applications after heat treatment. C80 provides a useful balance between hardness and formability. C85 is selected for tougher spring products. C90 delivers greater hardness, but bending becomes less forgiving. C100 is used for cutting edges and wear parts. C105 serves demanding spring and blade applications. C110 provides very high carbon content for specialized hardened components.

ASTM A684/A684M and EN 10132 are useful references for cold-rolled high-carbon strip procurement. Buyers should verify carbon range, coil width, thickness tolerance, surface condition, and spheroidized annealing requirements. Hardness data alone can mislead. A coil may pass hardness checks but crack during forming. That mistake happens more often than specifications suggest. My practical view is simple: compare chemistry, heat-treatment history, and trial-bend results together. Regional grade equivalents are not always exact. A mill certificate deserves careful review, not automatic trust.

Top 10 Types of High Carbon Steel Coil for Global Buyers

Typical carbon-content comparison for widely specified high-carbon and spring-steel coil grades. Values show the midpoint of the published grade range; actual limits may vary slightly by standard and product specification.

Procurement note: Carbon content strongly affects hardness, strength, weldability, and heat-treatment response. Buyers should also verify thickness tolerance, surface condition, delivery state, and the applicable national standard.

How Carbon Content and Heat Treatment Affect Coil Performance

High carbon steel coil usually contains about 0.60% to 1.00% carbon, though some grades exceed this range. That small percentage strongly changes hardness, strength, and formability. A coil for blades needs different performance from one used for springs, saw bands, wires, or wear-resistant parts. More carbon can improve edge retention and tensile strength. It can also reduce ductility and increase cracking risk during forming.

Heat treatment controls how that carbon behaves inside the steel. Annealing softens the coil and improves cutting, stamping, and cold forming. Spheroidizing creates a more workable structure for demanding machining operations. Quenching raises hardness rapidly, but uneven cooling may cause distortion or internal stress. Tempering after quenching reduces brittleness and makes the coil more dependable in service. Small temperature differences matter. A furnace error can change hardness across the coil width.

In practical purchasing, buyers should review carbon content, hardness range, tensile strength, and treatment records together. Surface scale, edge condition, and coil shape also reveal process quality. A coil may meet its chemistry standard yet perform poorly after stamping. That is a useful warning. Test samples should match the customer’s actual forming, cutting, or heat-treatment route. Harder is not always better. Storage conditions matter too, because moisture can mark untreated surfaces before fabrication begins.

Top 10 Types of High Carbon Steel Coil for Global Buyers? – How Carbon Content and Heat Treatment Affect Coil Performance

No. Steel Grade / Type Typical Carbon Content
(wt. %)
Typical Alloying Features Common Coil Thickness
(mm)
Typical Heat Treatment Indicative Hardened & Tempered Hardness Performance Characteristics Typical Applications
1 C60 / SAE 1060 0.55–0.65 Plain carbon steel; manganese typically about 0.60–0.90% 0.30–6.00 Austenitize, oil or water quench, then temper; spheroidize annealing may be used before cold forming. Approximately 35–50 HRC, depending on section size and tempering temperature Good balance of strength, wear resistance, toughness, and formability compared with higher-carbon grades. Clips, washers, agricultural components, wear strips, and moderately loaded springs
2 C67 / SAE 1065–1070 0.60–0.70 Plain carbon spring steel with moderate manganese content 0.20–4.00 Oil quenching followed by tempering; austempering is possible for selected strip sizes. Approximately 42–52 HRC Higher elastic strength and fatigue resistance than C60, with useful springback control. Flat springs, clips, retaining rings, blades, and general-purpose spring components
3 C75 / SAE 1075 0.70–0.80 Plain carbon steel; typically supplied with manganese around 0.50–0.80% 0.15–3.00 Quench and temper for spring properties; spheroidized condition improves machinability and cold forming. Approximately 45–55 HRC High tensile strength, good wear resistance, and strong elastic recovery after tempering. Saw blades, spring washers, agricultural blades, knives, and stamped spring parts
4 C80 / SAE 1080 0.75–0.85 Plain carbon steel with relatively high manganese for hardenability 0.15–3.00 Oil quench and temper; controlled heating is important to reduce distortion and decarburization. Approximately 48–58 HRC High hardness and wear resistance with good spring performance; toughness decreases if over-hardened. Industrial blades, saw components, high-load springs, scrapers, and wear-resistant parts
5 C85 / SAE 1084 0.80–0.90 Plain carbon steel; high carbon level supports high as-quenched hardness 0.15–2.50 Quench and temper; spheroidize annealing is commonly used before demanding cold-work operations. Approximately 50–60 HRC Very good edge retention and wear resistance, but limited weldability and lower impact toughness. Cutting blades, spring strips, wear plates, scrapers, and precision stamped components
6 C90 / SAE 1090 0.85–0.95 Plain high-carbon steel; manganese improves hardenability to a limited extent 0.15–2.00 Oil quench and temper, often with a lower tempering temperature when high hardness is required. Approximately 52–61 HRC Excellent wear resistance and high strength; greater risk of cracking and distortion during quenching. Knife components, industrial cutters, high-strength springs, and wear-resistant strips
7 C100 / SAE 1095 0.90–1.03 Very high-carbon plain steel; manganese commonly about 0.30–0.50% 0.10–2.00 Carefully controlled austenitizing, oil quench, and tempering; subcritical annealing may be used for forming. Approximately 55–64 HRC Very high hardness, strength, and edge retention; relatively low toughness and poor weldability. High-performance blades, fine springs, wear strips, scrapers, and cutting tools
8 65Mn 0.62–0.70 Manganese spring steel; manganese is typically about 0.90–1.20% 0.20–4.00 Oil quench and temper; controlled cooling and tempering help stabilize spring properties. Approximately 42–52 HRC Good strength, elasticity, fatigue resistance, and hardenability for general spring applications. Automotive leaf springs, clutch components, spring washers, saw blades, and agricultural tools
9 60Si2Mn 0.56–0.64 Silicon-manganese spring steel; silicon is commonly about 1.50–2.00% 0.30–4.00 Oil quench and temper; silicon improves elastic limit and resistance to softening during tempering. Approximately 42–52 HRC High elastic limit, strong fatigue performance, and better spring reliability under repeated loading. Heavy-duty springs, suspension components, torsion bars, and high-stress spring strips
10 75Cr1 0.70–0.80 Chromium-alloyed carbon spring steel; chromium generally improves hardenability and wear resistance. 0.20–3.00 Oil quench and temper; spheroidized annealing can improve machinability and forming behavior. Approximately 45–56 HRC Improved hardenability, wear resistance, and dimensional consistency compared with plain carbon spring steel. Industrial knives, circular saw components, spring parts, scrapers, and wear-resistant tooling

Note: Carbon ranges and hardness values are typical indicative ranges for commercial high-carbon steel products. Actual chemistry, thickness availability, coil dimensions, hardness, and heat-treatment results depend on the applicable material standard, product condition, section size, quenching medium, tempering temperature, and supplier specification.

Choosing the Right High Carbon Steel Coil for Industrial Applications

High carbon steel coil usually contains about 0.60% to 1.00% carbon. Its strength rises with carbon content, but formability and weldability decline. Common families include spring steel, piano-wire rod, tire-cord rod, saw-blade strip, bearing strip, tool strip, knife strip, scraper strip, chain steel, and wear-resistant strip.

Choosing the right coil starts with the finished part, not the catalogue name. Spring components need controlled elasticity and consistent hardness. Saw blades require clean edges, fine carbides, and low decarburization. Bearing applications demand strict cleanliness and stable spheroidized structures. ISO 16120-1:2017 provides requirements for steel wire rod, while ASTM A684 covers high-carbon steel strip. These standards help, but they do not replace a production trial.

Thickness tolerance matters. So does coil shape. A practical inspection should check surface cracks, edge tears, scale, hardness variation, and decarburized depth. The World Steel Association reported 1.892 billion tonnes of global crude steel production in 2023, showing the scale of steel supply and the need for disciplined purchasing. Yet a large supply base does not guarantee the correct grade. A perfect mill certificate can still hide poor coil handling or uneven cooling. Small details matter. Specify carbon range, annealing condition, tensile targets, surface finish, and inspection frequency before ordering. One assumption often remains weak: laboratory performance may not match stamping, slitting, or heat treatment on the factory floor.

Global Purchasing Factors: Standards, Quality, Pricing, and Supply

High carbon steel coil usually contains about 0.60% to 1.00% carbon. Common purchasing grades include SAE 1070, 1080, 1095, C67, C75, and bearing-quality grades. Each supports different uses, from saw blades and springs to wear-resistant components. Grade names are not interchangeable.

Standards must match the buyer’s destination and processing route. ASTM A684 covers cold-rolled carbon steel strip, while EN 10132 addresses narrow strip for heat treatment. Ask for chemistry, hardness, tensile strength, decarburization depth, surface condition, and coil shape. Mill test certificates should identify heat numbers and testing methods. ISO 9001 registration helps, but it does not replace independent inspection. That distinction matters.

Quality is only half the decision. The World Steel Association reported about 1.89 billion tonnes of crude steel production in 2023, showing the scale of global supply and its uneven regional risks. OECD’s Steel Outlook 2023 also highlights persistent excess capacity and trade pressure. Buyers should compare delivered cost, not only the quoted coil price. Include freight, duty, slitting, insurance, inspection, and payment terms. A cheaper coil may create higher rejection costs. Small details matter.

Pricing changes with carbon content, thickness, temper, surface finish, and order volume. Confirm tolerances before negotiating. Do not rely on a sample alone. A useful audit includes coil weight checks, hardness mapping, and packaging photographs. No checklist is perfect. Yet skipping traceability is an avoidable mistake.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.