How to Choose the Best Roller Compactor for Your Needs?
Choosing the right Roller Compactor starts with the material, not the machine’s appearance. Soil, asphalt, and granular fill respond differently to compaction. A unit that performs well on a road project may be poorly suited to a narrow trench or a small landscaping site. The details matter: working width, drum type, operating weight, vibration settings, and available access all affect daily performance. Small choices. Real consequences.
This guide explains how to compare roller compactors against your site conditions, workload, and operating budget. It considers single-drum and double-drum designs, smooth and padfoot drums, and the role of static or vibratory compaction. It also looks at practical factors such as transport, maintenance access, operator visibility, and ground clearance. Specifications offer a useful starting point, but they cannot tell the whole story. Ask how the machine behaves on the actual material, and check whether local service support is dependable. If possible, arrange a demonstration under realistic conditions. A brochure can make any model look capable.
No machine is best for every job. Even experienced buyers can overlook a constraint, especially when project needs change. Use the sections ahead to identify priorities, compare suitable options, and weigh trade-offs before making a decision. The goal is not to choose the biggest roller. It is to choose a machine that delivers consistent compaction without adding avoidable cost or complexity.
Define the Compaction Job: ASTM D698 Uses 600 kN·m/m³; D1557 Uses 2,700 kN·m/m³
Before choosing a roller compactor, define the soil and the required laboratory standard. ASTM D698 applies a compactive effort of about 600 kN·m/m³; ASTM D1557 uses about 2,700 kN·m/m³. That is roughly 4.5 times more energy in the lab. A higher target may require a more effective field compaction plan, but it does not specify one roller type. Not by itself.
These values describe laboratory procedures, not energy a roller must deliver per cubic metre on site. Soil gradation, plasticity, moisture, and lift thickness all affect the result. Granular soils may respond well to vibration, while cohesive soils can need a different combination of force and kneading action. Check the soil report and trial section before settling on machine weight, vibration settings, or pass count.
A practical trial can reveal what the test number alone cannot. Record moisture, lift depth, roller speed, and passes, then compare field density with the project requirement. If the surface looks firm but density remains low, the layer may be too thick or too dry. More passes are not always the answer. It is easy to focus on the 600-versus-2,700 difference and overlook moisture control; that assumption deserves a second look.
Match Roller Type to Soil: Smooth Drums for Granular Soil, Padfoot for Cohesive Soil
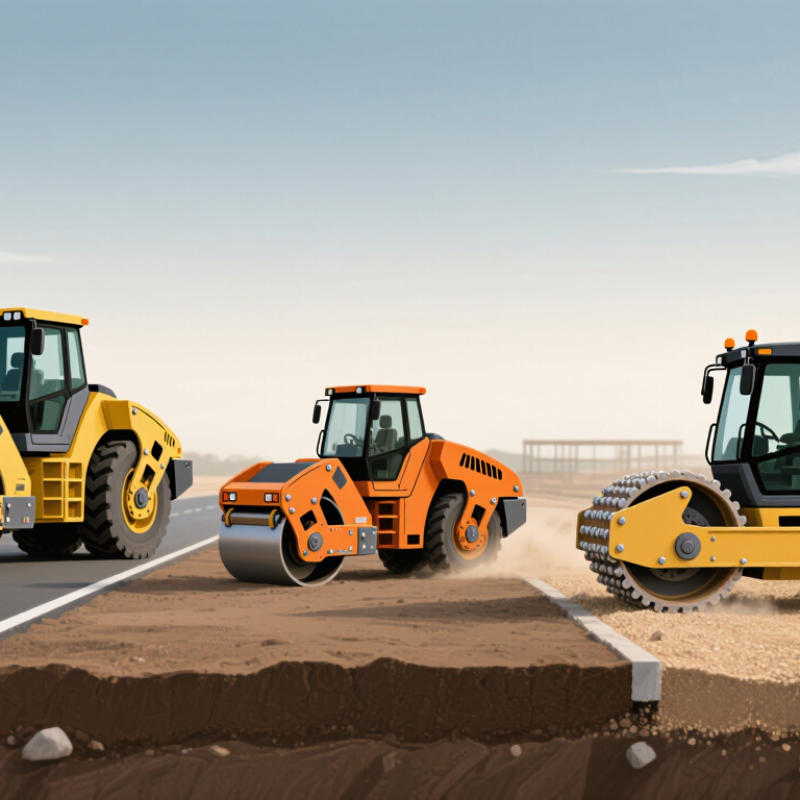
Choosing a roller starts with the soil, not the machine’s size. Smooth drums work well on granular materials such as sand and crushed stone. Their broad steel surface presses particles together and helps create a firm, even finish. Watch the surface after each pass. If stones shift or the drum leaves loose ridges, the lift may be too thick or poorly graded. A few test passes can show whether the material is tightening evenly.
Cohesive soil, such as clay or silty clay, usually responds better to a padfoot drum. Its feet knead the soil, helping break down lumps and compact deeper layers. Look for consistent foot impressions, not a surface that stays slick or pumps under the roller. Moisture matters: clay that is too wet may deform, while very dry clay can resist compaction. The rule is useful, not perfect. Soil changes across a site, and mixed ground may need a different approach. Check the material at the working depth, adjust lift thickness, and verify density with an appropriate field test rather than relying only on drum marks. A shiny surface can mislead.
How to Choose a Roller Compactor: Match the Drum to the Soil
How to read this guide: Ratings are qualitative recommendations on a 1–5 scale, not measured performance data. Smooth drums are generally suited to granular soils such as sand and gravel, while padfoot rollers are generally suited to cohesive soils such as clay. Moisture, soil gradation, and lift thickness can affect equipment choice.
Compare Operating Weight, Drum Width, Amplitude, and Frequency
How to Choose the Best Roller Compactor for Your Needs?
Choosing a roller compactor starts with the material, layer thickness, and ground conditions. Operating weight affects pressure, traction, and stability during each pass. A heavier machine can compact dense soil effectively, but it may leave marks on soft surfaces. I have found that weight alone rarely predicts performance. Balance matters more.
Drum width determines coverage and maneuverability. A wide drum suits open roadwork and reduces the number of passes. A narrower drum performs better near curbs, trenches, and tight work areas. Amplitude controls how deeply vibration reaches the layer. High amplitude suits thicker, stubborn soil, while low amplitude protects thinner layers and fragile surfaces. Too much vibration can damage the surface instead of improving it.
Frequency describes how quickly the drum vibrates. Higher frequency often supports smooth, granular materials and faster coverage. Lower frequency may work better with cohesive soil, depending on moisture and density. Always compare frequency with travel speed. If the machine moves too quickly, vibrations may not transfer enough energy. If it moves too slowly, the surface can become overworked. I would test a short section before full production. Real soil conditions can challenge laboratory assumptions. Surface temperature, moisture, and operator control also change the final result.
Check Production Needs Against Travel Speed, Pass Count, and Compacted Lift Depth
Choosing the best roller compactor starts with the production target, not the machine’s largest specifications. Estimate the required tons per hour, then compare travel speed and working width. Higher speed can increase output, but it may reduce compaction quality. A slower pass often creates better contact and more uniform density.
Pass count must match the material, moisture level, and compacted lift depth. Thin asphalt lifts may need fewer passes, while deeper granular layers usually require more controlled coverage. Check the machine’s effective compaction depth, not only its rated force. If the lift is too deep, the surface can look finished while lower material remains loose. That mistake is expensive to correct. Field density testing should guide adjustments during production.
Tips: Record results by pass. Note speed, vibration setting, moisture, and measured density. Start with a trial section, then adjust the pattern before full production. I have found that operators often chase speed too early. A balanced target works better: steady travel, complete coverage, and enough passes for the specified lift. Conditions change during the day, so yesterday’s settings may not fit today’s material. A perfect calculation is rarely possible. Watch the surface closely. Small waves, crushing, or uneven marks can reveal excessive speed, poor overlap, or too much vibration.
How to Choose the Best Roller Compactor for Your Needs? — Compare Production Needs with Travel Speed, Pass Count, and Compacted Lift Depth | Roller Type | Typical Application | Typical Working Width | Compacting Travel Speed | Typical Passes | Typical Compacted Lift Depth | Illustrative Area Production |
| Walk-behind vibratory roller | Small repairs, paths, and confined areas | 0.6–0.8 m (2.0–2.6 ft) | 1–2 km/h (0.6–1.2 mph) | 4–8 | 100–200 mm (4–8 in), depending on material and machine | About 100 m²/h (1,100 ft²/h) |
| Single-drum vibratory roller | Granular soil, road subbase, and general earthwork | 1.2–2.2 m (3.9–7.2 ft) | 2–4 km/h (1.2–2.5 mph) | 4–8 | 150–300 mm (6–12 in), subject to soil type and compaction target | About 750 m²/h (8,100 ft²/h) |
| Tandem vibratory roller | Asphalt paving and surface finishing | 1.0–2.1 m (3.3–6.9 ft) | 3–6 km/h (1.9–3.7 mph) | 4–8 | Approximately 25–100 mm (1–4 in) per asphalt lift | About 900 m²/h (9,700 ft²/h) |
| Pneumatic-tire roller | Asphalt finishing and selected soil or aggregate work | 1.7–2.3 m (5.6–7.5 ft) | 3–6 km/h (1.9–3.7 mph) | 4–8 | For asphalt, commonly about 25–75 mm (1–3 in) per lift | About 1,000 m²/h (10,800 ft²/h) |
| Planning note: Area-production figures are illustrative estimates based on representative widths, speeds, pass counts, and approximately 75% operating efficiency. Actual output and suitable lift depth vary with material, moisture, required density, site layout, and the roller’s operating settings. Confirm performance with a field test and project specifications. |
Verify Gradeability, Transport Limits, Service Access, and Site Safety Features
How to Choose the Best Roller Compactor for Your Needs?
Gradeability is more than a maximum slope printed in a specification sheet. Compare the machine’s rated climbing ability with the steepest approach, cross-slope, and turning area on your actual site. Wet clay, loose gravel, and a loaded drum can change traction quickly. Check the operator manual for operating limits; never treat a brief test run as proof of safe performance. A spec sheet can still mislead.
Confirm travel height, width, and total loaded weight, including attachments and the trailer setup. Measure the route, not just the machine. Low branches, narrow gates, tight turns, bridge limits, and soft shoulders can disrupt delivery. Ask the carrier to verify dimensions and axle loads before dispatch. Inspect whether filters, drain points, the battery, and daily check locations are reachable without awkward climbing. Clear access supports consistent inspections, though a quick walkaround can miss faults. Check rollover protection, seat belts, visibility, lights, reversing alerts, and emergency controls. Match these features to pedestrian routes and blind spots; alarms do not replace clear separation. Small details matter. Ground conditions change during a shift, so reassess after rain or fresh grading; no checklist catches every soft patch.





