How to Choose the Right HJT Wet Carrier for Solar Cells?
Choosing the right Hjt Wet Carrier is a practical process decision, not a minor equipment detail. In heterojunction solar-cell production, wafers move through wet steps where support, cleanliness, and gentle handling matter. A carrier that fits the wafer format, resists the process chemistry, and drains predictably can help reduce scratches, residue, and handling variation. Small details count: wafer spacing, contact points, edge support, and how quickly liquid leaves the carrier.
The best choice depends on the full production line. Review the cleaning and etching sequence, chemical exposure, transfer method, and target throughput before comparing materials or designs. Ask suppliers for compatibility data and trial the carrier with representative wafers. Watch for sticking, uneven drying, and marks near wafer edges. A short trial may reveal issues that a specification sheet misses. Not every line behaves alike.
This introduction cannot responsibly attribute a direct quotation to a named HJT wet-carrier expert because no source or interview was provided. A useful selection principle is: “Choose for the process your wafers actually experience, not only for the carrier’s listed material.” Treat that as guidance, not a verified expert quotation. Real production results should confirm it. Even a carefully selected carrier may need adjustment as recipes, wafer dimensions, or transfer equipment change. That uncertainty is worth acknowledging; reliable selection comes from documented trials, clear supplier evidence, and ongoing inspection.
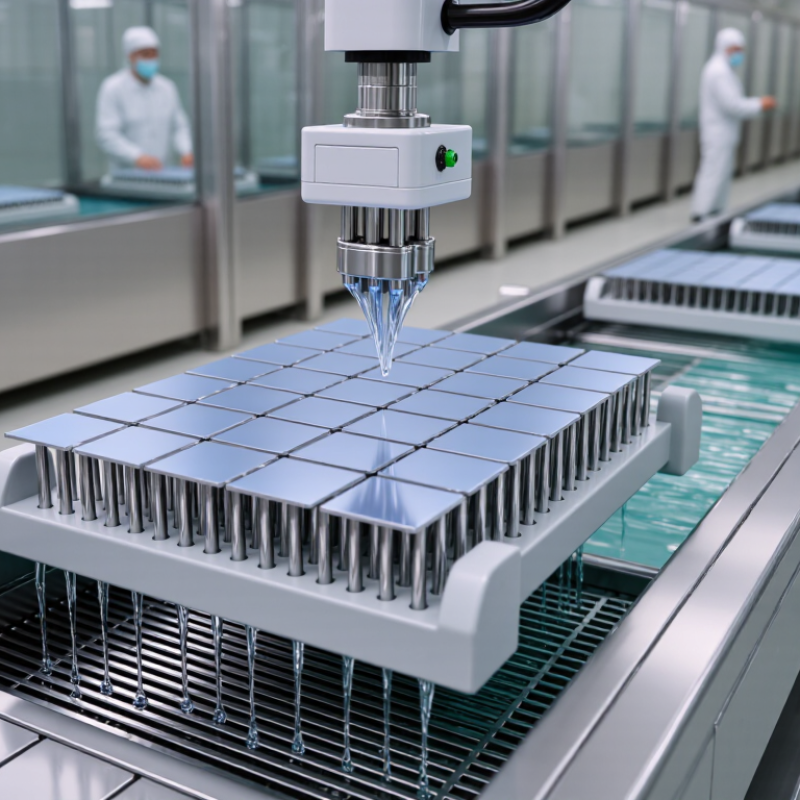
Identify the Handling Needs of HJT Solar Cells
HJT cells need careful support
Heterojunction solar cells combine thin silicon wafers with delicate surface layers. Their handling needs differ from those of sturdier cell types. A wet carrier should support each wafer evenly while allowing process liquid to reach both surfaces. Look closely at contact points: narrow rails or rough edges may create stress marks, especially during loading and unloading. Small details matter.
Consider the full wet-process route, not just the carrier’s fit in one tank. Check wafer dimensions, spacing, orientation, and how securely cells remain in place as the carrier moves. Uneven flow can leave residue or create inconsistent surface treatment. Too much restraint can also increase breakage risk. That balance is not always obvious; test representative wafers under actual process conditions. Watch for edge chips, slippage, trapped bubbles, and liquid that drains slowly. Record results across repeated runs, since one successful batch may not reveal a recurring handling problem. A carrier that is easy to clean and inspect can make these checks more reliable.
Assess Carrier Compatibility with Cell Materials and Processes
How to Choose the Right HJT Wet Carrier for Solar Cells?
Assess Carrier Compatibility with Cell Materials and Processes
A wet carrier must suit the full HJT process, not just one rinse station. Check its material against the actual cleaning solutions, rinse water, and process temperatures. Some polymers tolerate one chemistry but swell or shed particles after repeated exposure. That risk matters near sensitive silicon surfaces. Small residues can become large yield problems.
Fit matters just as much. Support points should hold thin wafers steadily without excessive contact or edge pressure. Look for smooth surfaces, consistent slots, and drainage paths that do not trap liquid. A carrier that fits a dry wafer may behave differently when wet. Test it with representative wafers and the intended loading method. Watch for movement, sticking, and chipped edges.
Run compatibility checks across repeated cycles, not just a single trial. Measure dimensions, inspect for wear, and review particle results after cleaning. Also confirm that the carrier works with robotic handling and the line’s rinse and drying steps. A clean-looking carrier can still leave residues. It is easy to overvalue a perfect fit on paper; real process conditions may expose a flaw. That deserves a second look.
Compare Carrier Design, Capacity, and Cell Protection
Choosing an HJT wet carrier means balancing cell protection with practical throughput. The carrier should support thin wafers securely without pressing hard on their surfaces. Smooth, well-finished contact points can help limit scratches and edge damage during loading and transfer. Openings between supports also matter. They allow process liquids to reach the wafer evenly and drain without lingering in narrow pockets.
Capacity is not simply a matter of fitting more cells into each carrier. Tighter spacing may increase output per batch, but it can restrict liquid flow, complicate rinsing, and make manual handling less forgiving. Check whether operators can load wafers without touching active surfaces, and whether the carrier remains stable as it moves through wet stations. A simple trial with actual wafers can reveal awkward contact points that drawings may miss. Small details matter.
Material choice deserves equal attention. Confirm compatibility with the process chemistry, temperature, and cleaning routine, rather than relying on appearance alone. A carrier that resists corrosion but flexes under load may still expose cells to risk. It is easy to focus on capacity and overlook drainage or wear. That is not always obvious at first. Inspect carriers regularly for residue, rough edges, and loosened supports, then adjust the design based on observed breakage and handling patterns.
Check Cleanliness, Chemical Resistance, and Thermal Stability
A wet carrier in an HJT line must hold wafers securely without adding contamination. Check every surface that touches a wafer, including slots, edges, and joints. Look for trapped residue after a rinse cycle. Small deposits can leave spots or create uneven wetting. Cleanliness is not just about appearance. Ask how the carrier is cleaned, dried, and inspected between runs.
Chemical resistance depends on the actual process recipe. Compare the carrier material with the acids, alkaline solutions, and rinsing agents used on site. Do not rely on a broad claim such as “chemical resistant.” Check exposure limits, concentration, temperature, and contact time. Seals and fittings matter too; they may age sooner than the carrier body. A brief compatibility test under controlled conditions can reveal swelling, discoloration, or surface changes. It takes time, but guessing is worse.
Thermal stability matters during drying and repeated process cycles. Confirm the carrier stays flat and keeps its slot spacing at the line’s operating temperatures. Even slight warping may affect wafer support or handling. Ask for dimensional data across the expected temperature range, then compare it with your process needs. A carrier that works at room temperature may behave differently after repeated heating. No specification replaces a real process check. Record changes after use, including chips or dull patches, and revisit the choice when the recipe changes.
How to Choose the Right HJT Wet Carrier for Solar Cells?
Typical continuous-use temperature limits vary by material and grade. Use this comparison as a screening guide, then confirm cleanliness, chemical compatibility, and operating limits with the material supplier.
Typical reference values: polypropylene about 100°C, PVDF about 140°C, PFA about 260°C, and fused quartz about 1,000°C. Actual limits depend on grade, load, exposure time, and process conditions.
Validate Carrier Performance in the Production Line
A carrier that performs well on a sample bench may behave differently during continuous HJT production. Validate it on the actual wet-process line, using the same wafers, chemistry, and operating settings planned for routine runs. Small differences matter. Track wafer breakage, edge chips, slipping, and visible residue across repeated loads, not just one successful pass.
Watch the carrier through each transfer and rinse. Does liquid drain evenly, or collect in corners? Check whether wafers remain seated when the carrier accelerates or changes direction.
Record loading time, unloading time, and any line stoppages. These details connect carrier design with real throughput. They also help distinguish a carrier issue from changes in process conditions.
Compare measurements before and after exposure to the production chemistry. Inspect contact surfaces for wear, deposits, discoloration, or deformation, and review particle data where available. Use a documented acceptance range and repeat the test after cleaning; cleaning can change surface behavior. Results may not be perfectly tidy. That is useful. If one position in the carrier shows more defects, investigate alignment, flow, and handling before approving a full-scale deployment. A short trial can miss slow wear, so include enough production cycles to reflect normal use.





