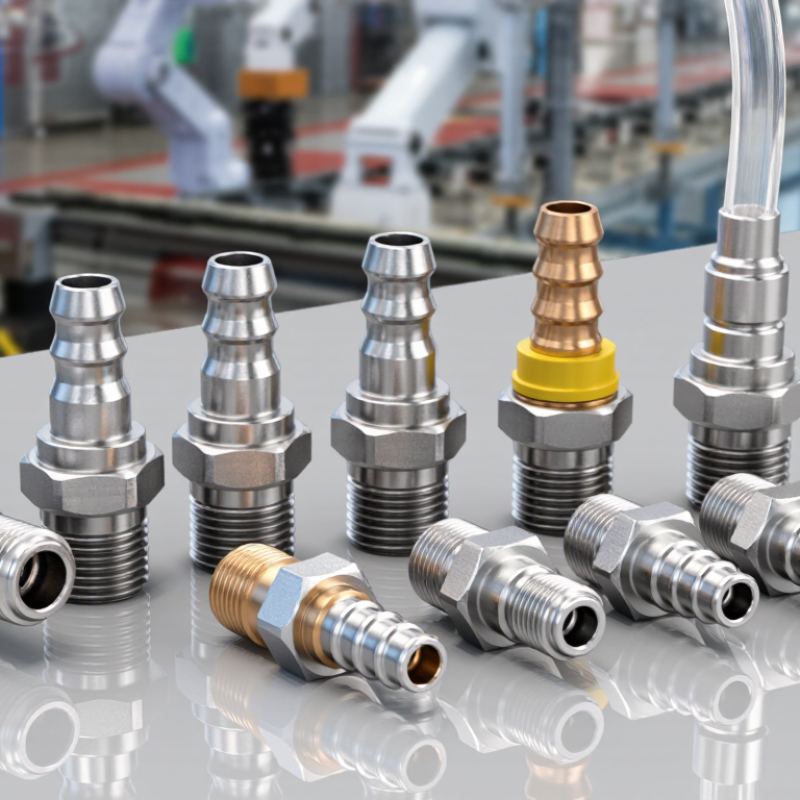
Global buyers are paying closer attention to Air Tube Fittings as factories demand cleaner, faster, and more reliable pneumatic systems. The choice affects every connection, from a compact robot gripper to a long production line carrying compressed air. A poorly selected fitting may create a barely visible leak, reduce pressure, and increase compressor workload.
Grand View Research identifies industrial automation as a major driver of the global pneumatic equipment market. MarketsandMarkets also reports continuing demand for pneumatic components across manufacturing, packaging, automotive, and process industries. These reports do not measure Air Tube Fittings separately in every region. That limitation matters. Market figures can look precise, while actual fitting demand varies with plant upgrades, maintenance cycles, and local standards.
Small component. Large consequences.
Dr. Peter Beater, author of Pneumatic Drives: System Design, Modelling and Control, wrote, “Pneumatics is a technology with a future.” His observation remains relevant, but modern buyers should examine more than catalogue price. Material compatibility, tube size, working pressure, temperature range, thread accuracy, sealing method, and documented quality controls all deserve attention. ISO 4414 guidance is especially useful when evaluating pneumatic safety and system design.
Leading manufacturers increasingly support traceability, corrosion-resistant materials, push-to-connect designs, and consistent dimensional tolerances. Yet no supplier is perfect. Product availability, technical support, and regional certification can still differ widely. This guide compares top Air Tube Fittings manufacturers for global buyers, using practical purchasing criteria and available industry evidence. It also acknowledges an uncomfortable truth: the cheapest fitting may become the most expensive part after months of unnoticed leakage.
Top Air Tube Fittings Manufacturers for Global Buyers
Air Tube Fittings: Functions, Types, and Industrial Applications
Air tube fittings connect pneumatic lines while controlling airflow, pressure, and installation direction. They create sealed paths between tubing, valves, cylinders, and filters. Push-to-connect fittings support rapid assembly and maintenance. Compression fittings suit rigid tubing and demanding vibration conditions. Threaded, elbow, tee, bulkhead, and reducer designs solve different routing problems.
Material selection depends on pressure, temperature, moisture, and chemical exposure. Nickel-plated brass offers strength in general industrial systems. Stainless steel performs better in corrosive or hygienic environments. Polymer fittings reduce weight and may support clean automation areas. Always check tube outside diameter, thread standard, working pressure, and seal compatibility. A small mismatch can cause slow leakage.
According to MarketsandMarkets’ 2024 Pneumatic Equipment Market report, the sector is forecast to grow at about 6.9% annually between 2023 and 2028. This growth reflects wider automation adoption in packaging, assembly, material handling, and process equipment. A 2024 report from the International Federation of Robotics also recorded more than 500,000 industrial robots installed globally in 2023, increasing demand for compact pneumatic connections. In factories, fittings appear beside grippers, pick-and-place units, conveyor stops, and robotic tooling. Field experience shows that accessibility matters as much as pressure rating. A perfect fitting on paper may still be difficult to service. That detail deserves more attention.
The chart presents common metric outside diameters used with pneumatic push-in air tube fittings. Sizes such as 4 mm, 6 mm, 8 mm, 10 mm, and 12 mm are widely used in factory automation, robotics, packaging machinery, instrumentation, and general compressed-air systems. Fitting selection should also consider tube material, working pressure, temperature, thread standard, sealing method, and ISO 14743-compatible connection requirements.
Top Air Tube Fittings Manufacturers for Global Buyers
Key Standards for Evaluating Global Air Tube Fitting Manufacturers
Selecting an air tube fitting manufacturer requires more than comparing prices. Start with documented compliance to ISO 4414 and ISO 14743, where applicable. These standards help assess pneumatic safety, tube compatibility, and fitting performance. Confirm thread specifications, including ISO 7-1 or ISO 228 requirements, before approving samples. A small thread mismatch can cause leakage during installation.
Request pressure, temperature, and leak-test reports for each fitting series. Reliable manufacturers should explain test methods, sample sizes, and acceptance limits. Check material certificates for brass, stainless steel, polymers, and sealing components. Traceable batch numbers make quality issues easier to investigate. Factory audits can reveal calibration practices, storage conditions, and operator training. A polished catalog is not proof of stable production.
Tips: Compare samples from three production batches. Test them under realistic pressure cycles. Ask for certificates, not verbal assurances. Confirm packaging protects threads and sealing surfaces during long-distance transport. Also review response times, engineering support, and replacement procedures. These details often matter more than a slightly lower quotation. Some evaluations remain imperfect because test conditions differ between factories. Record every assumption, then challenge it before final approval.
Choosing air tube fittings manufacturers requires more than comparing catalog prices. Product strength often reveals the real difference. Manufacturers specializing in push-to-connect fittings usually offer fast installation and clean tube release. Their products suit compact control panels and repeated maintenance work. I check tube compatibility, thread accuracy, and seal performance before approval. Small dimensional errors can create frustrating air leaks.
Compression fitting manufacturers serve buyers needing strong mechanical retention. They perform well in vibration, outdoor equipment, and heavier pneumatic assemblies. Stainless steel options provide better corrosion resistance near moisture or chemical exposure. However, material selection should match the actual environment. “Stainless” is not a complete specification.
Some manufacturers stand out through engineering support. They can develop custom elbows, bulkhead fittings, miniature connectors, or mixed-thread solutions. Their value appears in drawings, sample testing, and traceable inspection records. Pressure testing, pull-out testing, and leak testing should follow defined procedures. Clear documentation matters.
Still, no supplier is perfect. I have seen attractive samples fail after poor tube cutting. A strong manufacturer should explain installation limits, storage conditions, and replacement practices. Buyers should request production samples, dimensional reports, and independent test evidence when the application is critical. Consistent packaging also protects threads and sealing surfaces during long international shipments.
Global buyers should examine material choices before comparing prices. Brass fittings suit common pneumatic systems and offer reliable machinability. Stainless steel performs better in humid, corrosive, or outdoor environments. Engineered polymers can reduce weight, but temperature limits require careful review. Check tube compatibility, sealing performance, thread type, and working pressure together. A fitting may look suitable yet fail after repeated heat cycles.
Manufacturing quality depends on more than attractive samples. Skilled producers use controlled machining, clean deburring, dimensional inspection, and leak testing. They should provide material certificates, inspection records, and batch traceability. Consistent thread depth matters during installation. Poor finishing can damage seals or create tiny leaks. Customization may include tube diameters, thread standards, seal materials, body shapes, and special packaging. Clear technical drawings reduce misunderstandings between buyers and factories. Still, one weakness remains: a perfect prototype does not always represent mass production.
Tips: Request samples in your actual tubing and test them under realistic pressure. Ask about tolerance control, salt-spray testing, and temperature resistance. Confirm whether customization changes tooling costs or delivery times. A small trial order often reveals more than confident promises.
Global buyers selecting air tube fittings should verify suppliers, not merely compare unit prices. In my sourcing work, I begin with tube material, working pressure, temperature, media, thread standard, and expected cycles. A fitting that seals in a workshop may fail beside vibration, oil mist, or heat. The U.S. Department of Energy’s Improving Compressed Air System Performance sourcebook reports that leaks commonly waste 20% to 30% of compressor output. Small connection errors become expensive quickly. Ask for pressure-test records, dimensional drawings, material certificates, and batch traceability. Request samples from the same production line. That detail matters.
Supplier verification should combine documents with physical evidence. Check whether the factory controls incoming materials, machining, assembly, inspection, and final packing. Review calibration records and sampling plans, not only quality certificates. ISO 4414 provides safety principles for pneumatic systems, while ISO 8573-1 defines compressed-air purity classes. These standards support evaluation, but they do not prove consistent manufacturing. Independent testing can confirm leakage, pull-out strength, burst pressure, and repeated connection performance. The test method must match actual service conditions. Be cautious with claims such as “universal” or “industrial grade.” A supplier may pass one laboratory test yet struggle with inconsistent batches. I would also compare corrective-action reports and response times. Price matters, but an unexplained price gap deserves investigation.
| Fitting Category | Common Tube Compatibility | Typical Materials | Connection Method | Typical Working Pressure Range | Typical Temperature Range | Applicable Standards or References | Key Supplier Verification Points |
|---|---|---|---|---|---|---|---|
| Push-to-Connect Fittings | Polyurethane, nylon, and polyethylene tubing; common metric sizes from 4 mm to 12 mm and inch sizes from 1/8 in to 1/2 in | Nickel-plated brass, stainless steel, engineering polymer, and elastomer seals | Tube is inserted directly into an internal collet and sealed by an O-ring | Approximately 0.8–1.0 MPa for many industrial pneumatic designs; confirm by size, material, and temperature | Approximately −20°C to +80°C for common elastomer-sealed designs | ISO 14743 for push-in connectors; manufacturer test specifications | Request leakage-test results, tube-retention data, seal material details, and dimensional drawings |
| Compression Tube Fittings | Rigid metallic or polymer tubes; commonly available for 4–16 mm metric tubing and comparable inch sizes | Brass, stainless steel, aluminum, ferrules, and sealing rings | Threaded nut compresses a ferrule around the tube | Often approximately 1.0–3.0 MPa, depending on tube wall thickness, material, and fitting size | Commonly approximately −40°C to +120°C; seal selection may reduce or extend this range | ISO 8434-1 for selected metallic compression-style connections; applicable national standards | Verify pressure-rating calculations, ferrule geometry, tube-wall requirements, and repeat-assembly performance |
| Threaded Adapter Fittings | Used with pneumatic tubing, valves, cylinders, manifolds, and air preparation equipment | Brass, stainless steel, plated steel, or reinforced polymer | Male or female pipe threads, often combined with a tube connection | Typically approximately 0.7–2.0 MPa for compressed-air systems, subject to thread size and construction | Commonly approximately −20°C to +100°C | ISO 7-1 for pressure-tight pipe threads; ISO 228-1 for parallel pipe threads where applicable | Confirm thread standard, gauge inspection records, thread tolerance, sealing method, and cross-border compatibility |
| Bulkhead Fittings | Polyurethane, nylon, polyethylene, or metallic tubing; commonly 4–12 mm metric sizes | Nickel-plated brass, stainless steel, polymer body, and elastomer seals | Tube connection passes through a panel or enclosure and is secured with a retaining nut | Usually approximately 0.6–1.0 MPa in general pneumatic applications | Approximately −20°C to +80°C for common industrial versions | ISO 14743 where the tube interface is a push-in connection; panel dimensions must be supplier-specific | Check panel-hole diameter, maximum panel thickness, torque requirements, vibration resistance, and leak testing |
| Elbow and Tee Fittings | Compatible with common pneumatic tubing sizes from 4 mm to 12 mm and selected inch sizes | Brass, stainless steel, acetal, polyamide, and sealing elastomers | Push-in, compression, or threaded configurations in 90-degree and branch layouts | Commonly approximately 0.6–1.0 MPa for compact push-in designs | Approximately −20°C to +80°C for standard seal materials | ISO 14743 for applicable push-in tube connections; internal flow testing recommended | Compare flow-rate data, minimum bend radius, insertion depth, orientation strength, and dimensional consistency |
| Bulkhead Union and Straight Union Fittings | Same-size or reducing connections for nylon, polyurethane, polyethylene, and related tubing | Nickel-plated brass, polymer, stainless steel, and elastomer seals | Joins two tubes directly or connects tubes across a panel | Typically approximately 0.8–1.0 MPa for general-purpose pneumatic products | Approximately −20°C to +80°C | ISO 14743 for suitable push-in configurations | Verify tube-size accuracy, pull-out force, leak rate, body-wall thickness, and availability of replacement seals |
| Stainless Steel Pneumatic Fittings | Metallic and polymer tubing; frequently selected for corrosive, washdown, or hygienic environments | Stainless steel grades such as 304 or 316, with compatible elastomer seals | Push-in, compression, or threaded connection | Often approximately 1.0–3.0 MPa, depending on connection type and tube specification | Approximately −40°C to +150°C with suitable seals and application conditions | Material certificates, corrosion-resistance testing, and applicable ISO or ASTM methods | Request grade certificates, surface-finish data, salt-spray or corrosion-test records, and seal compatibility information |
| Miniature Pneumatic Fittings | Small tubing commonly from 2 mm to 6 mm outside diameter | Nickel-plated brass, stainless steel, polymer, and miniature elastomer seals | Miniature push-in or threaded connection | Commonly approximately 0.5–0.8 MPa, depending on bore size and body design | Approximately −10°C to +60°C for many compact assemblies | Supplier dimensional standards, ISO-based test procedures, and application-specific validation | Review minimum operating flow, dead volume, insertion depth, precision machining, and low-pressure leakage results |
| Supplier Qualification Checklist | All requested tube sizes, thread systems, and regional specifications | Material traceability for metals, polymers, coatings, and seals | Documented production, inspection, packaging, and change-control procedures | Rating must be supported by product drawings, test reports, and clearly defined operating conditions | Temperature rating must identify the seal compound, medium, pressure, and exposure duration | ISO 9001 certification, applicable product standards, RoHS or REACH declarations where required | Verify legal company records, factory audit results, sample consistency, inspection plans, complaint handling, and shipment traceability |


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.