


Buying a Palletizing Machine is not simply a matter of comparing prices. Global buyers must match equipment with products, pallets, factory space, and long-term production goals. A machine stacking sealed cartons may perform differently with bags, cases, or fragile containers. The details matter.
A practical evaluation starts with real production data. Check package dimensions, weight variation, pallet height, cycle speed, and required stacking patterns. Ask suppliers to run samples using your actual products. Watch the gripper move, not just the demonstration video. Measure changeover time. A few seconds can become several lost hours each week.
Reliability also depends on integration. Confirm communication with conveyors, wrapping systems, scanners, and warehouse software. Review guarding, emergency stops, operator access, and maintenance procedures with qualified specialists. Ask about spare parts, remote support, training, and service response times in your region. These factors often matter more than a small discount.
Supplier experience deserves careful attention. Request installation references from factories with similar workloads and climate conditions. Review documented performance, not only attractive claims. A strong supplier explains limitations clearly. That builds trust.
A spreadsheet can still lie. Electricity quality, dusty floors, uneven pallets, or changing product sizes may expose hidden weaknesses. Leave room for future growth, but avoid paying for unused capacity. A smaller robotic cell may suit one plant, while a high-speed conventional system may suit another. The right decision combines technical evidence, operator feedback, total ownership cost, and realistic expectations. These ten buying tips help global buyers ask better questions before signing a purchase agreement.
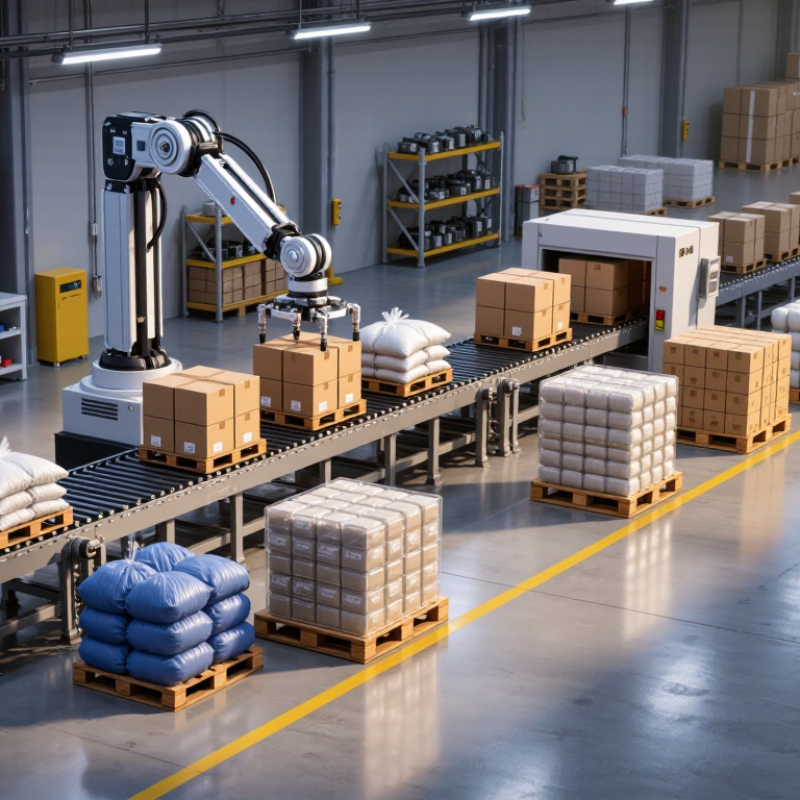
Before comparing palletizing machines, define the work they must perform every shift. Record product dimensions, case weight, packaging material, and surface friction. A small carton may slide differently from a heavy corrugated box. Measure pallet length, width, maximum height, and allowable overhang. Include damaged cartons and mixed product sizes in your assessment.
Capacity must match real production, not an ideal brochure figure. Count cases per minute during normal operation and peak periods. Note shift length, planned growth, and required changeovers. A machine handling 20 cases per minute may struggle when operators frequently switch between four patterns. Keep it practical. Floor space, ceiling height, conveyor direction, and pallet access also affect the design. Many early estimates miss these details.
Ask suppliers to test representative products and complete pallet patterns. Bring actual cartons, including weak or slightly warped samples. Check layer alignment, load stability, changeover time, noise, cleaning access, and operator controls. Safety guarding and emergency stops should fit the site’s risk assessment and applicable requirements. Maintenance access matters too; a compact machine can become difficult to service. Utility needs deserve attention, including electrical supply, compressed air, and network connections. Some decisions still involve uncertainty. Recheck assumptions after a trial run, because laboratory performance rarely matches a busy production floor.
Evaluate Machine Types, Payloads, and Packaging Compatibility
Tip 1. Match the machine type to your production pattern. Robotic arms suit varied products, while conventional palletizers often support steady, high-speed lines.
Tip 2. Measure the full payload, including the product, carton, wrapping, and gripping tool. A narrow safety margin can cause costly downtime.
Tip 3. Check reach, stacking height, and pallet dimensions together. A machine may lift the load but fail at the final layer.
Tip 4. Test packaging compatibility with real cartons, bags, trays, or pails. Surface texture matters.
Tip 5. Inspect the gripper’s contact points. Soft bags may deform, while rigid boxes can slip without proper support.
Tip 6. Ask for a practical line trial. Samples reveal problems that brochures often hide.
Tip 7. Review changeover time between package sizes. Five minutes can matter during daily production.
Tip 8. Confirm conveyor speed and product spacing before selecting machine capacity.
Tip 9. Consider local power standards, floor space, climate, and maintenance skills. Imported equipment may need different electrical protection or training.
Tip 10. Request documented payload tests, guarding details, spare-part plans, and operator instructions. Clear records improve reliability.
I once focused too heavily on maximum speed. That was a mistake. Real performance depends on stable feeding, careful programming, and consistent packaging. Leave room for future products, but avoid paying for capacity your line will never use.
Review the layout in three dimensions. Confirm aisle clearance, pallet entry direction, guarding space, maintenance access, and ceiling height. Leave room for future conveyors or inspection equipment.
A compact design may appear efficient, but crowded access can increase service time. It happens often. Compare robotic and conventional automation according to product variety, speed, and available floor space.
Integration deserves equal attention. Ask whether the machine can communicate with existing controls through suitable industrial protocols. Verify signals for line speed, pallet status, faults, recipe selection, and emergency stops. Request realistic factory acceptance testing with your products and pallet patterns.
Also examine safety documentation, operator training, spare-parts planning, and local technical support. Remote diagnostics can reduce delays, but they should not replace clear manuals or trained technicians. Utility requirements are easy to overlook, especially compressed-air quality and electrical standards across regions.
A perfect layout rarely exists; your team should record the compromises and judge their long-term cost. End users may prefer a lower initial price, yet difficult changeovers and weak integration can quietly reduce production reliability.
A reliable palletizing machine starts with a verifiable supplier, not a polished brochure. Request factory photographs, production records, and references from similar installations. Inspect weld quality, cable routing, guarding, and component traceability. Ask how each machine is tested before shipment. A documented factory acceptance test should include speed, load stability, fault recovery, and repeated pallet patterns. Numbers matter.
Safety evidence deserves careful attention. Require a documented risk assessment, emergency-stop testing, interlocked doors, light curtains, and safe access for maintenance. Confirm that the control system matches relevant machinery safety requirements, such as ISO 12100 and ISO 13849 where applicable. Do not accept “international standard” as a complete answer. Ask which standard, which market, and which certificate.
Global compliance can become expensive when checked too late. Confirm electrical drawings, operating manuals, declarations, and inspection reports in the destination language. Verify requirements for voltage, frequency, labeling, radio equipment, and local machinery certification. Compliance depends on the installation country and machine configuration. A supplier should explain these differences clearly.
I once underestimated spare-parts planning. That mistake can stop production for days. Request a recommended inventory, response times, software backup procedures, and technician training. Review the warranty exclusions line by line. A supplier may be technically capable yet weak in after-sales support. Leave room for doubt, and test every promise before signing.
10 Palletizing Machine Buying Tips for Global Buyers
A palletizing machine’s purchase price is only the visible cost. Your total ownership calculation should include grippers, guarding, conveyors, integration, software, training, energy, spare parts, and planned maintenance. Add changeover time for different carton sizes. A five-minute delay repeated across every shift can erase a promising payback.
The International Federation of Robotics reported 541,302 industrial robots installed worldwide in 2023. This shows strong automation demand, but popularity does not guarantee your return. Measure current cases per minute, labor hours, unplanned stoppages, product damage, and floor-space costs. Then model realistic performance, not the supplier’s best demonstration. A neat ROI spreadsheet can still be wrong. Include a slower ramp-up and occasional faults. Deloitte’s 2024 Smart Manufacturing survey found that 86% of manufacturers viewed smart manufacturing as an important competitiveness driver, yet implementation capability remains uneven.
Buying tip: Request a five-year total-cost worksheet with assumptions shown line by line. Ask for separate figures for installation, commissioning, operator training, annual service, and replacement parts. Require a sensitivity test at 80%, 90%, and 100% utilization.
Service support deserves equal attention. Confirm technician response times, local spare-parts stock, remote diagnostics, software update policies, and escalation procedures. Ask who repairs the machine at 2 a.m. during peak season. A low-cost machine with slow support may become expensive quickly. Test service communication before signing. That detail is often overlooked.
Practical comparison framework for evaluating palletizing equipment using a five-year total cost of ownership model. Monetary values are illustrative industry benchmarks in USD and should be replaced with supplier quotations and site-specific operating data.
| Tip | Buying Dimension | What to Verify Before Purchase | Realistic Benchmark or Target | Illustrative Cost or Benefit | Service and Risk Check | ROI Measurement |
|---|---|---|---|---|---|---|
| 1 | Match throughput to the production line | Confirm bags, cases, cartons, or trays per minute; product dimensions; pallet pattern; stacking height; and planned production growth. | 20–60 cases per minute for many conventional robotic or layer-palletizing applications, depending on payload and pattern. | Oversizing equipment by 30% may add approximately $20,000–$80,000 to the purchase price without improving current output. | Require a documented acceptance test at the agreed production rate using representative products and pallets. | Calculate annual recovered capacity: additional units per hour × operating hours × contribution margin. |
| 2 | Compare total ownership cost, not only purchase price | Request a five-year cost model including equipment, tooling, freight, installation, training, utilities, preventive maintenance, spare parts, and downtime. | Five-year operating and service costs commonly represent 25%–60% of the initial equipment investment, depending on complexity and utilization. | For a $180,000 system, a reasonable five-year ownership estimate may be $270,000–$390,000. | Separate one-time costs from recurring costs and identify which items are excluded from the quotation. | TCO per pallet = total five-year ownership cost ÷ pallets produced during five years. |
| 3 | Evaluate labor savings realistically | Count current palletizing staff, shifts, overtime, injury-related absence, supervision, and the number of employees required after automation. | A semi-automatic or robotic solution may reduce direct palletizing labor by approximately 1–3 full-time positions per shift, subject to local workflow. | At a fully burdened labor cost of $22 per hour, removing one position from two shifts may save about $91,500 per year before redeployment costs. | Confirm whether employees can be reassigned to loading, quality inspection, or material handling rather than eliminated. | Annual labor benefit = avoided labor hours × fully burdened hourly rate. |
| 4 | Check payload, reach, and pallet-pattern flexibility | Verify maximum product weight, end-of-arm tooling capacity, reach, pallet size, layer count, mixed-SKU requirements, and changeover procedure. | Allow a minimum 10%–15% payload margin above the heaviest product and confirm every required SKU during factory testing. | Additional tooling or pattern hardware may cost $5,000–$25,000 per configuration. | Ask for changeover time; a target of 15 minutes or less is useful for frequent product changes. | Measure increased line flexibility through reduced changeover minutes and higher available production hours. |
| 5 | Use realistic availability and downtime assumptions | Review guaranteed availability, mean time between failures, mean time to repair, planned maintenance hours, and jam recovery procedures. | For a properly integrated system, target technical availability of approximately 95%–98%, excluding upstream material shortages. | A 1% availability loss on a line producing 40 cases per minute for 4,000 hours annually equals about 9,600 cases of lost capacity. | Require alarm history, remote diagnostic capability, spare-parts response times, and a defined escalation process. | Downtime cost = lost production units × contribution margin per unit + recovery labor and logistics costs. |
| 6 | Assess integration and safety requirements | Confirm interfaces with conveyors, stretch wrappers, pallet dispensers, warehouse systems, barcode readers, guarding, interlocks, and emergency stops. | Budget approximately 10%–25% of machine purchase price for integration, guarding, site preparation, and commissioning. | For a $180,000 machine, integration may add approximately $18,000–$45,000. | Obtain risk assessment documentation and verify compliance with applicable local machinery, electrical, and workplace safety requirements. | Include avoided manual-handling incidents, lower rework, and reduced line interruptions in the benefit model. |
| 7 | Compare energy and consumable usage | Request connected load, average operating load, compressed-air consumption, lubricant requirements, stretch-film usage, and standby consumption. | Many electrically driven systems operate within approximately 3–15 kW average demand, excluding auxiliary equipment. | At $0.12 per kWh and 4,000 operating hours per year, a 10 kW average load costs about $4,800 annually. | Check whether air quality, pressure, filtration, and electrical supply requirements are compatible with the site. | Annual utility cost = average kW × operating hours × local electricity rate, plus compressed-air cost where applicable. |
| 8 | Verify local service and spare-parts support | Ask where technicians are located, typical response time, critical spare-parts stock, remote support hours, and training availability. | For production-critical equipment, target remote response within 4–8 hours and on-site support within 24–72 hours, depending on region. | An annual preventive-maintenance contract may cost approximately $6,000–$18,000, excluding major repairs and travel. | Define service-level agreements, parts-obsolescence notification, travel charges, labor rates, and warranty exclusions in writing. | Compare the expected annual service cost with the financial impact of one additional day of unplanned downtime. |
| 9 | Calculate installation, training, and ramp-up time | Confirm delivery terms, import duties, foundation work, factory acceptance testing, site acceptance testing, operator training, and production ramp-up. | Typical installation and commissioning may require 3–10 working days, depending on line complexity and site readiness. | Lost production during a five-day shutdown at a contribution margin of $2,000 per hour could exceed $80,000. | Use a detailed project schedule with responsibilities for utilities, drawings, permits, product samples, operators, and maintenance personnel. | Ramp-up loss = planned downtime hours × normal contribution margin per hour. |
| 10 | Set a measurable payback and ROI threshold | Model labor savings, increased throughput, quality improvement, reduced damage, lower injuries, maintenance, energy, financing, and residual value. | Many buyers target a simple payback period of approximately 2–4 years, subject to capital policy and production stability. | Example: $115,000 annual operating benefit minus $25,000 annual ownership cost equals $90,000 net annual benefit. | Use conservative, expected, and optimistic scenarios; do not base approval solely on the supplier’s best-case output claim. | Simple ROI = (annual net benefit ÷ total initial investment) × 100%; payback = initial investment ÷ annual net benefit. |


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

