


Process Water Treatment is the controlled management of water used in manufacturing, energy production, food processing, and other industrial operations. It removes unwanted substances before water enters a process, supports production, or leaves a facility. These substances may include suspended solids, oils, metals, salts, microorganisms, and chemical residues. The treatment method depends on the water source, production requirements, discharge limits, and reuse goals.
Professor Asit K. Biswas, a globally recognized water-policy expert, has said, “The biggest crisis facing humanity is the crisis of water governance, not water scarcity.” His observation applies directly to industrial water management. A factory may consume thousands of litres daily, yet poor monitoring can waste water and increase operating costs. A clear treatment plan connects filtration, clarification, membrane systems, disinfection, and regular testing. It also protects equipment. Scale inside a boiler, for example, can reduce heat transfer and create costly maintenance problems.
Small details matter. A cloudy sample can reveal a larger process failure. A rising conductivity reading may signal salt buildup or membrane damage. Experienced operators therefore review trends, not only single test results. Reliable treatment also requires calibrated instruments, documented procedures, trained staff, and independent verification when risks are high. Still, no system is perfect. Treatment chemicals can create secondary waste, and advanced equipment can demand significant energy. These limitations deserve honest attention. Understanding Process Water Treatment means balancing product quality, worker safety, environmental responsibility, water reuse, and practical operating costs. That balance is difficult. It is also essential.
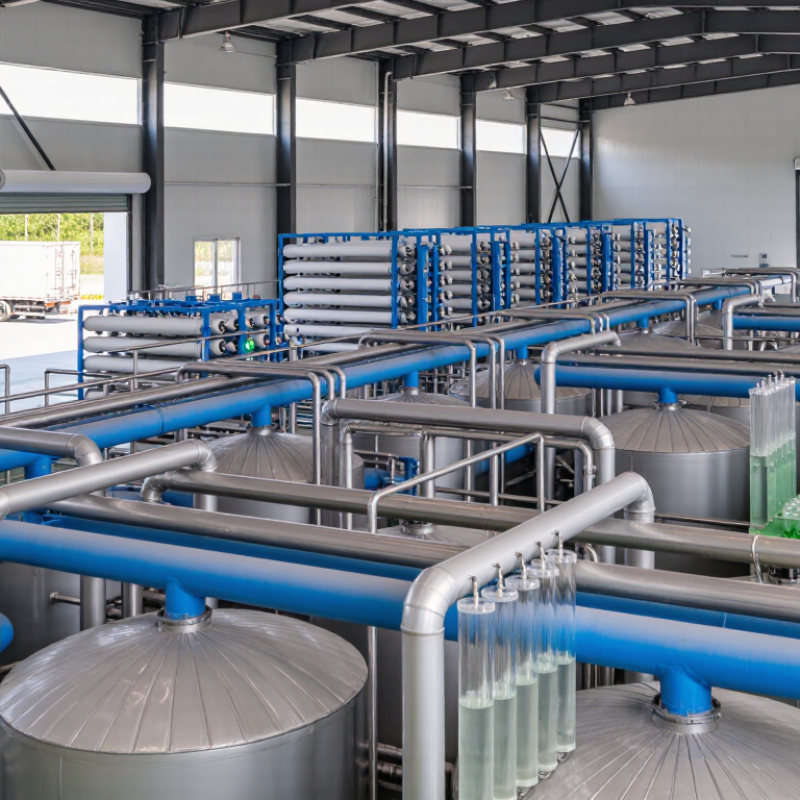
What Is Process Water Treatment?
Process water treatment is the controlled preparation of water used inside industrial operations. It supports cooling, heating, rinsing, production, and equipment protection. Unlike drinking water treatment, it begins with the process requirements. A semiconductor line may need ultra-low mineral content. A food facility may require strict microbial control. A boiler may need softened water to reduce scale.
Treatment commonly includes screening, clarification, filtration, softening, membrane separation, and disinfection. Operators select each step after testing the source water and identifying process risks. They also monitor pH, conductivity, turbidity, hardness, and microbial indicators. The 2024 UN World Water Development Report states that 2.2 billion people lacked safely managed drinking water in 2022. This pressure makes industrial water efficiency more important. The World Resources Institute’s Aqueduct Water Risk Atlas reports that 25 countries face extremely high annual water stress. Reuse can help, but it is not automatically safe or economical.
Tips: Start with a water balance. Measure intake, use, losses, discharge, and reuse points. Set limits for critical parameters, then verify them regularly. Keep sampling records near the equipment. Small errors matter. A treatment train that works today may fail after seasonal changes, production shifts, or membrane fouling. Operators should review results, question unusual readings, and adjust carefully rather than trust a fixed recipe. Industry guidance and local discharge requirements should shape the final design.
Process water is water used inside an industrial operation, not simply water discharged from it. Its sources vary by site. Municipal supplies provide predictable quality, while groundwater and rivers may offer greater volume. Rainwater harvesting and treated wastewater can reduce freshwater demand, but they require careful monitoring.
The numbers explain the pressure. UNESCO’s 2022 World Water Development Report estimates that industry accounts for about 19% of global freshwater withdrawals. In a factory, process water may cool heat exchangers, produce steam, wash equipment, transport materials, or become part of a product. A cooling tower can lose water through evaporation, while a boiler needs low hardness to prevent scale. Even a small amount of oil, salts, or bacteria can affect performance.
Water quality is rarely uniform. That matters.
Treatment may include screening, filtration, softening, reverse osmosis, biological treatment, or disinfection. The correct combination depends on the source and final use. A food-processing line may need microbiological control, while a metal-finishing process may require tight control of dissolved minerals. The U.S. Geological Survey reports substantial industrial water withdrawals across manufacturing and mining activities, although figures differ by sector and accounting method. This limitation deserves attention. Reuse targets can look impressive until hidden losses, concentrate disposal, and seasonal water quality are measured. Reliable planning therefore begins with testing the actual water, mapping each use, and checking performance over time.
Process water is water used in industrial operations such as cooling, washing, production, steam generation, and material processing. Treatment helps remove suspended solids, dissolved contaminants, chemicals, and microorganisms so the water can be used safely and discharged or reused responsibly.
Agriculture is the largest user of freshwater worldwide, while industrial withdrawals include water used for manufacturing and process operations. Common process-water sources include surface water, groundwater, municipal supplies, rainwater, and treated wastewater. Selecting the right treatment method improves water quality, protects equipment, supports reuse, and reduces environmental impact.
Data shown are approximate global shares of freshwater withdrawals based on widely cited FAO AQUASTAT and UN-Water estimates; values vary by country and year.
Process water treatment begins with understanding what the water carries. A laboratory test measures pH, conductivity, suspended solids, oils, metals, and biodegradable compounds. This baseline matters. Without it, engineers may choose expensive equipment that solves the wrong problem. The UNESCO World Water Development Report 2024 estimates that industry uses roughly 20% of global freshwater withdrawals. That figure makes treatment more than a maintenance task. It becomes a practical water-security measure.
How does the treatment process work? Coarse screens remove fibers and debris first. An equalization tank then smooths sudden changes in flow and concentration. Chemical adjustment may follow, using coagulation and clarification to settle fine particles. Biological treatment reduces biodegradable pollutants through controlled microbial activity. Membranes can then remove dissolved solids, microorganisms, and smaller contaminants. Disinfection provides an additional barrier before reuse or discharge. The final step depends on the water’s purpose, such as cooling, boiler feed, or equipment washing. “Clean” is not one fixed standard. That assumption often fails. The U.S. Environmental Protection Agency’s Water Reuse Action Plan emphasizes fit-for-purpose treatment and reliable monitoring. Operators therefore test critical points continuously, not only at the outlet. Sludge and concentrated reject water also need controlled handling. A treatment train can look efficient on paper, yet real production changes, cleaning chemicals, and sensor drift can reduce performance. Experienced teams leave room for adjustment.
| Process Stage | Primary Purpose | Typical Contaminants or Parameters | Common Treatment Technologies | Typical Monitoring Data | Contribution to Water Quality |
|---|---|---|---|---|---|
| 1. Water Characterization | Identify the water source, variability, treatment objectives, and potential risks before selecting equipment. | pH, temperature, turbidity, total suspended solids, conductivity, hardness, alkalinity, organic matter, metals, oils, and microbiological activity. | Laboratory analysis, online sensors, sampling plans, and mass-balance calculations. | pH is commonly measured on a 0–14 scale; conductivity is usually reported in µS/cm or mS/cm; turbidity is reported in NTU. | Creates the design basis for reliable and cost-effective treatment. |
| 2. Screening and Equalization | Remove large debris and reduce fluctuations in flow and contaminant concentration. | Rags, plastics, fibers, sand, grit, sudden pH changes, and variable pollutant loads. | Bar screens, strainers, grit removal, collection tanks, mixing, and flow-control systems. | Flow rate, tank level, pH, temperature, and visible solids. | Protects downstream equipment and improves process stability. |
| 3. pH Adjustment and Chemical Conditioning | Bring water chemistry into a suitable range for coagulation, biological treatment, corrosion control, or membrane operation. | Acidity, alkalinity, high or low pH, dissolved metals, and scaling potential. | Acid or alkali dosing, alkalinity addition, oxidation, reduction, and antiscalant dosing where appropriate. | pH, alkalinity, oxidation-reduction potential, and chemical dosage. | Improves treatment performance and helps prevent corrosion, precipitation, and membrane fouling. |
| 4. Coagulation and Flocculation | Destabilize fine particles and combine them into larger, settleable or floatable flocs. | Colloids, suspended solids, color, phosphorus, and some organic matter. | Coagulants such as iron or aluminum salts, polymers, rapid mixing, and gentle flocculation. | pH, chemical dose, mixing conditions, floc size, turbidity, and settled solids. | Reduces particle loading on clarification, filtration, and membrane systems. |
| 5. Clarification or Dissolved Air Flotation | Separate flocs, suspended solids, and buoyant materials from the water. | Suspended solids, precipitated metals, oils, grease, and flocculated particles. | Sedimentation tanks, tube settlers, lamella clarifiers, and dissolved air flotation units. | Influent and effluent turbidity, sludge blanket depth, surface loading, and solids concentration. | Produces clarified water and concentrated sludge for further handling. |
| 6. Media Filtration | Remove remaining suspended particles and protect downstream treatment units. | Fine solids, residual flocs, turbidity, iron, manganese, and some organic particles. | Multimedia filters, sand filters, cartridge filters, and specialty adsorption media. | Turbidity, filter differential pressure, flow rate, and backwash frequency. | Improves clarity and reduces fouling risk for membranes and heat-transfer equipment. |
| 7. Softening and Scale Control | Reduce hardness and scaling-forming ions when required by the industrial process. | Calcium, magnesium, carbonate hardness, silica, and other scale-forming constituents. | Lime softening, ion exchange, nanofiltration, reverse osmosis, and controlled chemical dosing. | Total hardness, calcium, magnesium, alkalinity, conductivity, and calculated scaling indices. | Helps prevent scale deposits in boilers, cooling systems, piping, and membranes. |
| 8. Membrane Treatment | Remove dissolved salts, microorganisms, colloids, and low-molecular-weight contaminants according to membrane type. | Dissolved solids, hardness, nitrate, ions, bacteria, viruses, and fine colloids. | Microfiltration, ultrafiltration, nanofiltration, and reverse osmosis. | Feed and permeate conductivity, pressure, recovery, flux, turbidity, and normalized membrane performance. | Produces high-quality water for process use, boiler feed, rinsing, or reuse. |
| 9. Activated Carbon or Advanced Organic Treatment | Reduce dissolved organic compounds, taste-and-odor compounds, residual oxidants, or specific trace contaminants. | Oil residues, solvents, pesticides, dissolved organic carbon, and chlorine or other oxidants. | Granular activated carbon, powdered activated carbon, ozone, ultraviolet advanced oxidation, or chemical oxidation. | Total organic carbon, ultraviolet absorbance, oxidation-reduction potential, and target contaminant concentrations. | Improves chemical quality and protects sensitive manufacturing processes. |
| 10. Disinfection | Inactivate microorganisms and control biological growth in treated water and distribution systems. | Bacteria, viruses, protozoa, biofilm-forming organisms, and microbial regrowth. | Ultraviolet light, ozone, chlorine, chlorine dioxide, or other approved disinfectants. | Ultraviolet dose, disinfectant residual, contact time, temperature, and microbial testing. | Reduces biological risks and helps maintain water quality during storage and distribution. |
| 11. Final Conditioning and Storage | Adjust treated water for its intended use and maintain quality until consumption. | Residual disinfectant, dissolved gases, pH imbalance, corrosion potential, and recontamination risk. | pH correction, remineralization, degassing, final filtration, storage tanks, and recirculation loops. | pH, conductivity, temperature, disinfectant residual, tank level, and recirculation flow. | Ensures water remains suitable and consistent at the point of use. |
| 12. Sludge and Concentrate Management | Handle treatment residuals safely and minimize environmental impact. | Chemical sludge, biological solids, rejected salts, concentrated organics, and spent filter media. | Thickening, dewatering, stabilization, evaporation, recovery, permitted discharge, or approved disposal. | Solids concentration, moisture content, conductivity, chemical composition, and disposal volume. | Supports regulatory compliance and reduces waste-handling costs. |
Process water treatment removes contaminants from water used in manufacturing, cooling, cleaning, and production. The treatment train depends on the wastewater’s chemistry, temperature, flow, and reuse target. Operators usually begin with screens and equalization tanks. Screens catch fibers, plastics, and larger solids, while equalization reduces sudden changes in flow and concentration.
Coagulation and flocculation help small particles form larger groups. Sedimentation or dissolved air flotation then separates these solids. Biological treatment can reduce biodegradable organic matter through controlled microbial activity. Membrane technologies provide finer separation. Ultrafiltration removes suspended solids and many microorganisms, while reverse osmosis reduces dissolved salts and selected contaminants. Activated carbon can adsorb odors and trace organic compounds. Ion exchange may control specific dissolved ions, especially where water reuse requires stable conductivity. Disinfection with ultraviolet light or carefully controlled chemicals provides an additional microbial barrier.
Reliable systems combine treatment stages with regular testing. Technicians may check pH, turbidity, conductivity, chemical oxygen demand, and microbial indicators at different points. A clear water sample is not always safe for reuse. That assumption can be costly. Process records, calibrated instruments, and well-maintained sensors support dependable decisions. No single technology fits every facility. A membrane system may achieve excellent quality, yet concentrate management can remain difficult. Biological treatment may lower operating costs, but temperature changes can affect performance. Practical design requires pilot testing, operator experience, and room for adjustment when production conditions change.
Process water treatment is the controlled management of water used inside industrial operations. It may support washing, cooling, heating, rinsing, or production. Unlike drinking water treatment, its target depends on the process. Water with excess hardness can leave scale on heat exchangers. Suspended solids may clog spray nozzles. Oil, salts, or microbes can also affect product quality and equipment life.
Why is process water treatment important? It protects production reliability. Clean, balanced water helps equipment transfer heat, move fluids, and operate within design conditions. This can reduce unplanned shutdowns and maintenance pressure. It also supports consistent products, especially where water touches ingredients, surfaces, or precision components. Proper treatment can lower freshwater demand by enabling safe reuse, but reuse requires careful monitoring. Conductivity, pH, temperature, turbidity, and biological indicators should match the process risk. Numbers matter.
Treatment also helps facilities meet discharge limits and document responsible water management. Yet treatment is not a magic shield. A system can fail when sensors drift, filters load up, or operators trust old settings. Regular sampling and calibrated instruments reveal these weaknesses. Good programs connect laboratory results with daily observations, such as cloudy water, rising pressure, or unusual odors. The uncomfortable lesson is simple: more chemicals do not always mean better treatment. Conditions change, and treatment plans must change with them.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

