What Is Sheetmetal Fabrication and What Types Are There?

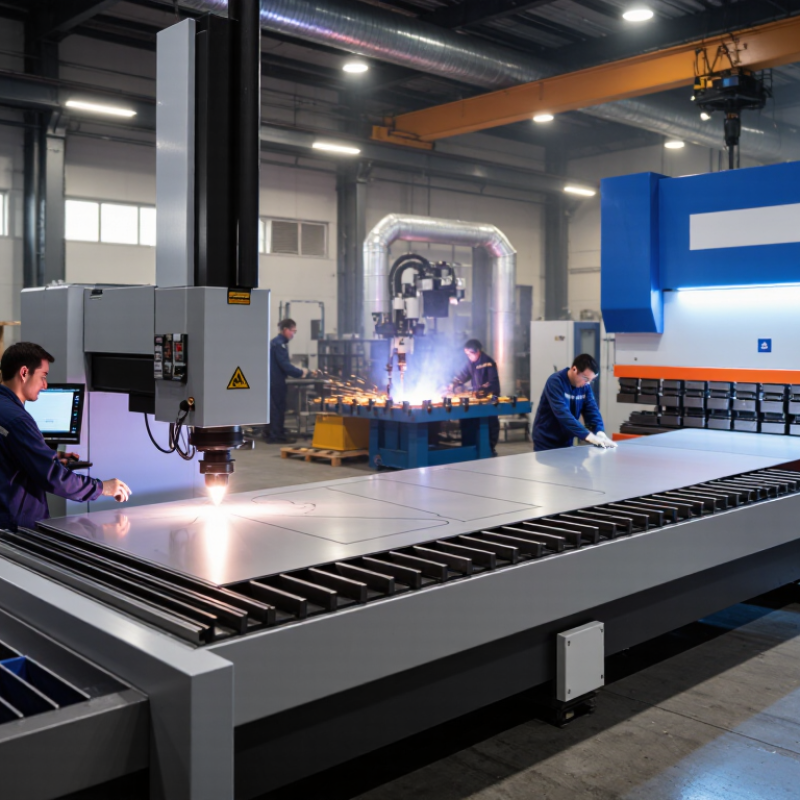
Sheetmetal fabrication is the process of transforming flat metal sheets into useful, accurate components. It supports industries such as construction, transportation, electronics, and industrial equipment. A steel enclosure, an aluminum duct, or a stainless steel bracket may begin as a simple sheet. Skilled fabricators then cut, bend, form, join, and finish it according to detailed specifications.

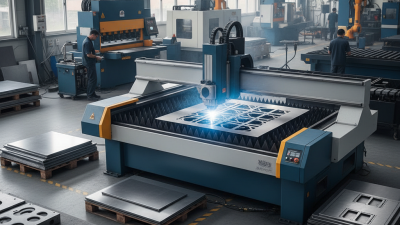
The work combines practical experience with engineering control. Material thickness, alloy selection, bend allowance, grain direction, and surface finish all influence the final result. Common methods include laser cutting, waterjet cutting, punching, press brake forming, rolling, welding, riveting, and fastening. Each method offers different benefits. Laser cutting creates precise profiles, while press brakes produce controlled angles. Welding can create strong assemblies, but heat may cause distortion if technicians overlook it.

There is no single best fabrication method. The correct choice depends on tolerance, production volume, geometry, material, and cost. Prototype work may favor flexible laser cutting and manual forming. Large production runs may benefit from automated punching or dedicated tooling. Experienced teams also inspect dimensions, edges, welds, and finishes throughout production. Small errors matter.

Quality depends on more than machinery. It requires readable drawings, calibrated equipment, trained operators, and documented inspections. Even experienced professionals can misjudge springback or overlook a tight assembly clearance. That is why fabrication planning should include testing and honest review. This guide explains what sheetmetal fabrication involves and examines its major types, processes, applications, advantages, and practical limitations.
What Is Sheetmetal Fabrication and What Types Are There?

What Is Sheet Metal Fabrication?

What Is Sheet Metal Fabrication?

Sheet metal fabrication is the process of turning flat metal sheets into useful parts or structures. Technicians cut, bend, punch, roll, and join metal to match a drawing or physical requirement. Common materials include steel, aluminum, and stainless steel. The chosen material affects strength, weight, corrosion resistance, and finishing options.

A typical project begins with a digital design and a suitable sheet thickness. Cutting may use shears, lasers, or punching equipment. Press brakes then create accurate angles, while welding or fastening joins separate pieces. Skilled fabricators check dimensions with calipers, gauges, and templates. Even a small bend error can affect final assembly. Results are rarely perfect on the first attempt, especially when material springs back after bending. That is why practical experience still matters beside modern equipment.

Tips: Confirm the material grade, thickness, grain direction, and bend radius before production. Leave space for fasteners and finishing layers. Ask for a sample part when tolerances are critical. Inspect edges for burrs, cracks, and sharp corners. A clear drawing prevents expensive corrections, although drawings can still miss real-world details. Good fabrication depends on careful planning, controlled processes, and honest inspection at every stage.
Materials, Tools, and Equipment Used in Sheet Metal Fabrication

Sheet metal fabrication turns flat metal stock into enclosures, brackets, ducts, panels, and structural parts. Common materials include carbon steel, stainless steel, aluminum, copper, and galvanized steel. Each behaves differently under heat, pressure, and cutting force. Aluminum is light and corrosion resistant, but it can distort during welding. Stainless steel handles harsh environments, though it needs tighter control during forming.

The World Steel Association reported global crude steel production of about 1.89 billion metric tons in 2023. That scale supports a broad supply chain for fabricated components. Tools usually begin with measuring gauges, scribes, clamps, and layout tables. Production equipment may include shears, press brakes, laser cutters, punches, rollers, and welding systems. CNC controls improve repeatability, while deburring tools remove sharp edges around holes and cut lines. Small details matter.

Grand View Research estimates that the global sheet metal fabrication services market will grow steadily through 2030, supported by construction, transportation, and industrial equipment demand. In practice, material thickness often determines the process. Thin aluminum may suit precision cutting and controlled bending. Heavy plate may require plasma cutting, forming, and multi-pass welding. I have seen drawings fail because bend allowances were treated as an afterthought. That mistake is avoidable, but not always obvious. Skilled fabricators still inspect grain direction, springback, weld distortion, surface finish, and dimensional tolerance before release. A clean part is not automatically a reliable part.

The Main Steps in the Sheet Metal Fabrication Process

Sheet Metal Fabrication: The Main Process

Sheet metal fabrication turns flat metal sheets into precise parts, enclosures, and structural components. Common methods include cutting, bending, punching, forming, and welding. The work begins with a drawing or digital model. Engineers check dimensions, material thickness, bend allowances, and tolerance requirements before production. Small errors here can cause expensive rework later.

The fabrication process starts with material selection. Steel, aluminum, and stainless steel behave differently during cutting and bending. Operators then cut the sheet using a suitable machine, leaving clean edges and accurate profiles. Bending follows, often with several measured folds. Each bend must account for springback, or the metal may return slightly toward its original shape. Parts may then be punched, rolled, welded, or fastened together. Surface finishing removes sharp edges and improves corrosion resistance. Inspection checks hole positions, angles, weld quality, and overall fit. In practice, even a well-planned job may need adjustment after the first trial part.

Tips: Confirm the material grade before cutting. Keep drawings updated after every design change. Measure the first finished part carefully. Protect completed surfaces from scratches during handling. Do not ignore tiny burrs; they can affect assembly and safety. Experienced fabricators also record machine settings, because repeatability depends on more than the drawing alone.

What Is Sheet Metal Fabrication and What Types Are There? — The Main Steps in the Sheet Metal Fabrication Process
Category Type or Process Stage What It Involves Common Methods or Equipment Typical Results and Key Considerations
Definition Sheet Metal Fabrication The conversion of flat metal sheets into finished parts, enclosures, panels, brackets, ducts, and structural components through cutting, forming, joining, and finishing. Computer-aided design, cutting machines, forming equipment, welding systems, and inspection tools. Parts are designed around material properties, sheet thickness, bend allowances, tolerances, and the intended service environment.
Fabrication Type Cutting Separating a sheet into a required profile or blank before forming or assembly. Shearing, laser cutting, plasma cutting, waterjet cutting, and punching. Laser cutting is suited to detailed profiles; shearing is efficient for straight cuts; punching can create holes, slots, and repeated features.
Fabrication Type Bending and Forming Applying controlled force to change the angle or shape of sheet metal without removing material. Press brakes, roll forming machines, folding machines, stamping presses, and forming dies. Designs must account for bend radius, springback, grain direction, flange length, and possible deformation.
Fabrication Type Joining Connecting two or more sheet-metal components into an assembly. MIG welding, TIG welding, resistance spot welding, riveting, bolting, clinching, and mechanical fastening. Joint selection depends on load, accessibility, appearance, heat input, corrosion risk, and whether future disassembly is required.
Fabrication Type Finishing Improving surface appearance, corrosion resistance, wear resistance, or compatibility with later assembly. Deburring, grinding, brushing, polishing, powder coating, wet painting, plating, and anodizing for suitable aluminum parts. Finishing requirements should specify surface preparation, coating system, color, coverage, thickness, and inspection criteria.
Main Step 1. Design and Engineering Developing a manufacturable part design and defining material, thickness, dimensions, tolerances, bend details, and finish. CAD models, flat-pattern development, technical drawings, design-for-manufacturing reviews, and tolerance analysis. Good design reduces scrap, avoids impossible bends, provides adequate tool access, and supports efficient assembly.
Main Step 2. Material Selection Choosing sheet stock according to strength, weight, corrosion resistance, ductility, conductivity, appearance, and cost. Common material families include carbon steel, stainless steel, aluminum, galvanized steel, and copper alloys. Material grade and thickness affect cutting behavior, forming force, weldability, springback, surface treatment, and final performance.
Main Step 3. Cutting and Blanking Producing the flat blank or individual features from the selected sheet. CNC laser cutting, CNC punching, mechanical shearing, plasma cutting, or waterjet cutting. Important controls include dimensional accuracy, kerf or clearance, heat-affected areas, edge quality, nesting efficiency, and material utilization.
Main Step 4. Deburring and Edge Preparation Removing sharp edges, burrs, slag, and unwanted surface irregularities left by cutting. Manual deburring, abrasive belts, tumbling, edge-rounding machines, brushing, and grinding. Proper edge preparation improves handling safety, coating adhesion, fit-up, and the quality of welded or assembled joints.
Main Step 5. Forming and Bending Creating the required angles, channels, curves, flanges, embossments, or three-dimensional shapes. Press-brake air bending, bottoming, coining, roll forming, stamping, and progressive forming. Critical variables include tooling selection, bend sequence, inside radius, bend deduction, material grain, and springback compensation.
Main Step 6. Joining and Assembly Combining formed components and attaching hardware or subassemblies. Welding, riveting, screws, bolts, threaded inserts, clinching, adhesives, and self-clinching fasteners. Assemblies should be checked for distortion, joint strength, alignment, accessibility, cleanliness, and electrical continuity when applicable.
Main Step 7. Surface Finishing Applying the specified protective or decorative treatment after fabrication and cleaning. Powder coating, liquid painting, plating, passivation for suitable stainless-steel applications, anodizing for aluminum, and polishing. Surface preparation, masking, drainage, curing conditions, coating coverage, and compatibility between the substrate and finish are important.
Main Step 8. Inspection and Quality Control Verifying that the finished part meets drawing, functional, appearance, and safety requirements. Calipers, micrometers, height gauges, angle gauges, coordinate measuring equipment, visual inspection, and coating-thickness gauges. Typical checks include dimensions, hole locations, bend angles, flatness, weld quality, surface condition, coating coverage, and assembly fit.
Main Step 9. Packaging and Delivery Protecting completed parts from scratches, corrosion, contamination, and deformation during storage and transport. Protective films, separators, edge guards, moisture-resistant packaging, pallets, and custom shipping containers. Packaging should reflect part geometry, surface sensitivity, weight, stacking limits, and environmental exposure during transit.
Note: Actual process selection, achievable tolerances, bend radii, and suitable sheet thicknesses vary according to the material grade, part geometry, equipment, tooling, and applicable quality requirements.

Common Types of Sheet Metal Fabrication

Sheet metal fabrication turns flat stock into accurate parts for enclosures, brackets, ducts, and machine frames. Common types begin with cutting, using laser, plasma, waterjet, or mechanical shears. Laser cutting suits fine profiles and small holes, while plasma handles thicker steel quickly. Punching creates repeated holes; stamping forms high-volume parts with dies. Grand View Research reported a global metal fabrication market value of about US$16.35 billion in 2023.

Bending uses a press brake to create flanges, channels, and boxes. Rolling produces cylinders and curved panels. Deep drawing pulls sheet into cups or housings, but thinning can cause cracks. Welding joins formed pieces, although heat may distort thin material. A 2024 MarketsandMarkets report estimated the sheet metal fabrication services market at roughly US$16.2 billion and projected about US$20.5 billion by 2029. These figures suggest strong demand, but market forecasts are not guarantees.

Tips: Match the process to the part, not habit. Define material grade, thickness, bend radius, tolerance, and production volume before quoting. Inspect the first article with calipers and a gauge. Small errors become expensive. CAD models can hide bend deductions, burrs, or springback, so a trial piece remains valuable. One uncomfortable lesson: the cheapest operation is not always the lowest-cost choice.

Applications, Advantages, and Limitations of Each Fabrication Type

What Is Sheet Metal Fabrication and What Types Are There?

Applications, Advantages, and Limitations of Each Fabrication Type

Sheet metal fabrication converts flat metal sheets into useful components through cutting, forming, and joining. The market continues expanding across construction, transport, electronics, and energy equipment. Grand View Research valued the global sheet metal fabrication services market at approximately USD 17.5 billion in 2023. The World Steel Association also reported 1.89 billion tonnes of crude steel production that year. These figures show strong material availability, although demand varies by region.

Laser cutting creates precise openings and complex profiles with limited physical contact. It suits electrical enclosures, machine panels, and architectural parts. Its accuracy reduces waste, but thick materials can increase cutting time and energy use.

Stamping produces large volumes quickly, especially for vehicle brackets and appliance shells. It offers repeatable dimensions and low unit costs. Tooling is expensive, however, and design changes become difficult after production begins.

Press-brake forming bends sheets into channels, frames, and covers. It requires modest tooling and supports flexible production. Springback can still affect final angles.

Welding joins separate pieces for tanks, frames, and structural assemblies. It handles thick sections well, but heat may cause distortion or visible marks.

Powder coating and other finishes improve corrosion resistance, yet they add processing steps and inspection needs.

In practice, the “best” method is rarely universal. Material grade, batch size, tolerance, and repair access can change the decision. Even experienced engineers sometimes underestimate setup time.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.