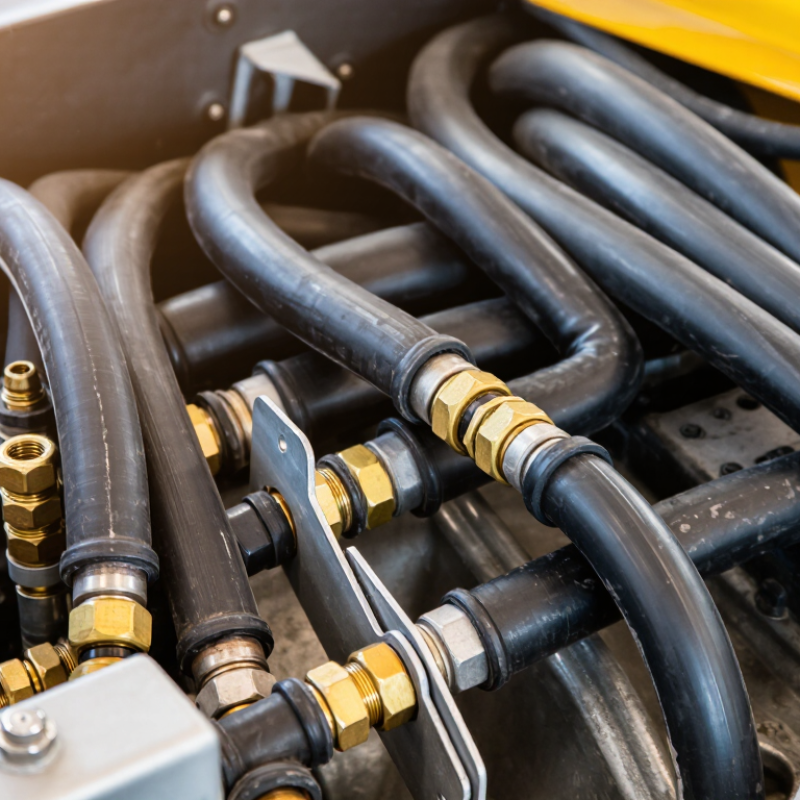
Choosing the right Hydraulic Rubber Hose is not a minor purchasing task. It affects machine safety, uptime, maintenance costs, and operator confidence. A hose may look strong on a workbench, yet fail quickly beside a hot engine or sharp steel bracket. Pressure matters. Temperature, fluid compatibility, bend radius, abrasion, and movement matter too.
Brendan Casey, a respected hydraulic systems author and educator, offers a practical warning: “The right hose is the one that survives the application, not merely the pressure test.” That idea should guide every selection. A hose rated for 3,000 psi may still be unsuitable for a system carrying heated oil through repeated flexing. Small details decide the result.
This guide presents seven practical tips for choosing a Hydraulic Rubber Hose with greater confidence. It explains how to read pressure ratings, check internal diameter, match materials, and measure installation space. It also considers routing, fittings, environmental exposure, and replacement timing. Look closely at the real workplace. Dust may collect around the coupling. A hose may rub against a frame during every cycle. The bend may be tighter than the catalog image suggests.
Perfect selection is not always possible. Assumptions can fail. Even experienced technicians sometimes overlook vibration or seasonal temperature changes. That is why inspection, documentation, and honest risk assessment belong in the process. The safest choice is rarely the cheapest hose on the shelf. It is the hose that matches the complete application, including the parts nobody notices at first.
A hydraulic hose must match the system’s real pressure demands, not just its normal gauge reading. Check the maximum working pressure, including startup surges and sudden valve closures. A hose rated slightly above normal pressure may still fail during repeated pressure spikes. Select a suitable safety margin.
Temperature needs equal attention. Measure the fluid temperature near the hose, then check the surrounding air temperature. Hot oil can weaken the tube, while cold conditions may reduce flexibility and increase cracking. Do not rely on one temperature figure. The hose must handle both extremes continuously.
During field inspections, I have found that pressure and temperature are often recorded separately. That approach can miss their combined effect. A hose operating near its pressure limit becomes less forgiving when exposed to heat. Review the hose specification, fluid type, duty cycle, and expected impulse frequency before ordering. Compatibility matters too, because an unsuitable fluid can damage inner layers without obvious external signs. Keep the details visible.
A practical check is to compare the selected hose rating with the highest measured pressure, not the average. Install test gauges where pressure changes are likely. I once saw a hose chosen correctly on paper, yet its temperature rating was based only on room conditions. The application later ran much hotter. That oversight deserved more questioning. Record actual readings during cold starts, peak loads, and extended operation. Small data gaps can become expensive failures.
7 Tips for Choosing the Right Hydraulic Rubber Hose
Match the Hose Material to the Hydraulic Fluid
Hydraulic hose selection starts with the fluid, not the fitting. Two hoses with identical dimensions may react differently inside the same circuit. Petroleum-based oils commonly suit nitrile rubber, which handles many industrial temperatures and pressures. Water-based fluids often require EPDM, because petroleum-resistant compounds may deteriorate in them. That difference matters.
Check the fluid’s exact formulation and operating temperature before choosing the inner tube. Hydraulic additives can change compatibility, especially during long shifts or high heat. For aggressive chemicals or elevated temperatures, PTFE may be appropriate, but the complete assembly still needs review. Do not judge compatibility by color or flexibility. A soft hose is not automatically a safe hose.
Use current compatibility data from the hose manufacturer, then compare it with your system conditions. Review the inner tube, cover, fittings, and seals together. In field inspections, swelling, sticky surfaces, and small cracks often indicate fluid incompatibility. Replace the hose if its bore feels enlarged or unusually hard. A compatibility chart is useful, but it is not infallible. Fluid mixtures and changing temperatures can expose gaps in a simple selection process. When uncertainty remains, test a sample under controlled conditions and document the result. Small details prevent expensive failures.
| No. | Selection Tip | Hydraulic Fluid or Service | Commonly Suitable Tube Material | Why It Is Used | Important Check |
|---|---|---|---|---|---|
| 1 | Match the tube material to the fluid | Petroleum-based hydraulic oils | Nitrile rubber (NBR) | NBR provides good resistance to mineral oils and is widely used in general hydraulic service. | Do not assume compatibility with phosphate-ester, water-based, or biodegradable fluids. |
| 2 | Use a water-compatible elastomer when required | Water-glycol fluids, water-based fire-resistant fluids, and hot water | Ethylene propylene rubber (EPDM) | EPDM generally performs well with water, steam, and many water-based fluids. | EPDM is generally unsuitable for petroleum oils; confirm the exact fluid formulation and temperature. |
| 3 | Check compatibility with phosphate-ester fluids | Phosphate-ester fire-resistant hydraulic fluids | EPDM or PTFE, when specifically approved | These materials can offer better resistance than standard oil-service NBR in phosphate-ester applications. | Hose-cover, reinforcement, fitting, and seal compatibility must also be verified. |
| 4 | Select higher chemical and temperature resistance when needed | High-temperature mineral oils and selected aggressive fluids | Fluorocarbon rubber (FKM) or PTFE | FKM offers strong resistance to heat and many oils; PTFE offers broad chemical resistance and a smooth, low-friction bore. | Verify pressure-pulse, flexing, permeation, and minimum-bend-radius requirements. |
| 5 | Confirm the complete temperature range | Cold starts, continuous heat, or rapid temperature cycling | Material selected from the hose construction rating | Elastomer stiffness, aging, and fluid resistance change significantly at temperature extremes. | Use the lowest ambient temperature and highest fluid temperature, not only the normal operating value. |
| 6 | Match pressure and impulse performance | High-pressure circuits, pulsating loads, and hydraulic shock | A hose construction with the required wire or textile reinforcement | Tube chemistry alone does not determine pressure capability; reinforcement and construction are equally important. | Choose a working-pressure rating above the system's maximum pressure, including transient spikes. |
| 7 | Evaluate the outer cover and installation environment | Outdoor exposure, abrasion, ozone, chemicals, and moving equipment | Cover material selected for the surrounding environment | A compatible tube can still fail if the cover is damaged by abrasion, ultraviolet light, ozone, heat, or external chemicals. | Provide guards or routing support where necessary and observe the specified bend radius. |
Choosing a hydraulic hose starts with flow, not outside diameter. Measure the actual pump flow in gallons per minute, then calculate velocity with this field formula: velocity = 0.4085 × flow ÷ inside diameter². A 10-gpm circuit through a 1-inch bore produces about 4.1 feet per second. That may suit a return line, but a suction line usually needs slower flow. Lower velocity reduces heat, noise, and pressure loss.
Tip: Match the hose bore to the circuit’s peak flow, not its average flow. ISO 4413 recommends controlling flow velocity to limit heat and pressure losses, while SAE J517 tables provide hose dimensions, pressure ratings, and test requirements. Use those values with the machine’s duty cycle. A hose rated for 20 gpm may still perform poorly when fittings, sharp bends, or long runs restrict the passage. I once trusted the nominal size alone. That shortcut missed a restrictive elbow.
Tip: Compare pressure drop across the complete assembly. Include the hose, adapters, couplings, and valve ports. The Hydraulic Institute’s pump-system guidance treats system resistance as a core sizing factor, not a minor detail. Record oil temperature, peak pressure, and start-up flow during commissioning. Then inspect the hose after several operating hours. A warm surface, pulsing gauge, or slow actuator suggests the sizing deserves another review. Perfect calculations can still meet imperfect field conditions.
Select the correct hose size and flow capacity before checking pressure, temperature, flexibility, and compatibility.
Approximate flow capacities are calculated from nominal hose inside diameter using a recommended hydraulic velocity of 6 m/s. Larger hose sizes reduce pressure loss and help maintain efficient fluid flow. Always verify the final selection against the system pressure, temperature, fluid type, hose construction, and application requirements.
Check flexibility before checking price. A hose should bend naturally without folding or flattening. In field inspections, stiff hoses often create stress near fittings. Choose reinforcement and materials suited to the working temperature. Cold conditions can make rubber less flexible. Hot fluid can accelerate aging. Leave enough hose length for movement, but avoid loose loops. A loop can catch nearby equipment.
Respect the minimum bend radius printed in the technical data. Measure the radius from the hose centerline, not its outside edge. A sharp bend can damage reinforcement, even when the outer cover looks normal. Never twist a hose during installation. Twisting changes its pressure behavior and may loosen connections. Use correctly positioned clamps to control movement without crushing the hose. Small details matter.
Study the installation space before selecting the final hose assembly. Check clearance around ports, cylinders, guards, and moving joints. A compact route may look efficient, but it can force an unsafe bend. Allow room for inspection and replacement. I once saw a hose rub against a metal bracket because the drawing ignored vibration. The failure was preventable. My early inspections also focused too much on static fit. Movement testing would have exposed the problem sooner. Move the equipment through its full operating range, then inspect for rubbing, stretching, and kinking. Leave practical access for technicians.
A hose can look perfect and still fail at the fitting. Measure the port, thread type, sealing face, and hose inside diameter before ordering. Confirm whether the connection uses metric, BSP, JIC, or another thread profile. Never force mismatched threads. That mistake can create leaks, damaged fittings, or sudden separation.
Check the hose against SAE J517 or ISO 18752, depending on the equipment and market. ISO 18752 defines performance classes, including impulse and pressure requirements. The U.S. Bureau of Labor Statistics recorded about 2.6 million nonfatal workplace injuries and illnesses in 2023. That figure is not hydraulic-specific, but it shows why preventable equipment failures deserve attention. Use the manufacturer’s pressure rating, including temperature and impulse limits. A hose rated for 3,000 psi may not safely handle pressure spikes at high temperatures.
Durability also depends on installation. Keep the bend radius above the stated minimum, support long runs, and prevent twisting during tightening. Shield exposed hoses from abrasion, sunlight, chemicals, and hot surfaces. Inspect for bulges, cracked covers, flattened sections, and rust near fittings. SAE J517 and ISO 18752 provide useful testing references, but field conditions remain harsher than a laboratory. I have seen hoses replaced too late because the outer cover looked acceptable. That judgment is unreliable. Record installation dates and inspect high-cycle lines more often.


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.