7 Tips for Choosing the Right Mother Roll Reel?
Choosing the right Mother Roll Reel is a production decision, not merely a purchasing task. It affects web stability, roll quality, changeover time, storage space, and operator safety. In a converting line, a small mismatch can appear as telescoping edges, uneven tension, or damaged cores. These problems may seem minor. They can still create expensive waste.
Industry data supports closer equipment evaluation. The Flexible Packaging Association’s 2024 industry overview reports that flexible packaging remains a major U.S. packaging sector, with annual sales exceeding $40 billion. Smithers’ The Future of Global Flexible Packaging to 2028 also highlights continued growth in flexible materials, driven by lightweight packaging and material efficiency. More production volume means greater pressure on reel accuracy and uptime. PMMI’s 2024 packaging trends research further emphasizes automation, labor efficiency, and operational flexibility as important investment priorities.
This guide examines seven practical factors for selecting a Mother Roll Reel, including material compatibility, maximum roll weight, web width, core dimensions, tension control, automation, and after-sales support. A reliable choice should match today’s line without blocking tomorrow’s upgrades. That sounds obvious. It is often overlooked.
In real facilities, specifications rarely align perfectly. A reel rated for maximum capacity may still perform poorly with delicate film or recycled paper. Operators may also value quick loading more than a brochure suggests. Therefore, compare supplier data with trial results, maintenance records, and actual floor conditions. The best decision is not always the most advanced model. It is the one that delivers stable rolls, predictable handling, and measurable value over time.
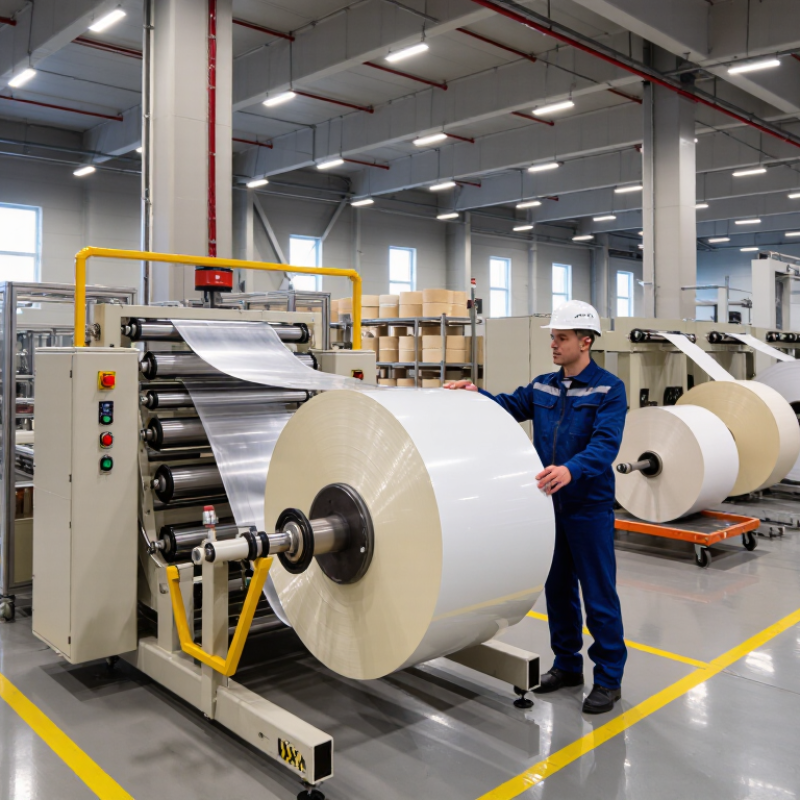
Map Line Requirements: 1,000–3,000 mm Web Width and 3–6 in Cores
Choosing the Right Mother Roll Reel: Match Web Width and Core Size
A reliable reel starts with a clear map of the production line. Record the usable web width, not only the machine’s maximum width. For most lines in this range, confirm support for 1,000–3,000 mm webs. Measure twice. A 2,950 mm roll may fail if the frame allows only 2,900 mm. Check edge clearance, shaft travel, and loading access. These details often matter more than advertised capacity.
Core selection needs equal care. Verify whether the line uses 3-inch, 4-inch, or 6-inch cores, and record the actual inner diameter. Core fit matters. A small mismatch can create runout, vibration, or uneven winding. Ask for the allowable core weight, outer diameter, and roll mass. Then compare those figures with your heaviest planned mother roll. Do not rely on one ideal production sample. Real material changes with moisture, coating thickness, and tension.
Review reel speed, braking response, and tension control across narrow and wide webs. Request documented test data, installation dimensions, and maintenance intervals from the supplier. If possible, inspect a working installation with similar widths and cores. A specification sheet cannot reveal every setup weakness. I once underestimated loading space; the reel met the width requirement but slowed changeovers. Leave room for that kind of mistake.
Size Roll Capacity for 1,000–2,000 mm Diameters and Rated Tonnage
Choosing a mother roll reel starts with diameter, not appearance. A 1,000 mm roll needs a different cradle than a 2,000 mm roll. ISO 3676:2012 identifies 1,200 × 1,000 mm as a standard unit-load footprint. This matters when the reel leaves the machine. CEPI’s 2023 Key Statistics report European paper and board production above 80 million tonnes. Heavy throughput makes capacity errors costly.
For a practical estimate, use the roll diameter, core diameter, width, and material density. A 1,500 mm roll with a 76 mm core, 1,200 mm width, and 700 kg/m³ density weighs about 1.48 tonnes. The same roll at 2,000 mm diameter weighs approximately 2.64 tonnes. These figures exclude pallets, shafts, moisture, and handling impact. Choose a rated tonnage above the calculated gross mass, with extra capacity for acceleration and uneven loading. A 20–30% working margin is sensible, although the correct margin depends on equipment design and site conditions.
Check the reel’s maximum diameter and cradle width together. A frame may carry the weight but still reject the roll geometry. I would also verify shaft load, brake capacity, floor strength, and fork clearance. Do not trust a neat spreadsheet blindly. Density changes across grades, and my estimate may be too optimistic without measured data. Record the heaviest real roll, not the average production roll.
Check Slitting Precision: ±1 mm Edge Control and Stable Web Tension
When choosing a mother roll reel, inspect the slit edge before admiring production speed. A clean edge requires lateral control within ±1 mm. That tolerance reduces trim waste, uneven unwinding, and unstable splice placement. The reel must also maintain web tension across its full width. Ask for tension records, not verbal promises. During a witnessed trial, measure edge position at the start, middle, and end. Test low, medium, and rated speeds.
The 2024 Smithers report, The Future of Flexible Packaging to 2028, values the global flexible packaging market at approximately US$288 billion in 2023. It forecasts continued growth toward 2028. This scale makes repeatable conversion more valuable than peak speed. Technical guidance from AIMCAL links tension variation with wrinkles, baggy lanes, and telescoping. Check dancer response, load-cell calibration, and taper-tension settings. A practical target is below 1% tension fluctuation during steady running. Material stiffness may require adjustment. Do not accept one perfect reel. Test three.
Inspect outer layers under side lighting. Look for wandering edges, powder, crushed cores, or a cone-shaped roll. Then unwind samples and compare width every few meters. A reel can hold ±1 mm briefly, then drift after thermal expansion. That is where evaluations become too optimistic. Ask how quickly the control system corrects errors. Request alarm limits and retained test data. Small gaps in the record matter. They reveal production risks early.
Compare Automation, Safety, Energy Efficiency, and Service Support
7 Tips for Choosing the Right Mother Roll Reel
A mother roll reel should match your actual production rhythm, not only its maximum speed. Check loading time, tension control, roll diameter, and changeover steps. The International Federation of Robotics reported 541,302 industrial robots were installed worldwide in 2023. This growth shows why automation matters, but full automation is not always economical. Compare automatic shaft handling, roll alignment, web guiding, and fault recovery. Ask operators to test the controls with gloves and limited visibility.
Safety deserves measurable attention. Review guarding, emergency stops, interlocks, braking, and safe access during roll changes. ISO 12100 provides a useful risk-assessment framework for machinery design. A reel with impressive output can still create dangerous pinch points. Look closely. Energy use also deserves a proper calculation. The International Energy Agency estimates motor-driven systems consume about 70% of industrial electricity. Therefore, compare motor efficiency, regenerative braking, standby consumption, and compressed-air demand. Request operating data at different loads, not only the best-case figure.
Service support often decides whether performance lasts. Check spare-parts availability, remote diagnostics, technician response times, training, and software update procedures. A 24-hour response promise sounds attractive, but define the actual coverage area. Ask for references from plants using similar roll weights and materials. I have seen specifications hide maintenance effort behind simple cycle-time figures. That is an imperfect comparison, but it deserves attention. The best choice balances automation, safety, energy efficiency, and practical support over the reel’s full working life.
7 Tips for Choosing the Right Mother Roll Reel
Compare automation, safety, energy efficiency, and service support
This neutral screening rubric rates the practical importance of seven selection factors on a 1–5 scale, where 1 means lower priority and 5 means critical. Confirm the final choice with measured throughput, energy consumption per output unit, documented safety compliance, changeover time, spare-parts availability, and supplier training or response commitments.





