


Buying Custom Steel Pipe is not merely a price comparison. It is a decision about pressure, corrosion, dimensions, traceability, and service life.
The World Steel Association reported global crude steel production of approximately 1.89 billion tonnes in 2023. That scale shows steel’s importance, but it does not guarantee a suitable pipe. The 2024 Global Steel Market Outlook also highlighted continuing volatility in energy, raw-material, and transport costs. These pressures can affect quotations, delivery dates, and material availability. Buyers should therefore verify more than a supplier’s catalog.
Edwin Basson, Director General of the World Steel Association, has stated, “Steel is a vital material for the future of our society.” His point applies directly to industrial purchasing. A pipe may look perfect on a warehouse floor. Its weld records, heat number, wall thickness, and test certificates may tell another story. Small details matter.
This guide presents 10 practical tips for buying Custom Steel Pipe successfully. It considers grade selection, outside diameter, wall tolerance, coating, end finishing, standards, inspection, packaging, and after-sales support. Ask for measurable evidence. Request mill certificates and dimensional reports before shipment. Confirm whether testing follows ASTM, ASME, API, or another required specification.
Be careful with the cheapest offer. It may exclude testing, coating, freight, or replacement protection. I have seen procurement plans focus heavily on unit price, then struggle with fit-up problems and delayed installation. That weakness is easy to overlook.
Good purchasing is not perfect. It is documented, questioned, and improved before the first pipe reaches the jobsite.
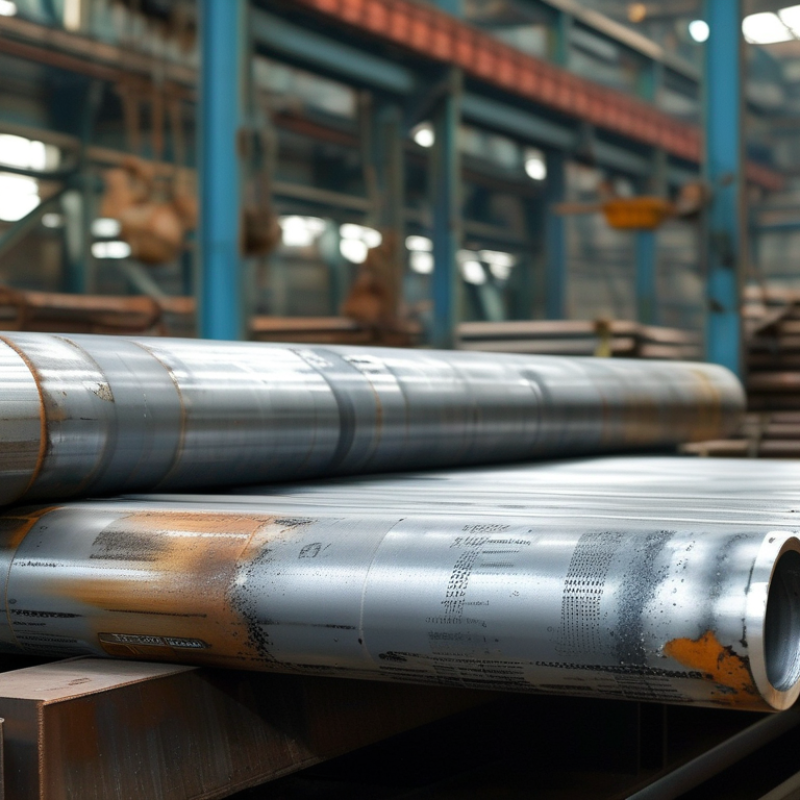
Before requesting a quotation, define exactly what your custom steel pipe must do. Describe the fluid, pressure, temperature, and installation environment. A pipe for outdoor cooling water needs different protection from one used indoors. I have seen projects delayed because buyers listed only diameter and length. That information is not enough. Specify outside diameter or nominal size, wall thickness, total length, and acceptable tolerances. Include the steel grade, manufacturing method, end connection, surface finish, and required corrosion resistance.
Tip Prepare a one-page requirement sheet. Add a simple drawing with dimensions, connection details, and inspection points. Mention whether cutting, drilling, bending, or coating is needed. Small details matter. Also state the expected quantity and delivery schedule, because custom production may require different tooling or batch planning. If the pipe will carry pressure, identify the applicable technical standard and testing requirements. Ask for material certificates, dimensional reports, and pressure-test records. Do not assume every supplier interprets standards identically.
Tip Challenge your own specifications. Are the tolerances truly necessary, or did someone copy them from an old project? I once treated a tight tolerance as essential, then learned the assembly allowed more movement. That mistake increased cost without improving performance. Still, reducing requirements too far can create leakage, poor alignment, or early corrosion. Review the design with an engineer, installer, and quality inspector. Their practical feedback can reveal missing details before production begins.
Choosing the right steel grade is the foundation of a successful custom pipe order. Start with the service conditions, not the supplier’s standard catalog. Check the fluid, operating temperature, pressure, corrosion risk, and outdoor exposure. A carbon steel grade may suit dry compressed air, but it can fail quickly in a salty or acidic environment. Stainless steel offers better corrosion resistance, although its cost and welding requirements may be higher.
Pipe specifications must match the actual installation. Confirm outside diameter, wall thickness, length tolerance, end preparation, and connection type. For pressure service, ask for the required design standard and hydrostatic or nondestructive testing records. For structural use, review yield strength, straightness, and surface condition. Small details matter. A few millimeters can disrupt alignment.
I once treated wall thickness as a minor purchasing detail. That was a mistake. The pipe fitted correctly, but its weight exceeded the support design. Avoid that shortcut. Request a clear drawing, material certificate, heat number, and inspection plan before production. Compare the stated grade with the applicable standard, and check whether welding changes the required heat treatment. Customization is useful, but unnecessary tolerances can increase cost without improving performance. Leave room for review. The first specification is rarely perfect.
When buying custom steel pipe, verify the supplier’s capabilities before discussing price. A suitable supplier should show traceable mill certificates, calibrated testing equipment, welding procedures, and documented inspection records. Ask whether its facility can meet your required outer diameter, wall thickness, tolerance, grade, and production volume. World Steel Association data reports about 1.89 billion tonnes of crude steel production in 2023. That scale makes traceability essential, because material quality can vary across mills and batches.
Tip: Request the certificate number, issuing body, scope, and expiry date. ISO’s Survey 2022 recorded 1,265,216 ISO 9001 certificates worldwide, but certification alone does not prove every pipe will meet your specification. Check whether the certificate covers manufacturing, testing, and the actual production site. A certificate for trading activities is not enough. Ask for recent third-party inspection reports and sample test results. Keep one physical sample when practical.
Tip: Match quality documents with contract requirements. Confirm chemical composition, tensile strength, hydrostatic pressure, non-destructive testing, and heat-number traceability. I have learned that suppliers may provide polished paperwork while missing a small dimensional detail. That gap can create expensive installation delays. Review drawings with the supplier’s engineer, not only a salesperson. Some checks feel excessive. They are cheaper than replacing a shipment. Still, I would reconsider any supplier that refuses reasonable audits or cannot explain an unclear test result.
Use recognized technical standards as a starting point when reviewing supplier documentation. The chart compares the specified minimum yield strength of common API 5L carbon steel pipe grades. Ask suppliers to provide material test certificates, traceability records, inspection results, and applicable quality certifications for the exact grade and size quoted.
Buying custom steel pipe is rarely about the lowest quotation. The World Steel Association reported 1.89 billion tonnes of crude steel production in 2023, showing the market’s enormous scale. Yet prices still vary with billet costs, energy, freight, diameter, wall thickness, coating, and testing. Request a line-by-line quotation. Check steel grade, outside diameter, tolerance, quantity, tooling, packaging, and delivery terms. Ask whether the price is fixed or linked to a published index. A low offer may exclude inspection or corrosion protection.
Lead time needs equal attention. OECD steel market reports have warned that global excess capacity could approach 630 million tonnes by 2026. Capacity does not guarantee your order arrives quickly. Confirm raw-material availability, production slots, welding, heat treatment, testing, and port handling. Request milestone dates, not one vague delivery promise. Add a written notice requirement for delays. Five days matter.
Contract terms expose weak planning. Define accepted standards, inspection points, mill certificates, sampling methods, and rejection rights. State who pays for rework, storage, retesting, and freight changes. Include dimensional tolerances and a clear remedy for short shipments. Payment milestones should follow measurable progress, such as approved drawings and passed inspection. I have seen buyers focus on unit price and miss packing details; that mistake can damage pipe ends before installation. Review governing law, dispute procedures, force-majeure language, and document deadlines with qualified counsel. Leave no blank fields.
10 Tips for Buying Custom Steel Pipe Successfully
Inspect the finished pipes before acceptance. A polished surface can still hide a thin wall or incorrect chemistry. I would not approve a shipment from photographs alone. The World Steel Association reported about 1.89 billion tonnes of crude steel production in 2023. That scale makes heat traceability essential, even for small custom orders.
Check each pipe against the purchase drawing. Measure outside diameter, wall thickness, length, straightness, bevel angle, and ovality. Use calibrated tools, not workshop guesses. ASME B36.10M provides dimensional guidance for welded and seamless steel pipe. ASTM E213 also describes ultrasonic examination practices for metal pipe and tubing. Ask for the actual inspection records. Generic certificates are weak evidence.
Match the heat number on every bundle with the material test report. Confirm yield strength, tensile strength, elongation, and chemical composition. Review hydrostatic or nondestructive testing results against the agreed specification. ISO 2859-1 can support sampling plans, but sampling cannot replace a clear acceptance rule. I have seen buyers count pipes while missing one badly marked piece. That mistake is easy to make. Photograph measurements, defects, and labels before signing the receiving report. If the coating is damaged, the ends are dented, or markings are unreadable, record it immediately. A rushed acceptance may save minutes and create weeks of rework.
| No. | Buying Tip | What to Verify on Finished Pipes | Practical Acceptance Criterion | Evidence to Keep |
|---|---|---|---|---|
| 1 | Define the complete pipe specification before ordering | Confirm outside diameter, wall thickness, pipe length, steel grade, manufacturing process, end finish, coating, and quantity. | Every requirement must match the approved purchase specification and the applicable standard, such as ASTM, EN, or API requirements selected for the project. | Approved technical data sheet, purchase order, and revision-controlled drawing. |
| 2 | Select the correct steel grade for the service | Check the material grade and chemical composition against the intended use, including pressure, temperature, corrosion, and weldability requirements. | The heat number, grade designation, and chemistry shown on the material certificate must correspond to the ordered grade and project specification. | Material test certificate, heat certificate, and traceability register. |
| 3 | Confirm dimensional tolerances in writing | Measure outside diameter, wall thickness, ovality, length, straightness, and end squareness using calibrated equipment. | All measurements must fall within the tolerances stated in the contract or applicable standard. Do not rely on nominal dimensions alone. | Inspection report with equipment identification and calibration status. |
| 4 | Review the manufacturing method | Identify whether the pipe is seamless, longitudinally welded, or helically welded, and verify that the process is suitable for the design application. | The actual manufacturing process must be the same as the process specified in the purchase order; unauthorized substitutions require written approval. | Manufacturing route, process qualification documents, and production batch records. |
| 5 | Inspect weld quality and weld areas | Check weld seams for visible cracks, lack of fusion indications, undercut, excessive reinforcement, arc strikes, and unacceptable surface defects. | Welds must meet the visual and nondestructive examination requirements defined by the selected pipe standard and project specification. | Visual inspection report, weld examination records, and repair log if applicable. |
| 6 | Require appropriate nondestructive testing | Confirm that the required ultrasonic, radiographic, magnetic-particle, or other examination has been completed on the specified quantity or percentage of pipes. | Test coverage, method, operator qualification, acceptance level, and results must satisfy the contract and applicable standard. | Nondestructive testing reports, examiner qualifications, and equipment calibration records. |
| 7 | Check hydrostatic or pressure-test requirements | Verify the test pressure, holding time, test medium, test temperature, and evidence of leakage or permanent deformation where pressure testing is required. | Each tested pipe or defined test lot must pass the specified pressure test without leakage or unacceptable deformation. | Pressure-test chart or certificate showing pressure, duration, pipe identification, and result. |
| 8 | Inspect surface condition and protective coating | Examine the external and internal surfaces for rust, laminations, dents, gouges, scale, contamination, coating holidays, and uneven coating coverage. | Surface defects must be within the permitted limits, and coating type, dry-film thickness, adhesion, and holiday-test results must meet the coating specification. | Surface inspection report, coating thickness readings, adhesion results, and holiday-test report. |
| 9 | Verify marking, traceability, and documentation | Match pipe markings, heat numbers, batch numbers, dimensions, grade, and inspection status with the packing list and certificates. | Each pipe or bundle must remain traceable from the finished product back to the material heat and inspection records. | Marking photographs, packing list, material certificates, and traceability matrix. |
| 10 | Complete a documented pre-acceptance inspection | Use a sampling plan or full inspection as required, record nonconformities, and confirm that corrective actions are closed before release. | Do not sign final acceptance or authorize shipment until dimensions, testing, appearance, quantity, packaging, and documentation are approved. | Signed inspection checklist, nonconformance reports, corrective-action evidence, and final release note. |


For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.
Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.
Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.
Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.
When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.
The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.
Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.
Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.
All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.
Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.
Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.
Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.
Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.
From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.
Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.
Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.
Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.
Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.
Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.
Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.
Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.

