


Top Auto Pipe Welding Machine Manufacturers Worldwide?

The global search for the Top Auto Pipe Welding Machine Manufacturers Worldwide reflects a changing industrial landscape. Energy projects, shipbuilding, pressure vessels, and process plants increasingly demand repeatable pipe welds. Operators now expect stable arc control, accurate alignment, lower rework, and clear production records. A strong Auto Pipe Welding Machine must perform consistently around carbon steel, stainless steel, and alloy pipe joints.

Market evidence supports this shift. Fortune Business Insights estimates that the global welding equipment market will grow from approximately USD 14 billion in 2024 to more than USD 21 billion by 2032. Grand View Research also reports strong growth in robotic welding, driven by labor shortages and improved automation. These figures describe broad equipment categories, not pipe welding alone. Definitions differ.

That matters.

Manufacturers should therefore be compared through practical evidence, not advertising claims. Important criteria include orbital or rotational control, welding power-source compatibility, torch positioning, cooling design, travel accuracy, and service support. AWS and ISO welding standards also emphasize procedure control, qualification, and inspection discipline. These requirements separate a dependable production system from a machine that only performs well during demonstrations.

This guide examines leading manufacturers through engineering capability, application experience, automation depth, customization, and after-sales support. It also considers operator usability, spare-part availability, and performance in dusty workshops or confined fabrication areas. No ranking is perfect. A supplier may excel in stainless-steel fabrication but offer limited support for heavy-wall pipeline work. Buyers should verify test welds, references, documentation, and total ownership costs before making a final decision.
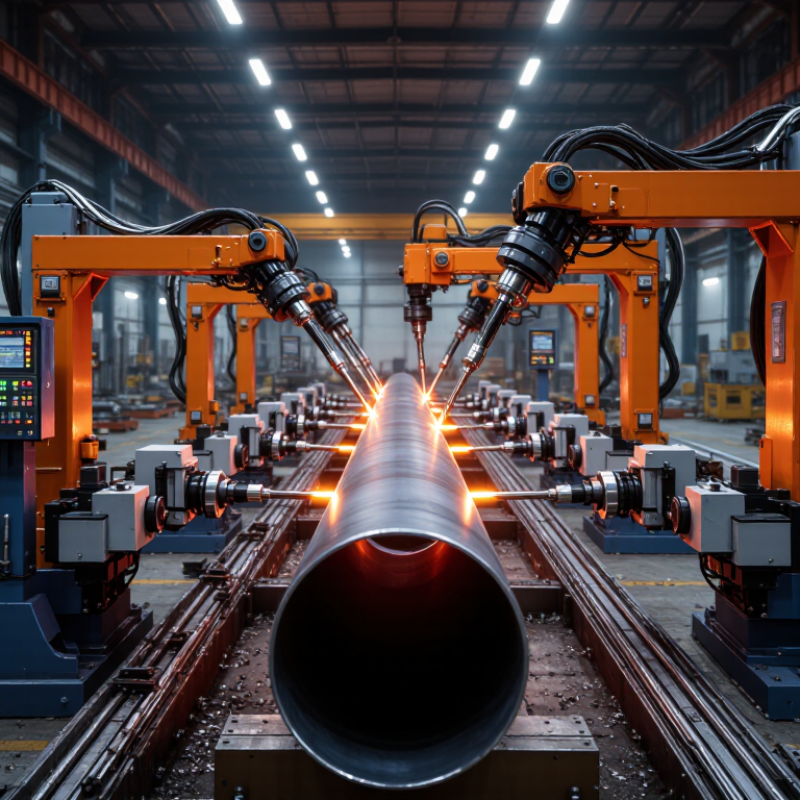
Top Auto Pipe Welding Machine Manufacturers Worldwide?

Definition and Role of Auto Pipe Welding Machines

An automatic pipe welding machine is an industrial system that joins pipe sections with limited manual torch movement. It aligns, rotates, and welds the joint according to programmed parameters. Unlike a hand-held torch, it coordinates travel speed, wire delivery, shielding gas, and arc control. That control matters. Pipe diameter, wall thickness, joint design, and metal type determine the correct settings. The machine does not understand a bad fit-up.

In field workshops, operators use these machines to improve repeatability across long production runs. Clamps hold the pipe, while a turning unit maintains a steady welding position. An operator sets the welding procedure, checks the joint preparation, and observes the arc during operation. Sensors may monitor rotation speed, temperature, or weld current. These records support inspection and process traceability. Still, automation is not magic. A warped pipe, contaminated surface, or poorly prepared edge can produce defects quickly. Even experienced teams must inspect the root, fill, and cap passes.

When evaluating manufacturers worldwide, buyers should examine documented testing, operator training, spare-part support, and machine adaptability. Factory trials with actual pipe materials can reveal problems hidden in brochures. Reliable suppliers explain capacity limits instead of promising universal performance. Maintenance access also deserves attention, especially around wire feeders, clamps, and cooling lines. One detail is often missed: software settings may be precise, but practical training determines how safely they are used. A fast machine with weak technical support can become an expensive interruption.


Key Technologies Used in Automated Pipe Welding

Automated pipe welding depends on coordinated motion, stable heat, and accurate sensing. Orbital welding systems rotate the torch around the pipe while controlling travel speed and arc length. This helps produce consistent joints on repeated production runs. TIG is often selected for clean root passes, while pulsed MIG or flux-cored processes can improve filling speed. The correct choice depends on wall thickness, alloy, joint design, and required inspection standards.

Modern machines use seam-tracking sensors to detect slight misalignment before the torch travels too far. Encoders monitor rotation and position. Closed-loop controls can adjust current, voltage, and travel speed during welding. Data logging also records gas flow, heat input, and cycle time. These records support traceability and help technicians investigate defects. Still, automation is not effortless. Poor fit-up can defeat expensive controls. A perfect program cannot repair a dirty or uneven joint.

Tips: Check pipe alignment with a calibrated gauge before welding. Clean the joint area carefully. Confirm shielding-gas flow at the torch, not only at the regulator. Run a short qualification test when material or thickness changes. Watch the first production bead closely. Small errors become expensive quickly. Skilled operators should review sensor alarms instead of accepting every automatic correction. Sometimes, the machine is technically correct, but the setup is not.

Top Auto Pipe Welding Machine Manufacturers Worldwide? – Key Technologies Used in Automated Pipe Welding

The chart compares representative welding-current ranges commonly used by automated pipe-welding processes. GTAW is typically selected for precise root passes, while GMAW, FCAW, and SAW support higher deposition rates for filling and capping passes. Actual settings vary according to pipe diameter, wall thickness, material, joint design, shielding gas, and applicable welding procedures.

Criteria for Comparing Global Machine Manufacturers

Comparing global auto pipe welding machine manufacturers requires more than reading speed claims. Start with the machine’s usable welding range, not its maximum brochure figure. Check pipe diameter, wall thickness, material compatibility, torch movement, and position accuracy. A machine designed for thin stainless pipe may struggle with thick carbon steel joints.

Ask each manufacturer for documented weld trials using your actual pipe samples. Measure bead width, penetration, arc stability, and heat distortion. Request procedure records, inspection reports, and repeatability data from several production cycles. Ask for evidence. A polished demonstration can hide setup difficulties.

Service capability matters just as much as engineering. Compare technician response times, operator training, spare-part availability, software updates, and remote diagnostic support across regions. Confirm electrical requirements and compliance documentation for every target market. Examine the control interface closely; clear alarms and stored parameters reduce production mistakes. Speak with current users about downtime, maintenance effort, and learning time. Their comments may reveal weaknesses that specifications omit. A spreadsheet can look precise and still mislead. Low purchase cost may become expensive when fixtures, consumables, calibration, and delayed repairs are added. Yet even this comparison is imperfect, because factory conditions rarely match a controlled test.

Leading Auto Pipe Welding Machine Manufacturers Worldwide

Choosing leading auto pipe welding machine manufacturers worldwide requires more than comparing purchase prices. Buyers should examine welding accuracy, orbital control, service coverage, and documented field experience. Pipe diameter ranges, wall thickness, joint design, and material compatibility also matter. A machine designed for stainless steel may perform differently on carbon steel or high-alloy applications.

Industry data supports this shift toward automation. The International Federation of Robotics reported 541,302 industrial robots installed worldwide in 2023. This reflects growing demand for repeatable production and reduced operator exposure. MarketsandMarkets estimates that the global welding equipment market will continue expanding through 2028, driven by infrastructure, energy, and manufacturing investment. However, reports often combine manual, robotic, and automated systems. Their figures should not be treated as exact pipe-welding demand.

Tips: Ask manufacturers for verified weld samples, cycle-time records, and maintenance response times. Check whether software supports traceability and real-time parameter monitoring. Request references from projects using similar pipe sizes and metals. A lower-cost machine can become expensive when spare parts arrive slowly.

A strong manufacturer should provide training, qualification support, and clear documentation. Factory demonstrations are useful, but they cannot replace long-term field evidence. I would also inspect calibration procedures and torch alignment personally. Marketing claims can sound precise, yet small setup errors may affect penetration and rework rates. The best choice is not always the most automated one; it is the system that fits the plant’s skills, workload, and quality controls.

Top Auto Pipe Welding Machine Manufacturers Worldwide? – Leading Auto Pipe Welding Machine Manufacturers Worldwide
Manufacturing Region Typical Automated Welding Processes Common Pipe Outside-Diameter Range Typical Wall-Thickness Capability Automation Configuration Applicable Qualification Standards Typical Industries Served Global Supply Profile
North America Mechanized GTAW, GMAW, FCAW and SAW systems; orbital GTAW for precision pipe work Approximately 25–1,500 mm, depending on the machine platform Approximately 1.5–75 mm, subject to joint design and welding process Track-mounted systems, positioners, column-and-boom equipment and multi-pass welding cells ASME Section IX, API 1104, AWS D1.1 and ISO 15614-1 are commonly specified Oil and gas, power generation, pressure vessels, process piping and heavy fabrication High export activity
Western Europe Orbital GTAW, mechanized GMAW, FCAW, SAW and hybrid welding solutions Approximately 6–1,200 mm for standard industrial equipment Approximately 1–60 mm, with specialized systems covering thicker sections Servo-controlled positioners, robotic cells, seam tracking and digitally monitored power sources EN 15614-1, ISO 3834, ISO 9606-1, PED-related requirements and applicable ASME codes Petrochemical, nuclear, pharmaceutical, food processing, shipbuilding and energy equipment High export activity
Central and Eastern Europe Mechanized GMAW, FCAW, SAW and orbital welding for industrial pipe assemblies Approximately 50–1,600 mm Approximately 3–100 mm for heavy-duty fabrication applications Rotary positioners, longitudinal seam systems, welding manipulators and automated flux recovery ISO 3834, EN 15614-1, ISO 9606-1 and project-specific pressure-equipment requirements District heating, steel fabrication, power plants, construction equipment and pipelines Established export activity
East Asia Orbital GTAW, GMAW, FCAW, SAW and robotic pipe welding systems Approximately 6–2,000 mm, depending on the automation class Approximately 1–120 mm across light, medium and heavy fabrication equipment Robotic cells, multi-axis manipulators, automatic wire feeding, seam tracking and production-line integration ISO 9001, ISO 3834, ISO 15614-1, ASME Section IX and API 1104 are frequently requested Shipbuilding, offshore structures, construction machinery, energy equipment and industrial piping Very high export activity
South Asia Mechanized GTAW, GMAW, FCAW and SAW systems for shop and field fabrication Approximately 25–1,500 mm Approximately 2–80 mm, depending on the number of welding heads and passes Portable orbital units, turning rolls, pipe positioners and semi-automatic welding stations ASME Section IX, API 1104, ISO 3834 and ISO 15614-1 are commonly used for project qualification Pipeline construction, boilers, pressure vessels, structural fabrication and process plants Growing export activity
Southeast Asia Orbital GTAW, GMAW, FCAW and robotic welding for repetitive pipe production Approximately 6–1,500 mm Approximately 1.5–75 mm Compact orbital equipment, rotary welding stations, robotic cells and integrated production fixtures ISO 9001, ISO 3834, ISO 15614-1, ASME Section IX and API 1104 Shipyards, palm-oil processing, petrochemicals, food processing and general manufacturing Strong regional supply
Middle East Mechanized GMAW, FCAW, SAW and orbital GTAW for pipeline and plant construction Approximately 50–1,800 mm Approximately 4–100 mm for pipeline and heavy industrial applications Field welding tractors, internal line-up systems, external welding stations and automated pipe handling API 1104, ASME Section IX, ISO 3834 and project-specific oil-and-gas specifications Transmission pipelines, refineries, LNG facilities, desalination and power generation Project-driven demand
Latin America Mechanized GMAW, FCAW, SAW and orbital GTAW for workshop and pipeline applications Approximately 25–1,500 mm Approximately 2–80 mm Portable welding tractors, pipe rotators, positioners and semi-automatic multi-pass systems API 1104, ASME Section IX, ISO 3834 and ISO 15614-1 Mining, oil and gas, hydropower, steel fabrication and industrial maintenance Regional and project-based supply
Capability ranges are representative industrial specifications rather than rankings of individual companies. Actual performance depends on pipe material, diameter, wall thickness, joint preparation, welding procedure, positioner capacity, heat input limits and required inspection level. Manufacturer qualification should be verified against the applicable project standard before purchase.

Industry Applications and Future Development Trends

Top Auto Pipe Welding Machine Manufacturers Worldwide?

Auto pipe welding machines now serve oil and gas lines, water infrastructure, shipyards, power plants, and prefabricated process skids. Their value depends on more than travel speed. Stable arc control, precise fit-up, repeatable heat input, and field service support matter equally. The International Federation of Robotics reported 541,302 new industrial robots installed worldwide in 2023. This growth signals wider automation across heavy manufacturing. Deloitte and The Manufacturing Institute also forecast up to 2.1 million unfilled manufacturing jobs by 2030. Pipe welding automation may reduce repetitive exposure, but it cannot replace skilled judgment during poor alignment or changing site conditions.

Future development will center on sensor-guided welding, digital twins, remote monitoring, and adaptive control. Cameras and laser scanners can detect joint gaps before defects become expensive. Data platforms may compare amperage, travel speed, shielding gas flow, and temperature in real time. Yet the data is often incomplete. A reflective pipe surface can still confuse a sensor. Human inspection remains necessary. Lower-energy power sources and improved wire efficiency may also support cleaner fabrication, especially in large-volume plants.

Tips:

Ask manufacturers for documented weld procedure qualification records, not only speed claims. Test the machine on your actual pipe diameter, wall thickness, alloy, and joint design. Check maintenance access, operator training, and spare-part response times. A short factory demonstration is useful, but a supervised field trial reveals more.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.
