How to Use RFID Tags for Asset Tracking
Tracking equipment across a warehouse can feel simple until a pallet disappears behind three storage rows. Rfid Tags For Asset Tracking create a digital trail for tools, inventory, vehicles, and returnable containers. Each tag stores an identifier, while fixed or handheld readers capture movement without direct line-of-sight scanning. This can reduce manual searches and improve inventory accuracy when the system is designed carefully.
A practical deployment begins with the asset, not the reader. Record its material, size, location, and expected movement. Metal surfaces and liquid-filled containers may weaken signals, so tag selection and placement require testing. A rugged tag on a steel cart may need a spacer or specialized mounting surface. Small details matter.
Readers need sensible coverage. Too many devices can create duplicate events, while weak coverage leaves silent gaps. Integrating RFID data with an asset management platform also helps teams view ownership, maintenance dates, and last-seen locations. The strongest results usually come from pilot testing, clear operating procedures, and regular audits.
RFID is not magic.
In practice, tags can detach, readers can miss signals, and databases can contain outdated records. I have found that a short pilot in one storage zone often reveals more than a large theoretical rollout. Teams should measure read accuracy, search time, installation effort, and staff acceptance before expanding. Independent standards, vendor documentation, and documented test results can support trustworthy decisions. The goal is not merely to scan more assets. It is to create reliable, explainable information that helps people manage physical resources with fewer delays and fewer avoidable errors.
What RFID Asset Tracking Is and How It Works
How to Use RFID Tags for Asset Tracking
What RFID Asset Tracking Is and How It Works
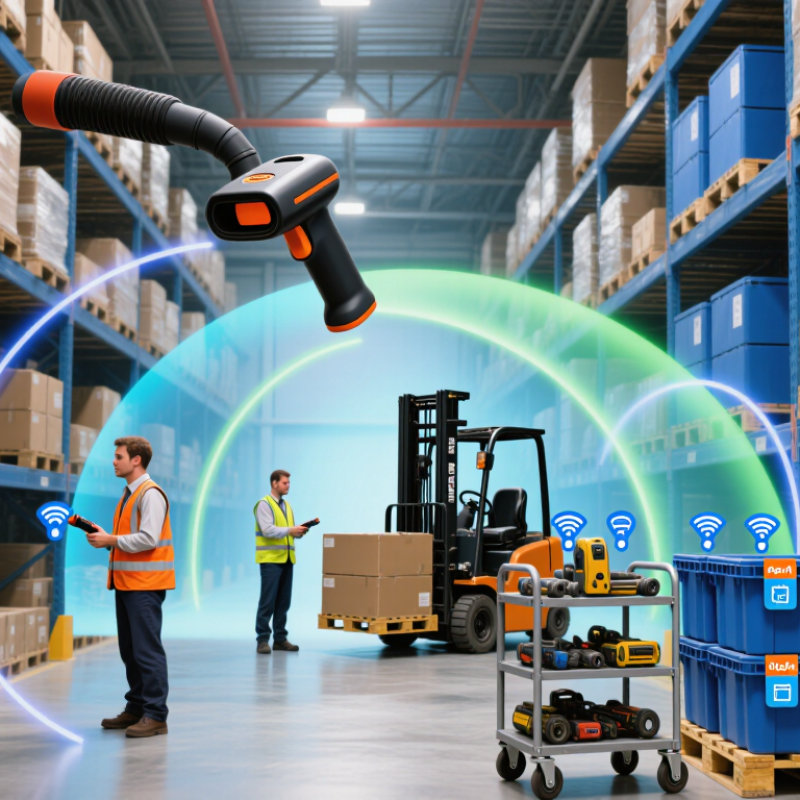
RFID asset tracking uses small electronic tags to identify and locate physical items. Each tag stores a unique identifier linked to an asset record. A reader sends radio signals to the tag. The tag then returns its identifier to the reader. Software records the event, time, and reading location.
Passive tags use energy from the reader’s signal. They are suitable for tools, containers, equipment, and boxed inventory. Active tags contain batteries and can transmit across longer distances. Their higher cost requires careful planning. A practical setup places readers at entrances, storage zones, or workstations. When an asset passes a reader, the system updates its movement history. Staff can then check whether equipment is available, misplaced, or due for inspection.
Placement matters greatly. Metal surfaces and liquids can weaken RFID performance. Testing several tag positions is essential. Do not trust a single successful scan. A warehouse trial may work well near a doorway but fail beside dense shelving. I have seen teams blame the software when the real problem was poor tag attachment. Records also need regular maintenance. If an asset changes location, its digital record must change too.
RFID is not magic.
Reliable tracking depends on readable tags, calibrated readers, accurate asset data, and trained users. Teams should test realistic conditions before expanding the system. They should also define who can edit records and how exceptions are handled. A missed scan is not always a technical failure; sometimes a worker carried the item outside the reading zone. That detail deserves investigation.
Choosing RFID Tags for Different Asset Types
How to Use RFID Tags for Asset Tracking
Choosing RFID tags starts with the asset, not the reader. Metal equipment can block or detune ordinary tags, so use tags designed with a spacer or protective backing. Liquid containers create another challenge because water absorbs radio signals. Test tags on filled containers, not empty ones. For cardboard boxes, clothing, and plastic tools, lightweight adhesive tags often provide reliable performance. Rugged assets may need screw-mounted or industrial tags that resist dust, moisture, impact, and temperature changes.
Tips: Match the tag to the surface, expected read distance, and handling conditions. Check whether cleaning chemicals or outdoor exposure could damage the label. Place the tag where workers can see and protect it. A hidden tag may survive longer, but it can become difficult to inspect. Record the tag location in your asset database.
Field testing matters. A tag that reads perfectly on a workbench may fail beside machinery or stacked inventory. Test several tag positions and approach angles. Use real workflows, including movement, storage, and repeated scanning. I have learned that maximum read range is not always useful. Overly sensitive tags may capture nearby assets and create confusing records. Smaller assets may need compact tags, while large equipment can support multiple tags for easier identification. Some choices remain imperfect, especially when one tag must serve many asset types. Review failed reads, adjust placement, and document the reasoning for future purchases.
Preparing Assets and Setting Up RFID Readers
Preparing assets and configuring RFID readers determines whether tracking data becomes useful or noisy. Clean each asset and remove old labels before applying a tag. Place tags on flat, visible surfaces when possible. Metal, liquid, and dense materials can weaken radio signals, so test each asset type separately. The 2024 RFID market report by MarketsandMarkets estimates the sector will grow from about $14.5 billion in 2024 to $24.9 billion by 2029. That growth reflects wider operational use, not automatic accuracy.
Our pilot team once placed tags too close to metal shelving. Read rates looked acceptable during testing, then fell sharply during busy movements. We repositioned the tags and reduced reader power near doorways. Set readers at receiving points, storage aisles, and dispatch exits. Define read zones with physical markers. Record antenna height, angle, power, and interference sources. The RFID Lab at Auburn University repeatedly emphasizes controlled testing and repeatable tag performance in its industry benchmarking work. Do not trust one successful scan.
Tips: Create a small test group before tagging everything. Include metal cases, liquid containers, fabric items, and stacked cartons. Walk assets through each reader several times. Compare missed reads, duplicate reads, and false reads. Keep a simple configuration log. A second technician should review it. That extra check may reveal assumptions everyone accepted too quickly. Overpowered readers can create more data, but not necessarily better data.
Capturing, Organizing, and Monitoring Asset Data
RFID asset tracking begins with reliable data capture, not expensive equipment. Attach a durable tag to each asset, then record its identification number, location, condition, and assigned user. Readers can capture several tags during a warehouse walk or equipment check. This reduces manual typing and exposes missing records quickly. Metal surfaces, liquid containers, and crowded storage areas may weaken signals, so test tag placement under real conditions.
Organize the captured data around practical fields. An asset record might show purchase date, maintenance history, current location, and expected return date. Use consistent names for rooms, departments, and equipment types. Otherwise, “Storage A” and “Store Room A” can become separate locations. That small mistake causes large reporting problems. Keep access permissions clear, and retain an audit trail for changes. Reliable records need accountability.
Monitoring becomes useful when the system supports routine decisions. Set alerts for overdue returns, unusual movement, inspection dates, or assets leaving approved areas. Review exception reports with staff who handle the equipment daily. Their experience often explains problems that a dashboard cannot. A reader may report a tag, while the asset remains misplaced. Human verification still matters. I have found that simple weekly checks reveal gaps faster than complex reports. No setup is perfect. Reassess reader coverage, tag durability, and data quality after several weeks of use.
Maintaining RFID Tracking Accuracy and System Performance
How to Use RFID Tags for Asset Tracking
Maintaining tracking accuracy starts with the physical environment, not the dashboard. Metal shelves, liquid containers, and tightly packed cartons can weaken or redirect radio signals. Place tags on a consistent, testable surface, then record each asset’s orientation. In field deployments, a portal that reads well at one speed may miss tags when forklifts move faster. Set a baseline using repeated passes, not one successful scan. The 2024 MHI Annual Industry Report states that 39% of surveyed supply-chain organisations currently use sensors and automatic identification. Adoption is growing, but performance still depends on disciplined installation and measurement.
Tips: Test each tag type on real materials. Mark reader zones on the floor. Keep antenna angles fixed. Log missed reads by location, speed, and asset class. Review the exception log weekly. A simple spreadsheet can reveal patterns before expensive changes. Avoid chasing a perfect 100% rate without context; a 99% read rate may still create serious inventory gaps at high volume. The RAIN Alliance’s 2024 market research indicates that tens of billions of RAIN RFID tags are sold annually, making quality control more important across large deployments. Yet tag volume does not guarantee reliable data. Antenna power, reader firmware, interference, and reader placement need periodic checks. Errors remain. That is useful evidence, not failure.





