What Is a Cold Storage Freezer Unit Used For?
A Cold Storage Freezer Unit keeps products at controlled subzero temperatures when ordinary refrigeration is not enough. It is used in food processing, distribution, laboratories, and other settings that need dependable frozen storage. The exact temperature depends on the product and its handling requirements. Frozen food, for example, must remain consistently cold to protect quality and reduce spoilage risk.
Inside, insulated panels limit heat transfer, while a refrigeration system removes heat from the storage space. Fans may circulate cold air, and digital controls help staff monitor conditions. You might see pallet racks holding cartons, temperature displays near the door, and alarms that flag a rising reading. These details matter. A freezer is only useful when its temperature is suitable and monitored.
Cold Storage Freezer Units can support bulk inventory, seasonal production, and the safe holding of temperature-sensitive materials. But they are not all interchangeable. Capacity, airflow, door use, product loading, and maintenance can affect performance. Frequent door openings may introduce warm, moist air. Poorly packed loads can also restrict circulation. Small operational habits make a difference.
Choosing a unit starts with understanding what will be stored, how much space it needs, and how often staff will access it. Temperature records and routine equipment checks help reveal problems early. Still, monitoring cannot replace good maintenance. Nor can a freezer correct poor product handling. This guide explains common uses, key components, and practical considerations, while recognizing that real operating needs vary from site to site.
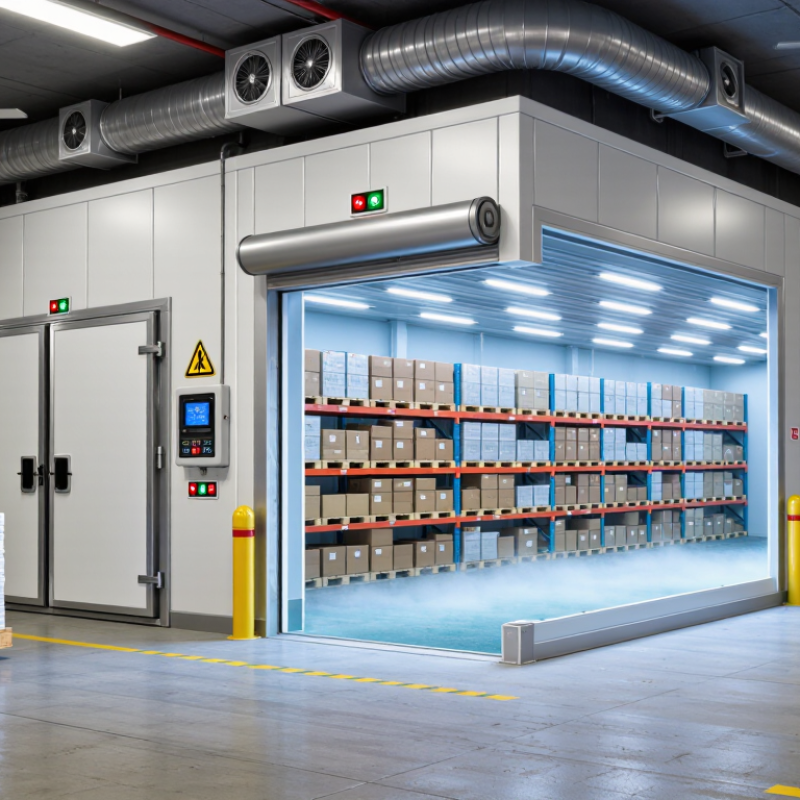
What Defines a Cold Storage Freezer Unit and Its Core -18°C Benchmark?
A cold storage freezer unit is an insulated enclosure with a refrigeration system designed to keep products frozen during storage. Its core benchmark is -18°C, or about 0°F. At this temperature, many frozen foods can maintain quality for extended periods, though packaging and storage time still matter. The number is a practical target, not a promise that every item stays unchanged. Texture can suffer, and poor wrapping may allow dry, pale freezer burn.
The unit’s job is to remove heat and limit temperature swings. Thick insulated walls, a tight door seal, and steady airflow help maintain conditions. A crowded shelf can block vents, while frequent door openings let warm, moist air enter. During routine checks, staff can compare a reliable thermometer reading with the unit display. Small mismatches happen. Investigate persistent changes rather than assuming the display tells the whole story.
Tips: Keep products off air vents, leave space for circulation, and record temperatures at consistent times. Check the door gasket for gaps; a strip of paper should resist being pulled from a closed door. If temperatures drift above -18°C, check the load, seal, and airflow, then follow the unit’s operating guidance.
What Is a Cold Storage Freezer Unit Used For? - What Defines a Cold Storage Freezer Unit and Its Core -18°C Benchmark?
| Dimension | Typical Details | Purpose or Practical Note |
| Basic definition | A refrigerated enclosure designed to store products below their freezing point, with temperature controlled for frozen storage. | It generally includes insulated walls and doors, a refrigeration system, temperature controls, and airflow management. |
| Core benchmark | −18°C (0°F) or colder | This is a widely used reference temperature for long-term storage of many commercially frozen foods. Actual requirements depend on the product and applicable regulations. |
| Common applications | Frozen food, meat, seafood, vegetables, ice cream, and certain temperature-sensitive materials. | Storage conditions should be selected according to product specifications; not every item is suitable for the same temperature or storage period. |
| Temperature stability | Designed to maintain a controlled set point, with monitoring to detect fluctuations. | Frequent door openings, overloading, blocked airflow, or equipment faults can cause temperature variation. |
| Air circulation | Fans or other airflow arrangements distribute cooled air through the storage space. | Leave suitable clearance around stored goods and air outlets to support even cooling and avoid obstructing circulation. |
| Product placement | Goods are typically stored on racks, shelves, or pallets and organized to allow access and airflow. | Keep products away from evaporator outlets and avoid placing warm goods into a unit intended for maintaining already-frozen stock unless it is rated for that duty. |
| Monitoring and records | Temperature displays, alarms, and manual or electronic temperature logs may be used. | Monitoring helps identify excursions. Sensor placement and record frequency should reflect the unit’s operating procedures and relevant requirements. |
| Defrost management | Many units use scheduled or demand-based defrosting to remove frost from cooling components. | Defrost cycles are part of normal operation, but excessive frost can reduce airflow and cooling performance. |
| Routine upkeep | Typical tasks include checking door seals, cleaning condenser surfaces, keeping drains clear, and servicing refrigeration components. | Regular maintenance supports reliable temperature control and helps reduce avoidable energy use and downtime. |
| Important distinction | A storage freezer is primarily intended to maintain frozen products; a blast freezer is designed to freeze products rapidly. | Use equipment rated for the required product load, pull-down time, capacity, and operating temperature. |
The −18°C benchmark is a common frozen-food storage reference, not a universal specification. Always follow product guidance and applicable food-safety or industry requirements.
How Do Freezer Units Preserve Food, Medicines, and Other Temperature-Sensitive Goods?
A cold storage freezer unit preserves temperature-sensitive goods by continuously removing heat from an insulated chamber. For frozen food, maintaining about -18°C slows microbial growth, oxidation, and moisture loss. This temperature does not make food permanently safe. Quality can still decline during long storage or repeated thawing. A properly loaded freezer leaves space between cartons, allowing cold air to circulate around every package. This detail is easy to overlook.
Medicines require tighter control. Some vaccines and biological products need frozen storage, while others must remain refrigerated, not frozen. Staff should follow the product’s approved temperature range rather than rely on general freezer settings. Calibrated probes, data loggers, and visible alarms help identify unsafe changes. A brief door opening may cause little harm, but a power failure can raise the internal temperature quickly. Temperature records provide evidence for careful decisions.
Freezers also protect laboratory samples, prepared ingredients, and selected chemical materials. Operators should label each item with its name, date, and required range. They should inspect door seals, remove ice buildup, and test alarms regularly. Even a well-managed unit can fail without warning. I have seen small gaps around a damaged seal create uneven temperatures. The display may look normal while products near the door warm first. That possibility deserves honest attention.
Which Systems Serve Different Needs: Walk-In, Blast, and Ultra-Low-Temperature Freezers?
What Is a Cold Storage Freezer Unit Used For?
Cold storage systems protect products by keeping them within a controlled temperature range. Walk-in freezers suit larger inventories, such as boxed food or prepared meals. Staff can enter to organize shelves, check labels, and move stock with carts. Walk-in units may be configured for chilled or frozen storage, so confirm the required range before choosing one. Door openings matter. Frequent traffic can raise temperatures and create frost.
Blast freezers serve a different purpose: they rapidly lower the temperature of warm or freshly prepared products. Strong, directed airflow helps freeze items more quickly than ordinary storage equipment. This can limit large ice crystals in many foods, supporting texture after thawing. Blast freezing is a process step, not long-term storage; products usually need transfer to a suitable freezer afterward. Ultra-low-temperature freezers, often operating near -80°C, are designed for certain research samples and sensitive materials. They need stable power, temperature alarms, and careful access controls.
Tips: Match the unit to the product, load size, and temperature target. Check temperatures with an independent logger, not just the display. Leave airflow gaps around stored items. A crowded freezer may cool unevenly—an easy detail to overlook. Keep a written response plan for alarms and power interruptions.
How Do Refrigeration, Insulation, and Temperature Monitoring Maintain Safe Storage?
What Is a Cold Storage Freezer Unit Used For?
A cold storage freezer unit keeps temperature-sensitive goods frozen during storage. It is used for food, laboratory samples, and other materials that require controlled low temperatures. Safe storage depends on more than a cold setting. Refrigeration removes heat, while insulation slows outside warmth from entering. Together, they help the unit maintain a stable environment, even when the door opens briefly.
Temperature monitoring helps staff spot problems before stored goods warm beyond their required range. A clear display, regular checks, and suitable alarms can reveal a failing sensor or a door left ajar. Small fluctuations may be normal, but repeated changes deserve attention. Records also help teams review patterns, rather than relying on memory. That detail can be easy to overlook.
Tips: Keep the door closed as much as possible, check seals for gaps, and avoid blocking interior airflow. Place a separate thermometer where stored items sit, then compare its reading with the unit display. Follow the storage requirements for the specific materials inside; one temperature target does not suit every item. Temperature logs are useful, though they cannot fix a poorly maintained freezer.
What Capacity, Temperature Range, and Energy Data Guide Unit Selection?
A cold storage freezer unit protects temperature-sensitive products during storage, handling, and distribution. Selection should begin with usable capacity, not the advertised cabinet volume. Measure cartons, racks, airflow gaps, and future stock growth. A unit filled too tightly may hold more products, but it can recover temperature slowly after door openings.
Temperature requirements depend on the stored material. Many frozen foods require about -18°C, while laboratory samples may need -40°C, -60°C, or below. Confirm the product specification before choosing the freezer. Also check temperature uniformity, alarm functions, probe accuracy, and recovery time. A displayed temperature is helpful, but it does not prove every shelf remains stable. Record temperatures during busy periods, not only overnight.
Tips: Compare energy use in kWh per day and per year. Review test conditions, ambient temperature, defrost cycles, and door-opening assumptions. A larger cabinet may consume more power, yet an undersized unit can work harder and fail to maintain temperature. Insulation quality, compressor performance, and room ventilation matter. Keep clearance around the unit and clean condenser areas according to the service instructions. In practice, energy labels are useful, but they are not perfect predictions for every facility. I would leave extra capacity for seasonal demand, although that choice deserves a cost review. Smaller units may suit frequent access; larger units may reduce loading pressure but increase standby consumption. Temperature logs and maintenance records provide stronger evidence than purchase specifications alone.
Cold Storage Freezer Selection: Capacity, Temperature & Energy
Typical planning ranges for common freezer formats. Capacity and energy use vary with insulation, ambient temperature, door openings, loading, and equipment efficiency.
Temperature guide: Frozen-food storage is commonly maintained at −18°C or colder; some applications require lower setpoints. Confirm product requirements and the unit’s specified operating range. Use measured site conditions and manufacturer data—not capacity alone—to estimate energy costs.





