Why Choose Marble Slab for Global Projects?

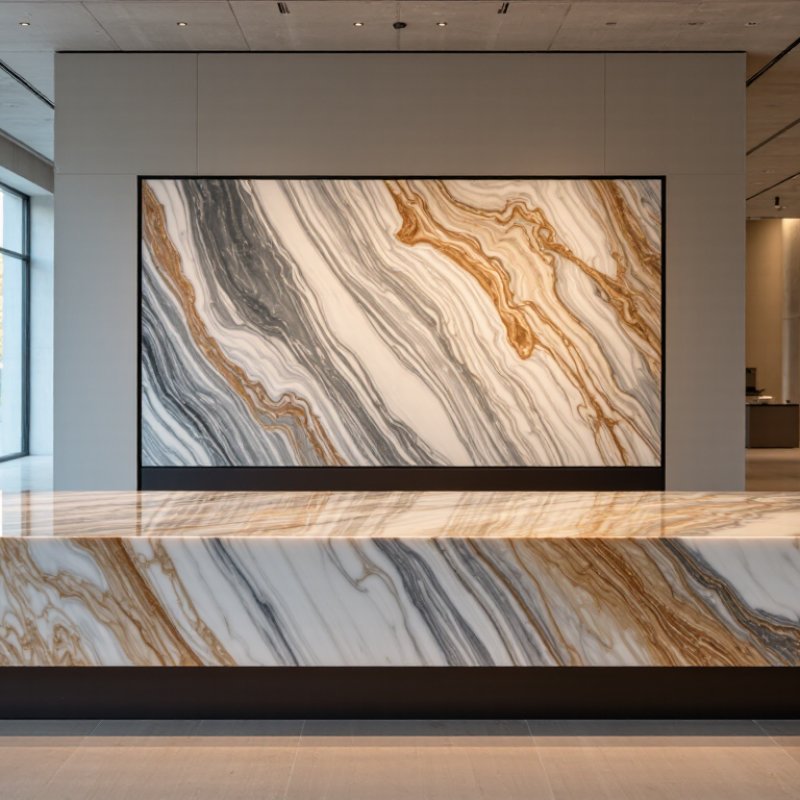
Choosing Marble Slab for global projects involves more than selecting an attractive surface. It requires a dependable balance of design, performance, sourcing, and logistics. Marble offers distinctive veining, natural depth, and a refined appearance that manufactured materials often struggle to reproduce. Each slab carries its own geological story. That individuality creates visual character.

Experienced project teams assess more than color. They review slab dimensions, thickness, water absorption, surface condition, and expected maintenance. They also inspect samples under realistic lighting. A showroom sample can look different beside large windows or warm interior lighting. Careful planning matters.

For international developments, supply reliability becomes equally important. Professional suppliers should provide clear quarry information, inspection records, packing standards, and accurate shipping schedules. They should also explain how the material will be fabricated and installed locally. Standards vary between markets, so project documentation must be checked with qualified architects, engineers, and contractors.

Marble is not maintenance-free. That deserves honest attention. Acidic cleaners, standing water, and careless handling can affect its surface. Natural variation may also create differences between approved samples and delivered slabs. These are not reasons to reject the material, but they require realistic specifications and client approval.

When selected responsibly, Marble Slab can support hotels, residences, commercial interiors, and landmark spaces across different regions. Its value comes from more than luxury. It comes from verified quality, practical coordination, and long-term design confidence. The strongest results appear when beauty and evidence guide the same decision.
Why Choose Marble Slab for Global Projects?

Define Project Requirements: 20–30 mm Slabs, Finish, Format, and Tolerance

Why Choose Marble Slab for Global Projects?

Define Project Requirements: 20–30 mm Slabs, Finish, Format, and Tolerance

Global marble projects require a written slab schedule before purchasing begins. Specify 20, 25, or 30 mm thickness, not simply “standard thickness.” Include finished dimensions, allowable variation, edge details, and reinforcement requirements. EN 1469 and ASTM C503/C503M provide useful references for stone performance and dimensional control.

Finish changes both appearance and safety. Polished marble reflects strong light, while honed surfaces show softer movement and usually offer better visual consistency. Flamed or textured finishes may improve slip resistance, but they can expose more color variation. The 2024 World Natural Stone Trade Report recorded over 50 million tonnes of internationally traded natural stone in 2023. That scale makes clear specifications essential.

Format decisions should match the installation method. Large panels reduce joints but increase handling risks. Smaller formats simplify replacement and access around corners. A tolerance of ±1 mm may suit precision interiors, while larger architectural elements may require a different allowance. Confirm this through approved shop drawings and a full-size mock-up.

Do not trust photographs alone.

Review quarry test reports, finish samples, and calibration records. ASTM testing can verify water absorption, density, and strength, but laboratory results do not predict every site condition. That assumption is convenient, but often wrong. Veining, shade, and thickness can still vary between production lots. Record each lot clearly before fabrication.

Why Choose Marble Slab for Global Projects?

Define project requirements clearly by confirming slab thickness, surface finish, format, and dimensional tolerance before procurement.

Thickness

20 mm for lighter applications; 30 mm for higher visual weight and durability.

Finish

Polished, honed, and leathered finishes should be approved against a physical sample.

Format

Confirm standard or jumbo slabs according to layout, access, lifting, and installation limits.

Tolerance

Allow approximately ±1–2 mm for thickness and verify project-specific fabrication standards.

Planning reference: common natural-stone slab thickness options and indicative dimensional allowances. Final tolerances should be confirmed in the project specification and inspection plan.

Verify Performance: ASTM C170 Strength and EN 13755 Absorption Data

Why Choose Marble Slab for Global Projects?

Verify Performance: ASTM C170 Strength and EN 13755 Absorption Data

Marble slabs can bring depth, light, and a durable surface to international projects. Yet appearance should never replace measured performance. ASTM C170 evaluates compressive strength, helping engineers assess how marble may respond under structural pressure. EN 13755 measures water absorption at atmospheric pressure. Lower absorption can support better resistance to staining and moisture-related damage, especially in humid interiors and exposed applications.

Tips: Request current laboratory reports, sample identification, test conditions, and production-lot traceability. Compare results with the project specification, not with attractive photographs. Check slab thickness, fixing design, edge details, and local climate together. A strong stone can still fail when installation allows water behind the panel.

Performance data needs careful interpretation. ASTM C170 results do not automatically predict freeze-thaw behavior, abrasion resistance, or anchor capacity. EN 13755 absorption data also cannot guarantee stain-proof performance. Field teams should review quarry variation and test representative samples before approval. Small differences in veining may indicate different mineral structures. That detail is easy to overlook.

A practical review should include mock-ups, sealed joints, and cleaning trials. Dusty transport routes can expose surface weaknesses early. A laboratory result is valuable, but it is not the whole building. Project decisions should remain evidence-based, transparent, and open to revision when site conditions disagree with expectations.

Assess Lifecycle Value: 50-Year Design-Life Benchmarks for Marble

Why Choose Marble Slab for Global Projects?

A 50-year design-life benchmark makes marble easier to evaluate across global projects. It is a planning reference, not a guaranteed lifespan. ISO 15686-1 explains that service life depends on climate, detailing, maintenance, and actual use. RICS Whole Life Carbon Assessment, 2nd edition (2023), commonly applies a 60-year study period for commercial buildings. That difference matters. A 50-year marble assessment should test performance before replacement assumptions are accepted.

In practice, marble can retain value when its slab thickness, fixing system, drainage, and surface finish match the site. Coastal air, freeze-thaw cycles, foot traffic, and cleaning chemicals can change the result. The Natural Stone Institute recommends evaluating absorption, flexural strength, abrasion, and stain resistance before selection. A project team should also request verified environmental product data. UNEP’s 2023 Global Status Report notes that buildings create about 37% of global energy and process-related emissions. Long service life can reduce replacement impacts, but transport and quarrying still require scrutiny. The uncomfortable truth is simple: beautiful stone does not correct weak detailing.

Tips: Compare a 50-year and 60-year scenario. Record cleaning frequency, repair access, and expected replacement rates. Check local weather data. Test a sample panel. Leave room for doubt. A polished finish may age unevenly in busy entrances, especially where grit collects near doorways. Lifecycle value becomes credible only when design assumptions meet observed maintenance records.

Control Global Supply: ASTM C503 Compliance, Batch Traceability, and QC

Why Choose Marble Slab for Global Projects?

Global marble supply requires more than attractive photographs and a competitive quotation. ASTM C503 compliance gives project teams a consistent reference for material performance, testing, and acceptance. Each slab should be linked to its quarry block, production date, finish, and inspection record. This information matters when matching stone across several buildings or shipment phases.

Batch traceability begins before cutting. Suppliers can assign a unique batch code and record block origin, slab thickness, dimensions, and surface treatment. Independent testing may verify water absorption, density, flexural strength, and compressive strength. Inspection teams should also check veining, cracks, edge damage, flatness, and color variation under suitable lighting. Small details become expensive problems later.

Quality control needs evidence, not confident promises. A clear inspection report, packing list, and photographic record help resolve questions across time zones. Crates should show durable labels, handling directions, and matching batch numbers. No inspection system is flawless. A missed label or inconsistent finish can disrupt installation. That risk is why pre-shipment checks and random sampling remain valuable. Teams should review nonconforming slabs honestly, even when replacement affects the schedule. Careful records build trust between quarries, fabricators, distributors, and project managers.

Why Choose Marble Slab for Global Projects? – Control Global Supply: ASTM C503 Compliance, Batch Traceability, and QC
Control Dimension Data to Record or Verify Acceptance or Control Basis Quality Evidence Release Status
Material Identification Marble type, commercial description, country of origin, quarry source, block number, and slab reference. Material identity must match the approved sample, shop drawings, purchase specification, and project schedule. Approved material submittal, sample approval record, quarry or production identification record. Documented
ASTM C503 Compliance Compliance declaration for marble dimension stone supplied for the project, including the applicable ASTM C503/C503M edition. Conformance is evaluated against ASTM C503/C503M and the project specification. The applicable marble classification and project-specific limits must be stated. Material compliance statement, current product data, and third-party or laboratory test reports where required. Verified
Physical Properties Water absorption, density, compressive strength, and flexural strength or modulus of rupture, as applicable to the specified marble. Recorded test results must meet the limits established by the applicable standard, marble classification, and project specification. Laboratory report identifying the specimen, test method, test date, and result units. Test Required
Test Method Control Test method, specimen orientation, specimen quantity, conditioning procedure, laboratory identity, and test date. Testing must follow the methods referenced by the governing specification and the applicable ASTM requirements. Complete laboratory test report with method references and signed or electronically approved results. Traceable
Batch Traceability Unique batch ID linked to quarry block, slab numbers, production date, finishing line, finish type, thickness, and destination. Every slab must be traceable from the shipping document back to its originating block and production records. Batch register, slab tags, barcode or QR record, packing list, and shipping documentation. Mandatory
Dimensions and Tolerances Slab length, width, thickness, squareness, edge condition, flatness, and any project-defined dimensional tolerance. Dimensions and tolerances must comply with approved fabrication drawings, purchase requirements, and applicable project standards. Incoming and final inspection report with calibrated measurement equipment records. Measured
Surface Finish Specified finish, such as polished, honed, brushed, or sanded; finish uniformity; visible resin or filler treatment; surface defects. Finish, color range, veining, pits, repairs, and allowable visual characteristics must match the approved control sample. Visual inspection checklist, approved sample, photographic record, and nonconformance report where applicable. Inspected
Color and Veining Control Slab sequence, tonal variation, vein direction, book-match or vein-match requirements, and installation zone allocation. Slabs must be selected and packed according to the approved layout and the project's permitted natural variation. Slab layout drawings, high-resolution photographs, selection record, and installer allocation list. Approved
Defect Classification Cracks, open fissures, chips, stains, warpage, edge damage, excessive repairs, and other visible discontinuities. Defects must remain within the project-approved visual and structural limits. Rejected material must be segregated and identified. Inspection checklist, defect map, quarantine tag, corrective-action record, and disposition approval. Controlled
Packaging and Protection Slab separators, edge protection, moisture protection, crate identification, lifting points, and maximum safe loading configuration. Packaging must prevent impact, staining, abrasion, movement, and moisture-related damage during handling and international transport. Packing inspection record, crate list, loading photographs, handling instructions, and shipping marks. Released
Document Control Revision number, purchase order, inspection plan, test reports, certificates, packing list, and destination documentation. Only current, approved documents may be used for production, inspection, packing, and shipment release. Controlled document register and project quality dossier with revision history. Current
Nonconformance Management Nonconformance number, affected batch or slab IDs, defect description, root cause, corrective action, and final disposition. Nonconforming material must be identified, isolated where necessary, reviewed, and formally accepted, repaired, replaced, or rejected. Nonconformance report, corrective-action record, reinspection result, and authorized disposition. Closed Before Shipment
Shipment Release Final quantity, slab IDs, approved inspection status, container or vehicle number, seal number, destination, and shipping date. Shipment is released only after required inspections, document checks, packaging verification, and outstanding nonconformances are resolved. Final release checklist, packing list, inspection approval, and transport record. Release Gate
Receiving Verification Received quantity, slab IDs, packaging condition, visible damage, dimensions, finish, and comparison with shipping documents. Receiving inspection must confirm that delivered slabs match the approved batch records and purchase requirements before fabrication or installation. Receiving inspection report, delivery photographs, signed delivery record, and discrepancy report. Site Verified

Plan Installation: 2–3 mm Joints, Substrate Tolerances, and Moisture Control

Why Choose Marble Slab for Global Projects?

Marble slab brings depth, natural movement, and a strong architectural presence to global projects. Its installation, however, demands careful planning. A 2–3 mm joint can create a refined surface, but it allows little room for error. Every slab edge should be checked for squareness, thickness variation, and possible chipping before placement. A dry layout on site often reveals problems that drawings miss.

The substrate must be stable, clean, and within the project’s specified tolerance. Do not assume a visually flat floor is truly flat. Use a straightedge or laser level across several directions, then record high and low points. Excessive unevenness can force slabs into tension, causing cracks or uneven joints. Large-format marble also needs proper support beneath the full slab, not only at selected spots. I have seen rushed preparation create avoidable lippage.

Moisture control deserves equal attention. Test the substrate using the project-approved method, and follow the adhesive manufacturer’s moisture limits. High moisture can stain porous marble, weaken adhesion, or delay curing. Waterproofing and vapor-control details should match the building’s climate and wall or floor assembly. A small mock-up can confirm joint width, adhesive coverage, grout color, and cleaning methods. It may feel slower, but it exposes weak assumptions early. Even experienced teams should leave room for adjustment; natural stone rarely behaves as perfectly as the schedule suggests.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.