Why Choose Titanium Hemispheric Bolt for Global Sourcing?

Why Choose Titanium Hemispheric Bolt for Global Sourcing?

Global sourcing decisions often begin with one practical question: will the fastener remain reliable after years of exposure, vibration, and maintenance? A Titanium Hemispheric Bolt offers a strong answer for demanding assemblies. Its rounded head can reduce snagging points, while titanium’s low density helps control overall equipment weight. It also provides strong corrosion resistance in humid, marine, and chemically challenging environments.

Matthew J. Donachie Jr., author of Titanium: A Technical Guide, wrote, “Titanium alloys are used where their unique properties justify their higher cost.” This principle remains valuable for sourcing teams. The lowest unit price is not always the lowest total cost. A bolt that resists corrosion may reduce replacement work, shutdowns, and inspection pressure. That matters in aircraft structures, medical equipment, offshore systems, and precision machinery.

Details matter.

Buyers should verify grade, diameter, thread accuracy, surface finish, head dimensions, and batch traceability. Supplier audits and material certificates also deserve attention. However, titanium is not automatically the best choice. Its higher material price, possible galling during installation, and specialized machining requirements can create avoidable problems. In my view, this is where many sourcing comparisons become too optimistic.

A realistic evaluation should compare purchase cost, service conditions, installation practice, and expected maintenance. It should also confirm compliance with the destination market’s technical requirements. With disciplined supplier selection, the Titanium Hemispheric Bolt can deliver dependable performance rather than merely an impressive specification.
Why Choose Titanium Hemispheric Bolt for Global Sourcing?

What Is a Titanium Hemispheric Bolt? Grade 5 Density: 4.43 g/cm³

Why Choose Titanium Hemispheric Bolt for Global Sourcing?

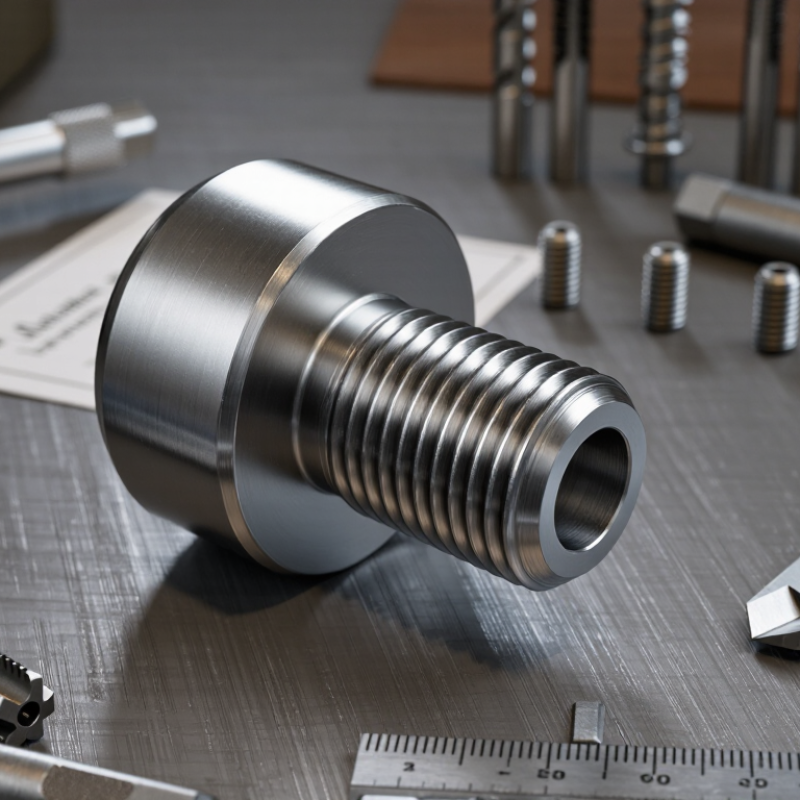
A titanium hemispheric bolt has a rounded, dome-shaped head and a threaded shaft. The curved head reduces sharp contact points and can distribute pressure across mating surfaces. This design is useful where exposed fasteners need smoother profiles and lower snagging risks. Grade 5 titanium, usually Ti-6Al-4V, has a density of approximately 4.43 g/cm³. That is far lighter than many steel alternatives. It also provides strong corrosion resistance and a useful strength-to-weight ratio.

In practical sourcing, this lower density can reduce assembly weight and handling effort. The material performs well in demanding outdoor, marine, and engineering environments. However, lightweight does not mean universally stronger. Thread design, preload, surface condition, and joint geometry still control performance. This detail is easy to overlook. A bolt may meet a material specification yet fail an application requirement. Reliable suppliers should provide dimensional inspection records, material certificates, batch traceability, and clear information about thread standards. Checking actual density is uncommon, but reviewing the stated alloy and certification remains valuable.

Tips: Confirm head diameter, thread pitch, length, and tolerance before ordering. Request samples for fit testing. Compare strength data at the expected temperature. Do not select Grade 5 only because it weighs less. A small design review can prevent expensive rework.

Why Titanium? About 43% Lower Density Than Steel (4.43 vs 7.85 g/cm³)

Why Choose Titanium Hemispheric Bolt for Global Sourcing?

Titanium hemispheric bolts offer a clear weight advantage in demanding assemblies. Titanium has a density of about 4.43 g/cm³, compared with steel at 7.85 g/cm³. That is roughly 43% lower. A box of bolts feels noticeably lighter during handling and shipping. This difference can reduce structural weight in aerospace, marine, medical, and high-performance equipment applications. Less mass may also simplify installation where access is limited.

However, weight is not everything. In practical sourcing work, I have found that thread accuracy, material grade, surface condition, and heat treatment matter just as much. A titanium bolt may resist corrosion well, but poor galling control can damage threads during tightening. Hemispheric heads also require careful contact design. The mating surface must distribute pressure evenly. One overlooked detail can create expensive rework.

Tips: Request density, tensile strength, hardness, and chemical composition reports. Confirm the exact diameter, thread standard, pitch, head radius, and tolerance. Test sample bolts with the intended torque tools before approving mass production. Compare shipping weight using real order quantities, not only individual part data. Titanium costs more, and the weight saving may not justify it in every application. That is worth checking honestly.

Performance Data: Grade 5 Tensile Strength Reaches 895 MPa

Why Choose Titanium Hemispheric Bolt for Global Sourcing?

Grade 5 titanium offers a strong performance case for demanding bolt applications. ASTM B348 specifies a minimum tensile strength of 895 MPa for this alloy. Its minimum yield strength is 828 MPa, with approximately 10% elongation. These figures support reliable clamping under high mechanical loads. They also provide useful design margin.

The hemispheric head spreads contact pressure across a rounded surface. This can reduce sharp stress concentration around the joint, especially on curved or uneven assemblies. In practical sourcing work, engineers should verify head radius, thread accuracy, surface finish, and dimensional tolerance. A bolt can meet the alloy requirement and still perform poorly if its geometry is inconsistent.

Corrosion resistance is another reason to consider titanium. ASM Handbook, Volume 17, identifies Grade 5 as a high-strength titanium alloy with strong resistance in many aggressive environments. However, the 895 MPa value is not a universal guarantee. Temperature, thread engagement, preload, machining damage, and galvanic contact can change actual performance. This is often overlooked.

For global purchasing, request material certificates, tensile-test records, heat-treatment details, and inspection results. ASTM-based testing improves traceability between suppliers. Independent verification is still sensible for critical assemblies. Country-specific documentation rules may also vary. A lower quoted price can hide weaker inspection control. That deserves careful review.
Global Standards: ASTM F468, ASME B1.1, and Material Traceability

Why Choose Titanium Hemispheric Bolt for Global Sourcing?

Global sourcing requires more than a competitive quotation. ASTM F468 helps define requirements for suitable nonferrous fasteners, including titanium grades, dimensions, and mechanical properties. The exact grade must match the engineering specification.

ASME B1.1 controls Unified inch screw thread forms, tolerances, and inspection practices. This matters when a hemispheric bolt crosses suppliers or assembly sites. Correct thread fit reduces rework, galling risks, and installation delays. Head shape still requires drawing control. The standard does not define every hemispheric feature.

Material traceability connects each bolt to its production history. A reliable record should show the heat number, material grade, test results, and certificate details. Incoming inspection can compare markings with documents and purchase requirements. Portable material identification may provide another useful check. Certificates are important, but they are not proof by themselves. Traceability can fail when records are copied carelessly.

In practical sourcing, clear specifications prevent many disputes. State the titanium grade, thread class, surface condition, dimensions, packaging, and inspection level. Keep samples from approved lots when possible. Mistakes happen. Even experienced teams should review tolerances and documentation before shipment. A supplier may meet ASTM F468 yet miss a project-specific requirement. That gap deserves attention before production begins.

Sourcing Workflow: RFQ, MOQ, Inspection, Lead Time, and Total Cost

Choosing a titanium hemispheric bolt for global sourcing requires more than comparing unit prices. The RFQ should state the titanium grade, thread standard, head diameter, radius, tolerances, surface finish, and packaging requirements. Attach a clear drawing and expected annual volume. Details matter. Ambiguous drawings often create costly revisions.

MOQ should be discussed with tooling, setup, and production capacity in mind. A lower MOQ may increase machining costs, while a higher MOQ can create unused inventory. Ask for separate pricing at several quantity levels. Request material certificates, dimensional reports, thread-gauge results, and sample approval before mass production. An independent inspection can verify head geometry, thread engagement, surface damage, and lot traceability. Do not rely only on photographs.

Lead time should be divided into engineering review, raw-material preparation, machining, inspection, and shipping. Titanium machining may need slower cutting speeds and careful control, so optimistic schedules can fail. That happens. Include a buffer for nonconforming samples or customs delays. Total cost should cover tooling, testing, packaging, freight, duties, payment fees, and possible rework. A cheaper quotation may become expensive after these items appear. In practice, I would compare landed cost beside technical risk, not unit price alone. One detail is still easy to miss: confirm whether replacement parts follow the same inspection plan.

Powder Coat Booths

For those larger-sized parts, or smaller quantity runs, we have 2 independent powder coat booths and ovens. The quality, durability and affordability of today’s powder coating finishes make this the process of choice for world-class companies.

Powder coating advantages over other forms of coating are many. Materials used in the Powder coating process can be metals and non-metals that come in a multitude of thicknesses, textures, colors, etc. Another of Powder coating’s biggest advantages over conventional coatings is its ability to create finishes in many different textures. Powder Coating Booths allow us the ability to apply these advantages to large products.

Wet Paint Line

Tri-State Fabricators runs a full-service conveyor line for painting. Wet painting can provide protection or decoration to many different part styles. From start to finish, every project is easier to undergo random and point-based inspection by our skilled painting team.

Advantages to our Wet Paint Line are these lines start with product prep and ends with a thorough inspection of a high quality finished product. Our ability to complete large and small projects with a superior finish and doing so in a timely and economical fashion. This passes along the savings in production to our customers. When powder coating ins not an option, our Wet Paint Line gets the job done right the first time.

Wet Paint Booths

When the parts get big and heavy we roll-out our custom paint racks and oversize booth. By utilizing our partnerships with all the major paint brands, we can match virtually any color with wet paint.

The advantages of having access to a Wet Paint Booth are many. Large projects of many different shapes can be loaded into the booth. The Wet Paint Booth offers an environment that is much more controlled than a typical parts painting operation.

Not only are they used because of their controlled environment, but they’re are also advantageous when it comes to applying paint to parts that are needed in industries that require specialty coatings such as medical, aerospace, etc.

Military CARC

Our military forces have some very high standards when it comes to the finish of their vehicles and equipment. From the first pre-treatment step to final coat, it takes a great deal of knowledge and experience to protect the men and women of our armed forces. They deserve only the best, and Tri-State Fabricators provides it.

All of our processes are closely monitored by our staff and management teams. Both of which are highly trained in the processes of metal fabrication and finishing. Tri-State Fabricators’ goal is to always fully satisfy each and every customer, including the military. We will always put a 110% into what we do.

Glass-Bead Blasting

Abrasive media blasting is an excellent way to remove old paint, rust, and increase the paint/powder adhesion. Glass beads produce a much smoother and brighter finish than angular abrasives; leaving the part clean yet without any dimensional change. Chemically inert and environmentally friendly, we can recycle our beads approximately 30 times; making them a more preferred method of metal cleaning or surface finishing.

Advantages to Glass Bead Blasting are many. Glass bead blast media is used when a project is needing rough surfaces need to become smooth for applications of coatings such as paint. It is typically used to clean paint and rust from a product surface without deforming the surface it is being used on. Overall, compared to many other blasting media, Glass Bead Blasting is a very economical choice and those savings are always passed on to our customers.

Part Washing

Tri-State Fabricators utilize a zinc phosphate wash to clean and etch the material to ensure the best paint adhesion possible. The unique design of our 3-stage wash system does the work like a 5-stage. From Cleaning and rinsing to conversion coating and post-treatment, Our Part Washing process is a complete service and works throughout the fabrication service and the finishing service.

Along with the previously mentioned benefits, Curing is a vital chemical reaction that leaves the product finish hard and relatively safe from mild abrasion and aggressive corrosion. This process can be done in more than one way; ambient air-dry or in curing ovens at temps that exceed 240°.

Burn-Off Oven

From fixing paint mistakes (someone else’s of course) to simply cleaning our paint line hooks, our burn-off oven is put to good use. After a quick burn-off, a little clean up, and a fresh coat of paint, your parts will look better than new.

Why does our Burn-Off Oven work so well? Because super heating the air around parts turns the materials into ashes. From paint and powder coatings to rubber and machining oils, high temps do the job without degrading the integrity of the part.

Masking

Masking is a vital part of producing high quality products. We have die-cut masking patterns to protect machined surfaces as well as a wide range of plugs and caps to protect threaded holes and bolts. We provide permanent and temporary masking.

Masking allows the selected sections of a product to be protected from a fabrication or finishing service. This can be with both chemicals when etching and tapes, paints when only finishing just a section of the product. Masking is great in aiding the customization process of a project.

Screen Printing

Screen printing is a photographic process that transfers artwork onto a porous nylon screen which allows colored ink to flow through the screen and be deposited on an aluminum or plastic component. We can generally have just about any design created onto a screen for your parts.

Some of the advantages of Screen Printing are, brand recognition for your business displaying on your products, assembly instructions, product warnings/hazards, etc. Tri-State Fabricators produces Screen Printing of the highest quality so you know it’s durable.

Metal Finishing

Metal Finishing is the art of treating the exterior portion of product, often metal but can also be made of other materials, so that the surface is clean and free of any debris. Then the process of applying coats or either paint of powder coat takes place. This coating process improves the quality of the product in both appearance and resistance to wear and corrosion.

Tri-State Fabricators, Inc., understands that a project typically isn’t complete until a high-quality finish has been added to your product. This is why our painting and powder coating teams continuously inspect the products throughout the Metal Finishing process.